In extreme corrosive environments such as sea-crossing bridges, offshore wind power, and port machinery, ordinary organic coatings often fail to meet the durability requirements of several decades. Thermal spray zinc with zinc wire, as a mature "metallization" protective technology, instantly melts pure zinc wire and sprays it onto the substrate surface, forming a zinc layer that is "metallurgically bonded" with steel, putting a veritable metal armor on major projects. Its protective life can reach decades, making it one of the heavy anti-corrosion solutions with the optimal life-cycle cost.
I. Principle of Thermal Spray Zinc
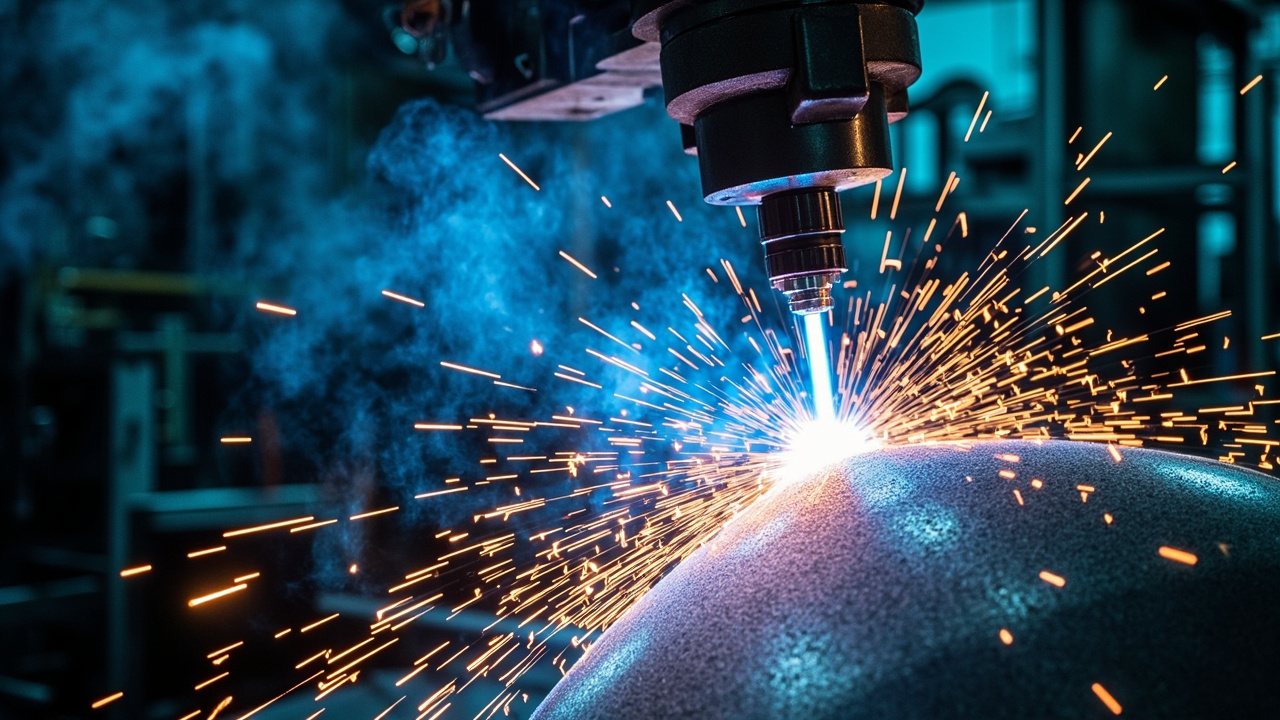
Thermal spraying uses an electric arc or flame to continuously melt the zinc wire, and uses compressed air to spray the molten droplets at high speed onto the sandblasted steel surface. After the molten droplets hit the substrate, they flatten and cool rapidly, stacking layer by layer to form a porous but dense zinc coating. Since zinc and steel produce local metallurgical bonding at the moment of impact, the bonding strength between the coating and substrate is much higher than the adhesion of ordinary paint, and the common problem of whole-sheet peeling of organic coatings will not occur.
The zinc wire itself is a long-lasting anti-corrosion "sacrificial anode material", and its purity and stability directly determine the service life of the coating.
II. Quality of Zinc Wire Determines Protective Life
The purity and dimensional stability of the zinc wire directly affect the spraying quality:
- Purity: It is recommended to use high-purity zinc wire above 99.99%; excessive impurities (especially iron and lead) will weaken the electrochemical activity and bonding strength.
- Wire diameter and ovality: Common specification Φ2.0–3.0 mm; uniform wire diameter without ovality ensures stable wire feeding, stable arc, and uniform atomization.
- Surface cleanliness: The zinc wire surface should be free of oil and scale to avoid contaminating the coating and causing slag inclusions.
- Winding quality: Neatly arranged without dead knots, ensuring continuous spraying without wire breakage and improving construction efficiency.
III. Anti-Corrosion Mechanism: Dual Protection
The zinc wire sprayed coating provides two layers of protection logic:
- Sacrificial anode protection: At damaged or porous areas, zinc corrodes preferentially, protecting the underlying steel from rusting through electrochemical action; even if the coating has local scratches, it can provide "self-healing" protection.
- Physical barrier: The continuous metallic zinc layer blocks the contact of water, oxygen, and chloride ions with the steel substrate; the pores are further densified after sealing treatment.
It is precisely this dual mechanism that enables the properly constructed zinc sprayed coating to achieve a protective life of 30–50 years or more on sea-crossing bridges, significantly reducing the huge costs of high-altitude and waterborne rework.
IV. Reference for Key Process Parameters
| Item | Typical Indicator | Description |
|---|---|---|
| Zinc wire purity | ≥ 99.99% | High-purity zinc |
| Coating thickness | 120–200 μm | Depending on corrosion grade |
| Bonding strength | ≥ 7 MPa | Metallurgical + mechanical bonding |
| Surface treatment | Sa 3.0 grade | Sandblast to near-white grade |
| Sealing paint | Epoxy sealing | Penetrate pores to prevent white rust |
| Service life | 30–50 years | With matching system |
V. Compatibility with Organic Coatings
A single zinc sprayed coating needs to be matched with sealing and topcoat to achieve maximum benefit:
- Sealing paint: Use low-viscosity epoxy sealing to penetrate the pores of the zinc layer, prevent white rust, and improve density.
- Intermediate and top layers: Match with the epoxy micaceous iron intermediate coat and water-based fluorocarbon topcoat in the heavy-duty anti-corrosion system to provide weather resistance and decoration.
- Wind power scenario: In wind tower protection, zinc spraying + sealing + topcoat is a classic combination for marine environments.
VI. Typical Application Scenarios
- Sea-crossing bridges and steel box girders: Standard anti-corrosion process for mainstream sea-crossing projects worldwide, balancing ultra-long life and low maintenance.
- Offshore wind tower and foundation: The first choice for high salt spray and long-life requirements, reducing high-cost offshore operation and maintenance.
- Port machinery and offshore platforms: Withstanding harsh corrosion from dry-wet alternation and splash zones, the metallic zinc layer performs stably.
VII. Frequently Asked Questions (FAQ)
Q: What is the difference between thermal spray zinc with zinc wire and hot-dip galvanizing? Hot-dip galvanizing immerses the workpiece entirely into molten zinc, limited by the size of the galvanizing bath; thermal spray zinc is sprayed on-site on the workpiece surface, not limited by size, suitable for large steel structures and on-site construction, and allows local thickness control.
Q: Why must sealing treatment be done after spraying? The sprayed zinc layer contains micro-pores; if not sealed, moisture easily enters and forms white rust. Low-viscosity epoxy sealing paint penetrating the pores can significantly improve density and corrosion resistance, and is an indispensable process.
Q: How long can the zinc sprayed coating last? Under the premise of standard construction with sealing and topcoat, it can reach 30–50 years in marine atmospheric environments, far exceeding ordinary painting systems, with lower life-cycle cost.
Further Reading
- Heavy-duty anti-corrosion coating system: Complete matching from primer to topcoat
- Water-based micaceous iron oxide coating: Water-based long-term protection for heavy-duty anti-corrosion steel structures
- Product center: Zinc wire ZW
- New coating national standard GB 30981 2026 upgrade, water-basedization is inevitable