Nanocoatings are a new type of high-performance coating based on nanomaterials and surface modification technology, offering excellent anti-corrosion, waterproofing, wear resistance, and self-cleaning properties. They are widely used in industrial equipment, construction, marine, and new energy sectors, providing an innovative solution for the upgrading of conventional coatings.
I. Definition and Technical Background of Nanocoatings
Nanocoating refers to the introduction of functional materials with nanoscale particle sizes (typically less than 100 nm) into a coating system, which are uniformly dispersed in the coating via physical or chemical means and form a highly dense, stable, and functionally specialized protective layer with the substrate surface during film formation.
Unlike traditional paints that mainly rely on resin film formation, nanocoatings place more emphasis on material scale control and interface structure design. Due to their ultra-high specific surface area and quantum size effect, nanoparticles enable the coating to maintain excellent protective performance even at extremely thin thicknesses, which is exactly the core value of nanocoating technology.
From an application perspective, nanocoatings are not a single product, but a class of comprehensive coating solutions that integrate materials science, surface engineering, and chemical modification.

II. Core Mechanisms of Nanotechnology in Coatings
1. Structural densification induced by the nanoscale
Nanomaterials can effectively fill the micro-pores and defects that are inevitably present in conventional coatings, making the internal structure of the coating more compact and significantly reducing the permeation rates of water, oxygen, and corrosive media. This property enables nano anti-corrosion coatings to maintain long-term stable performance even in harsh environments.
2. Surface Energy Regulation and Functionalization Realization
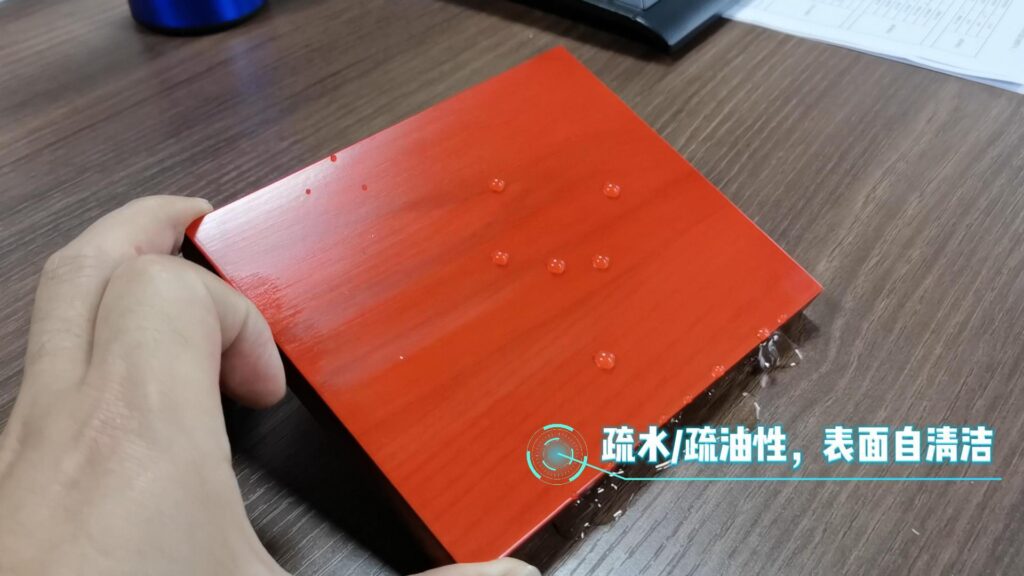
Through nanoscale surface modification technology, the surface energy of coatings can be precisely regulated, thereby endowing them with properties such as hydrophobicity, oleophobicity, antifouling, and self-cleaning. Such nano-coatings perform particularly prominently on building exterior walls, industrial equipment surfaces, and in complex environments.
3. Interfacial adhesion is significantly enhanced
Nanoparticles can form a multi-point anchoring structure between the substrate and the coating, greatly enhancing adhesion. This structure not only improves the coating's peel resistance but also extends the overall service life.
III. Essential Differences Between Nanocoatings and Conventional Coatings
| Comparison Dimension | Traditional Coatings | Nano Coatings |
|---|---|---|
| Material Scale | Micrometer-level | Nanometer-level |
| Structural Density | Average | Extremely High |
| Protection Mechanism | Single Physical Isolation | Multiple Barriers + Surface Regulation |
| Service Life | Relatively Short | Significantly Extended |
| Function Expansion | Limited | Customizable Multi-function |
Essentially, a nanocoating is not simply a "finer paint," but a high-performance coating system that achieves a leap in properties through microstructural reconstruction.

IV. Main Performance Advantages of Nanocoatings
1. Excellent anti-corrosion and rust-proof performance
Nanocoatings effectively block corrosive media through a multi-layer protective structure and are widely used in steel structures, pipelines, chemical equipment, and other fields.
2. Excellent abrasion resistance and impact resistance
Nanomaterials enhance the overall strength of the coating, enabling it to remain intact under mechanical friction and impact conditions.
3. Long-lasting waterproof and antifouling performance
The unique surface structure makes it difficult for water droplets and contaminants to adhere, reducing maintenance costs.
4. Good weather resistance and aging resistance
It maintains stable performance even in complex environments such as ultraviolet radiation, high temperature, and heat and humidity.
V. Typical Application Fields of Nanocoatings
- Industrial equipment and heavy-duty anti-corrosion engineering
- Protection of building exterior walls and steel structures
- Ships, offshore engineering, and port facilities
- Petrochemical and Energy Systems
- New energy equipment and high-end manufacturing sector
With continuous industrial upgrading and increasingly stringent environmental requirements, industrial nanocoatings are gradually becoming a crucial choice for high-end coating engineering.


VI. Development Trends of Nanocoatings
In the future, nanocoatings will continue to evolve toward high functional integration, environmental friendliness, and customized solutions. Through the composite application of different nanomaterials, coatings will no longer be merely "protective layers," but functional surface systems with multiple values.