Imprimación epoxi rica en zinc Epoxy Zinc-Rich Primer
Two-component epoxy polyamide/zinc-rich heavy-duty anticorrosive primer — sacrificial anode cathodic protection
Epoxy Zinc-Rich Primer is a high-performance two-component anticorrosive primer that uses epoxy resin and polyamide curing agent as the film-forming material, with ultrafine zinc powder (dry film content ≥70%) as the main antirust pigment. The coating provides active corrosion protection through the sacrificial anode cathodic protection mechanism of zinc powder on steel—even if the paint film is locally damaged, the surrounding zinc powder continues to provide electrochemical protection for the exposed steel. It complies with the Class 2 standard of HG/T 3668-2020 "Epoxy Zinc-Rich Primer." When used in combination with an epoxy micaceous iron oxide intermediate coat and a polyurethane/fluorocarbon topcoat, the system achieves neutral salt spray resistance ≥1000h, meeting the requirements of ISO 12944 C4-C5 high-corrosion environments. It is widely used as an anticorrosive primer for major projects such as sea-crossing bridges, offshore oil platforms, petrochemical storage tanks, transmission towers, wind turbine towers, and large steel structure factories.
ProductsDescripción general
Resumen del producto: ¿para quién? ¿qué problema resuelve?
Epoxy zinc-rich primer is a heavy-duty anticorrosive primer designed for steel structures requiring long-term corrosion protection of over 15 years in C4-C5 high-corrosion environments.The core problem it solves is that ordinary anti-rust paint fails within 3–5 years in harsh environments such as coastal areas, chemical atmospheres, and high humidity. In contrast, epoxy zinc-rich primer, through the dual mechanism of "cathodic protection + barrier protection," can provide 15–25 years of long-term protection when used with an intermediate coat and topcoat—significantly reducing the full life cycle maintenance cost.
Definición del producto
Epoxy Zinc-Rich Primer, Chinese standard number HG/T 3668-2020, is a two-component (2K) ambient temperature crosslinking and curing anticorrosive primer using epoxy resin (bisphenol A type, CAS 25068-38-6) and polyamide curing agent (CAS 68410-23-1) as film-forming substances, ultrafine spherical zinc powder (CAS 7440-66-6, particle size 3-8 μm, mass fraction in dry film ≥70%) as anticorrosive pigment, and xylene/n-butanol as the solvent system.
Mecanismo de protección anticorrosiva:High-content zinc powder particles in the coating form continuous conductive pathways between themselves and with the steel substrate. Since the standard electrode potential of zinc (-0.76V vs SHE) is lower than that of iron (-0.44V), zinc acts as the anode in corrosion microcells and preferentially undergoes oxidation (Zn → Zn²⁺ + 2e⁻). The released electrons flow through the conductive network to the steel surface, cathodically polarizing the steel below its immune potential—this is known as "sacrificial anode cathodic protection." Meanwhile, the corrosion products of zinc (ZnO, Zn(OH)₂, basic zinc carbonate, etc.) gradually fill the coating pores, forming a dense secondary barrier layer—the "corrosion product self-healing effect."
Datos de rendimiento clave:
- The dry film zinc powder content is ≥70% (compliant with HG/T 3668-2020 Category 2).
- Contenido de sólidos en volumen ≥60 % (ISO 3233:1998)
- Adherencia por método de tracción ≥ 6 MPa (ISO 4624:2016, con dolly de 20 mm de diámetro para la prueba).
- Resistencia a la niebla salina neutra (NSS) de una sola capa ≥ 400 h (ISO 9227:2022, ancho de corrosión en la línea de rayado ≤ 2 mm).
- Sistema combinado (imprimación epoxi rica en zinc 80 μm + capa intermedia epoxi de mica de hierro 150 μm + pintura de poliuretano 80 μm) Resistencia a NSS ≥ 1000 h.
- Mixed application period: 4-8 hours (23°C, main agent: curing agent = 10:1 w/w)
Sustratos aptos y limitaciones:Applicable to carbon steel, low-alloy steel, and cast iron substrates blasted to Sa2.5 (ISO 8501-1:2007). Not recommended for direct application on galvanized steel (the passivation film on the zinc surface will block the conductive path—sweep blasting pretreatment or an epoxy primer transition layer is advised), stainless steel (the surface passivation film must be removed first), or aluminum alloy (risk of galvanic corrosion—the potential difference between zinc and aluminum is too large). Application temperature limits: standard type 5–40°C (below 5°C, the epoxy-amine crosslinking reaction rate is extremely low, resulting in incomplete coating curing).
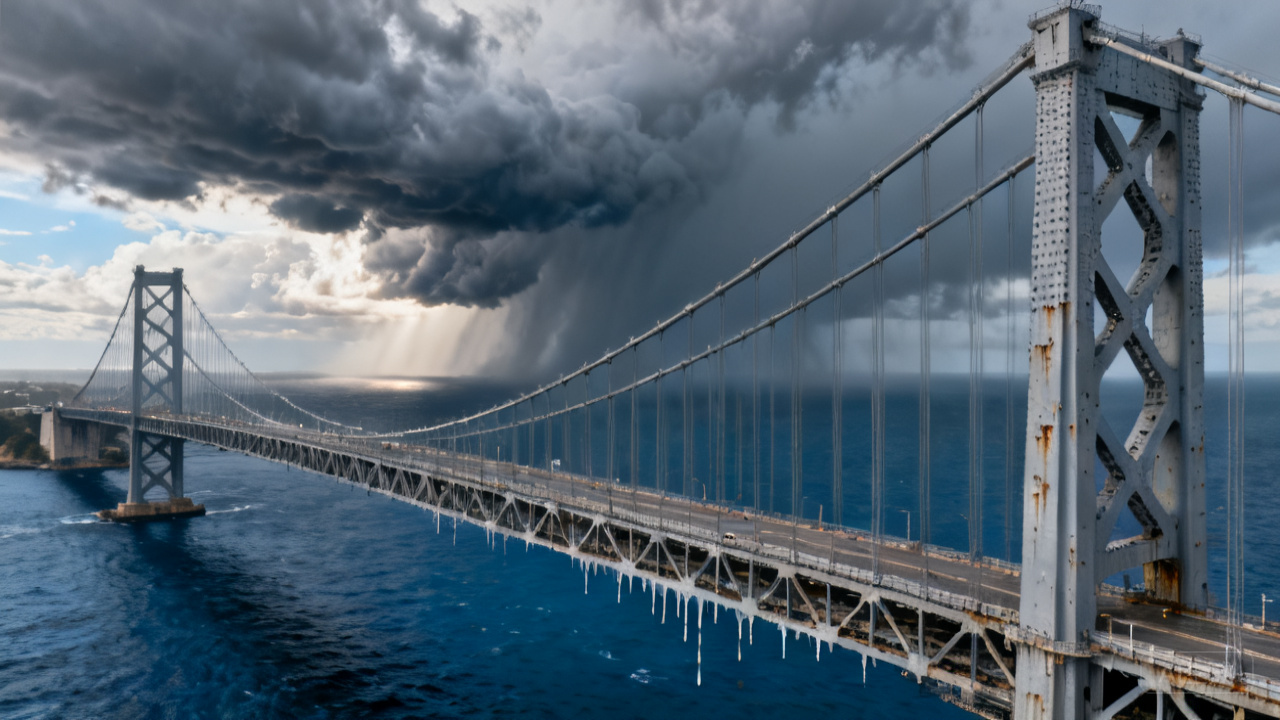
Posición en el sector y aplicaciones:Epoxy zinc-rich primer is one of the most widely used primer types in global heavy-duty anticorrosive coating systems (ISO 12944-5:2019 systems A2.08/A3.08/A4.08, etc.), forming a classic triple protection system together with epoxy micaceous iron oxide intermediate paint and polyurethane/fluorocarbon/polysiloxane topcoat. Typical application projects include: Japan's Akashi Kaikyo Bridge (opened in 1998, design life of 100 years), Hong Kong-Zhuhai-Macao Bridge (opened in 2018, 500,000 m² of steel box girders), and the Beihai offshore oil platform (NORSOK M-501 system certified). According to Grand View Research data, the global zinc-rich primer market size in 2023 was approximately USD 2.8 billion, with the Asia-Pacific region accounting for a 48% share.
ProductsFeatures
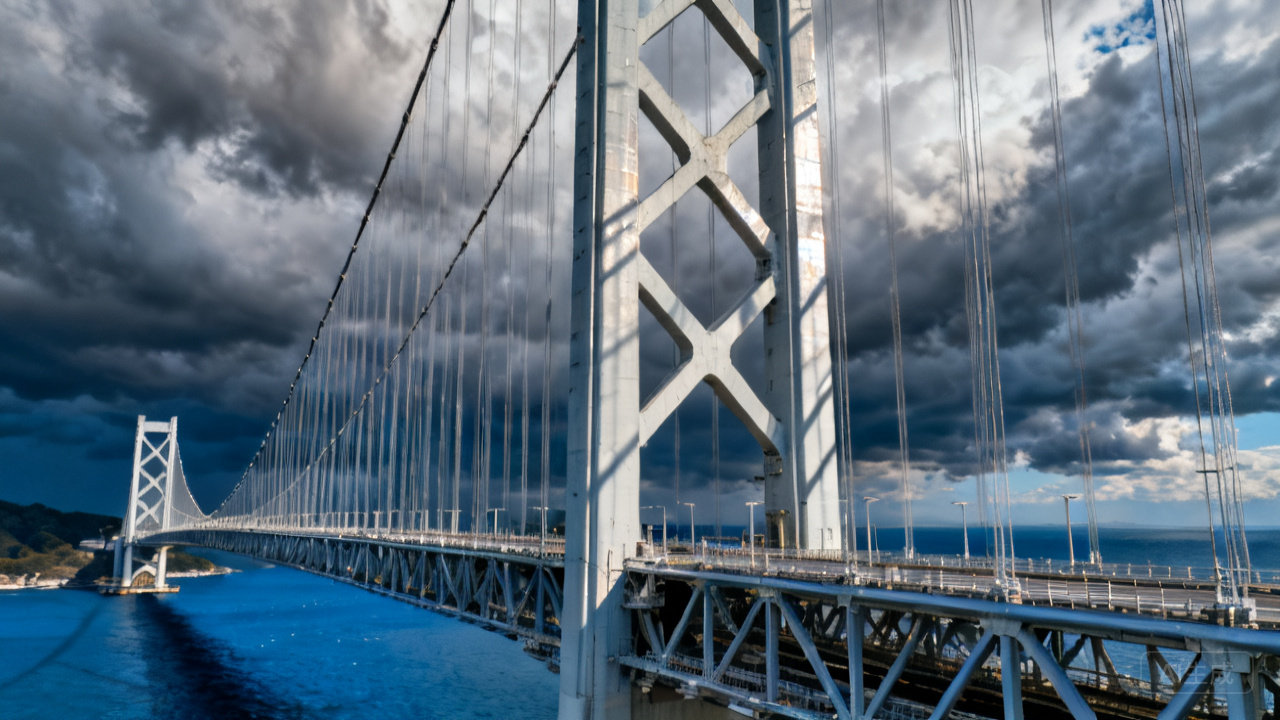
1. Mecanismo de protección catódica (ánodo de sacrificio)
The dry film of the coating contains ≥70% zinc powder, forming a continuous conductive network. The standard electrode potential of zinc (-0.76V) is lower than that of iron (-0.44V). When corrosion occurs, zinc is preferentially oxidized (Zn → Zn²⁺ + 2e⁻), releasing electrons that cathodically polarize the steel to an immune potential—even if the coating has 3-5mm of damage, the surrounding zinc powder can still provide continuous electrochemical protection for the exposed steel. This makes the anti-corrosion performance of epoxy zinc-rich primer far superior to that of ordinary anti-rust primers that rely solely on physical shielding.
2. Resistencia a la corrosión y durabilidad superiores
Single coating NSS ≥ 400h (HG/T 3668 Type 2), system NSS ≥ 1000h after matching with epoxy micaceous iron oxide intermediate paint + polyurethane topcoat. Designed service life of 15-25 years under ISO 12944-2 C5-M very high corrosivity environment (marine splash zone). The Akashi Kaikyo Bridge in Japan adopted an epoxy zinc-rich primer system in 1998, and the coating has remained intact for over 25 years—actual service life far exceeds the design value.
3. Excelente compatibilidad
It exhibits excellent interlayer adhesion (pull-off test ≥5 MPa) with epoxy micaceous iron oxide intermediate paint (MIO barrier layer), polyurethane topcoat (weather-resistant decorative layer), fluorocarbon topcoat (super weather-resistant, ≥25 years), and polysiloxane topcoat (high weather resistance + high chemical resistance). The combination of epoxy zinc-rich primer, epoxy micaceous iron oxide intermediate paint, and topcoat is the most classic heavy-duty anti-corrosion three-coat system in the ISO 12944-5 standard—where the primer provides cathodic protection, the intermediate coat supplies thickness and physical barrier, and the topcoat offers weather resistance and decoration.
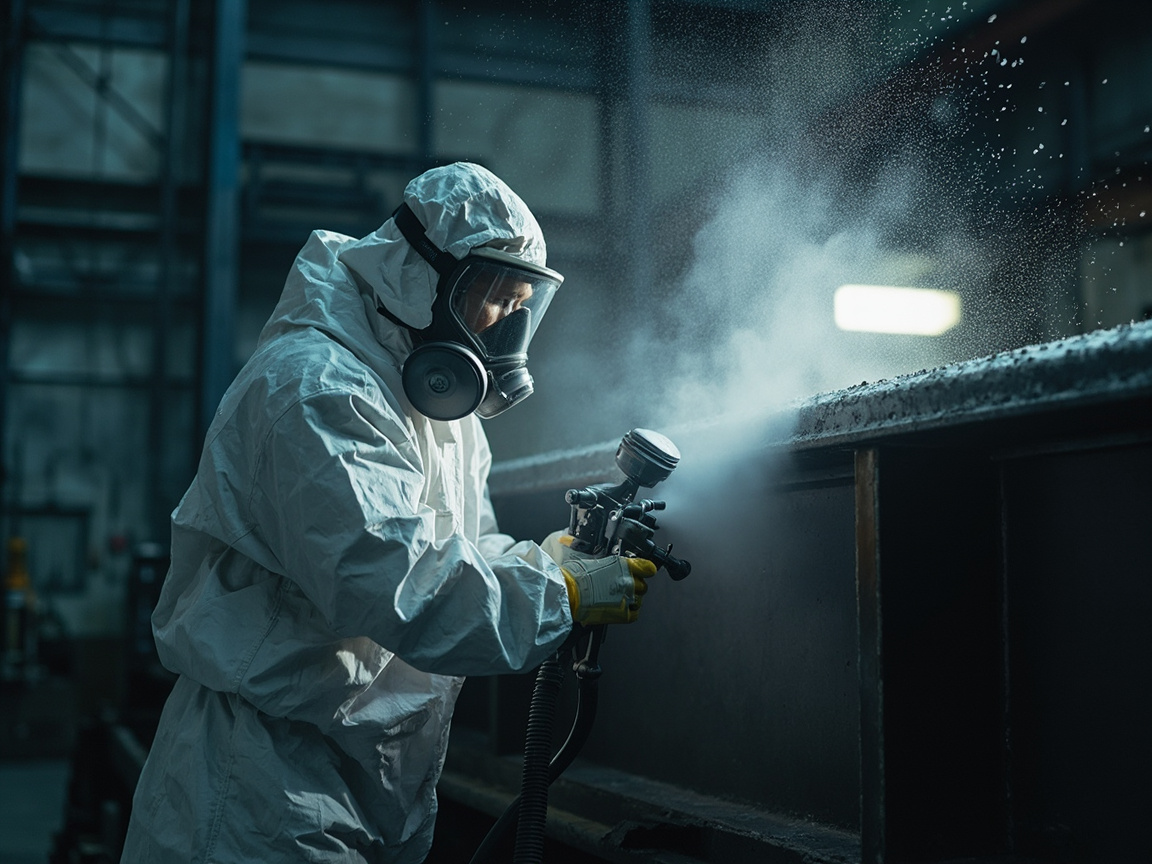
4. Amplia adaptabilidad de aplicación
Supports airless spray (nozzle 0.43–0.53 mm, 15–25 MPa), air spray, and brush/roller application (for small-area touch-ups). Single-pass dry film thickness: 60–80 μm. Mixing ratio: 10:1 (w/w). Pot life: 4–8 h (23°C). Wide temperature range for application (5–40°C); low-temperature formulation can be applied down to –5°C. Continuous stirring is required during spraying to prevent zinc powder sedimentation—use of a pressure pot with a pneumatic agitator is recommended to ensure coating uniformity.
5. Imprimación de taller soldable (Shop Primer)
Specialized formulation (dry film 15-25μm) can be used as a shop primer—after application in the steel structure prefabrication plant, the steel remains suitable for welding and cutting. Welding fumes comply with occupational exposure limits (GBZ 2.1-2019), and the pass rate of X-ray inspection of welds is not affected. Suitable for automated spray painting on steel structure production lines—parts can be handled and stacked within 3-5 minutes after spraying. Note: Only the specialized shop primer formulation is weldable—the standard type with a dry film thickness of 60-80μm is not suitable for welding.
6. Cumplimiento ambiental: estándares globales
Complies with HG/T 3668-2020 (China) Standard Class 2, ISO 12944-5:2019 system numbers A2.08/A3.08/A4.08, NORSOK M-501:2022 (Norwegian Petroleum Industry) System 1, SSPC Paint 20 (USA) Zinc-rich Primer Type II (≥77% zinc powder). VOCs<420g/L(GB 30981-2020),可通过ROHS 2011/65/EU和REACH (EC) 1907/2006Cumplimiento normativoTesting。Products碳足迹约2.8kg CO₂e/kg(摇篮到大门,SimaPro 9.5计算)——低于Imprimante inorgánico rico en zinc(3.5kg CO₂e/kg)。
TécnicoParameters
Parámetros fisicoquímicos
Secado y rendimiento
· Marzo de 2024: Informe de ensayo del Centro Nacional de Inspección y Ensayo de Calidad de Recubrimientos (N.º: NTC-2024-0315-ZR).
HG/T 3668-2020 "Epoxy Zinc-Rich Primer" Type 2 Indicators
· Los datos de esta tabla son valores típicos en condiciones estándar de laboratorio (23±2 °C, 50±5% HR). Los valores reales pueden variar ligeramente según el estado del sustrato, el proceso de aplicación y las condiciones ambientales. Contacte al soporte técnico para obtener el COA (Certificado de Análisis) por lote.
ApplicationProcess
Preparación de la superficie
Granallado hasta grado Sa2.5 (ISO 8501-1:2007), con rugosidad Rz 40-75 μm. La limpieza manual debe ser ≥ St3. Las grasas deben eliminarse con disolvente según SSPC-SP1. Aplicar la capa de imprimación dentro de las 4 horas posteriores al granallado (HR<50%可延至8h)。禁忌:雨天/雾天/Temperatura del sustrato低于露点3°C时禁止Application。
Preparación de la mezcla
Stir the main agent for 3-5 minutes until the zinc powder is completely and evenly dispersed. Add the curing agent at a ratio of 10:1 (w/w) and continue stirring for 3-5 minutes. Let it stand for 15-30 minutes (23°C) to mature. Continuously stir during application to prevent zinc powder from settling—a pneumatic mixer is recommended. The mixed usable period is 4-8 hours (23°C). Do not dilute and use materials that have gelled beyond this period.
Aplicación de imprimación
Boquilla recomendada para pulverización sin aire: 0.43-0.53 mm / 0.017-0.021 pulgadas, presión 15-25 MPa. Pulverización con aire: boquilla 1.5-2.0 mm, presión 0.3-0.5 MPa. Brocha/rodillo solo para pre-recubrimiento y retoques en áreas pequeñas. DFT por capa 60-80 μm. Pre-recubrir soldaduras, bordes libres, etc.
Secado y repintado
Surface dry ≤ 1h (23°C), hard dry ≤ 24h. Minimum recoating interval 8h (23°C). Maximum recoating interval 7d—exceeding this interval requires sandblasting (low pressure 0.2-0.3MPa, non-metallic abrasive) to remove surface zinc salts (basic zinc carbonate). Matching: Epoxy micaceous iron oxide intermediate coat 100-150μm → Polyurethane/fluorocarbon topcoat 50-80μm × 2.
Inspection and Acceptance
Medición DFT (ISO 2808:2019, SSPC-PA2): el 80% de los puntos de medición ≥ valor especificado, sin puntos de medición.<80%规定值。AdherenciaTesting(Ensayo de adherencia por arrancamiento ISO 4624或ISO 2409Método de corte cruzado)。detección de picaduras(Método de esponja húmeda,67.5V/90V)。Inspección visual:无Descuelgue/漏涂/起泡/缩孔/Polvo de zinc不均匀。
AplicacionesField/Area
Puentes marítimos / fluviales
Cajones de acero, torres de puente, nervios de arco
Plataforma petrolera marina
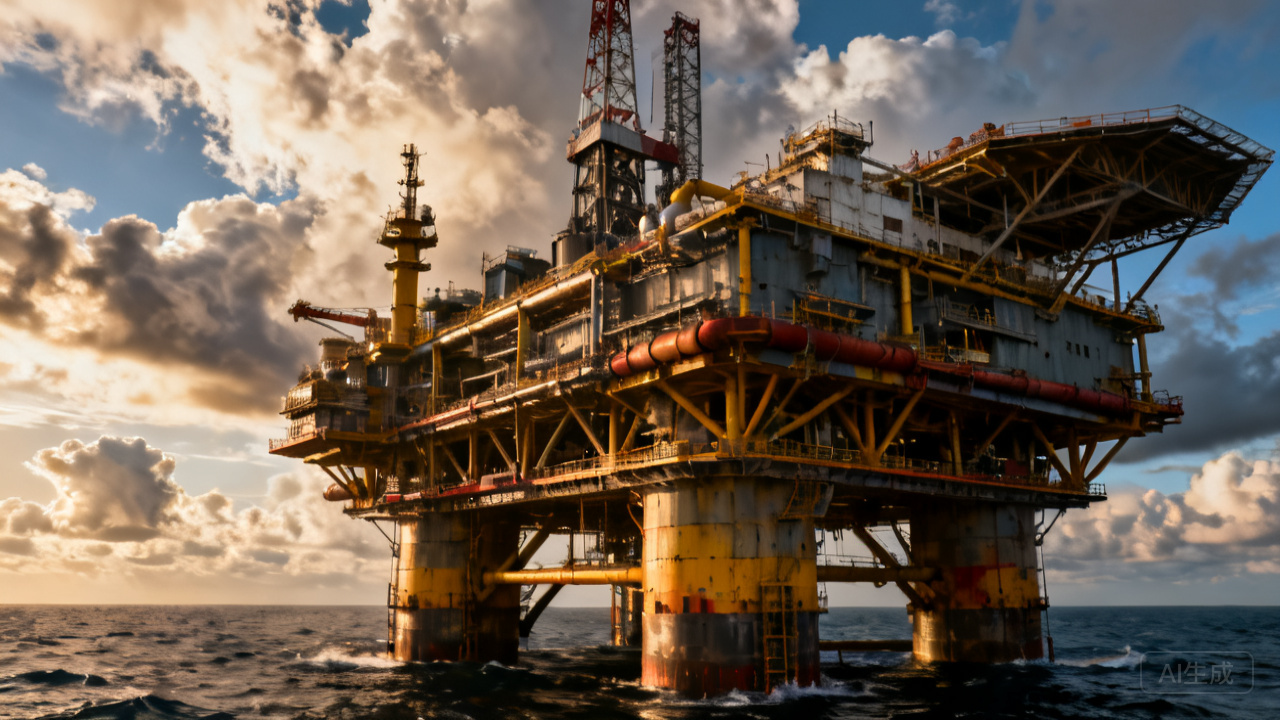
Jackets, cubiertas, módulos habitacionales
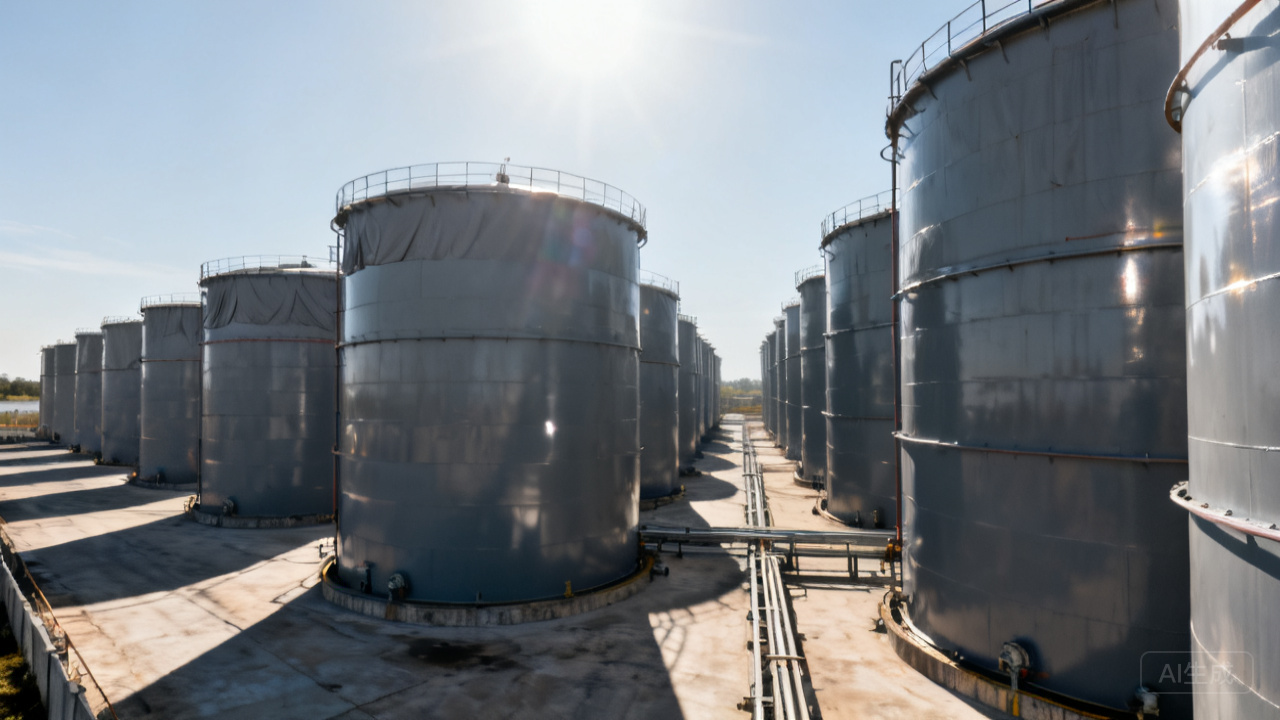
Paredes exteriores de tanques petroquímicos
Tanques de crudo / productos refinados / productos químicos
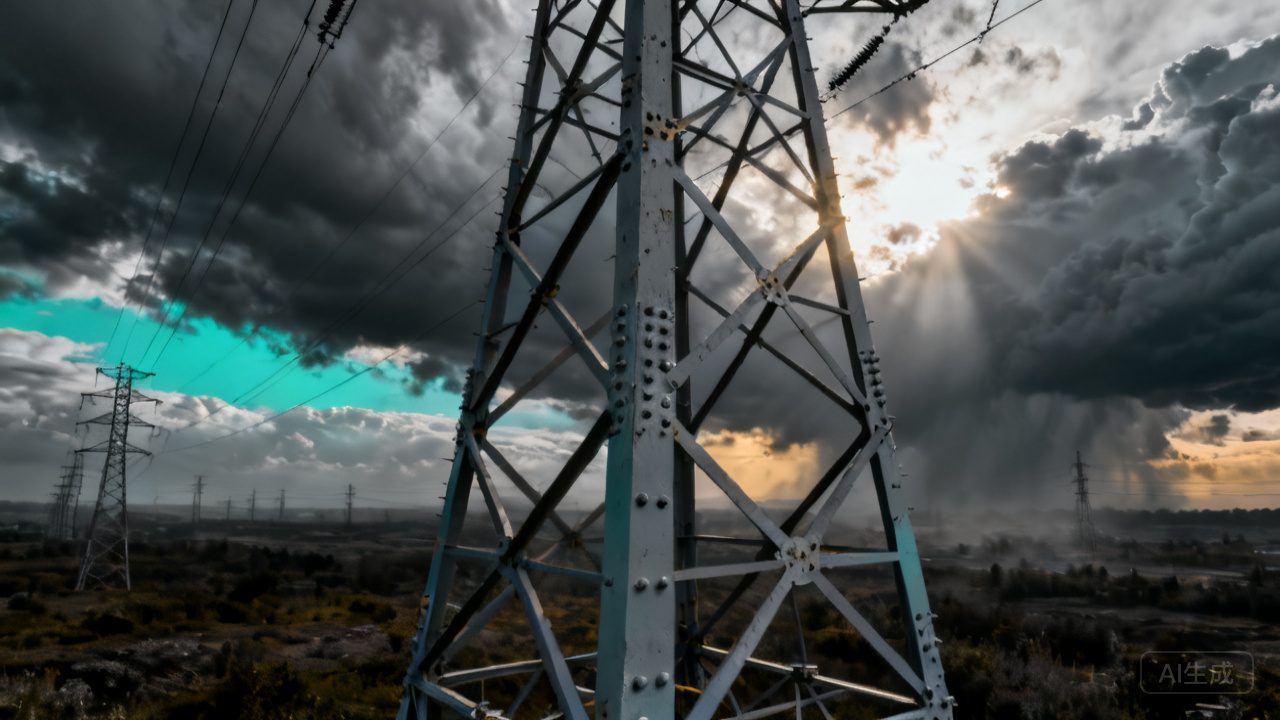
Torres de transmisión / torres tubulares
Estructuras de acero para líneas de alta / muy alta tensión
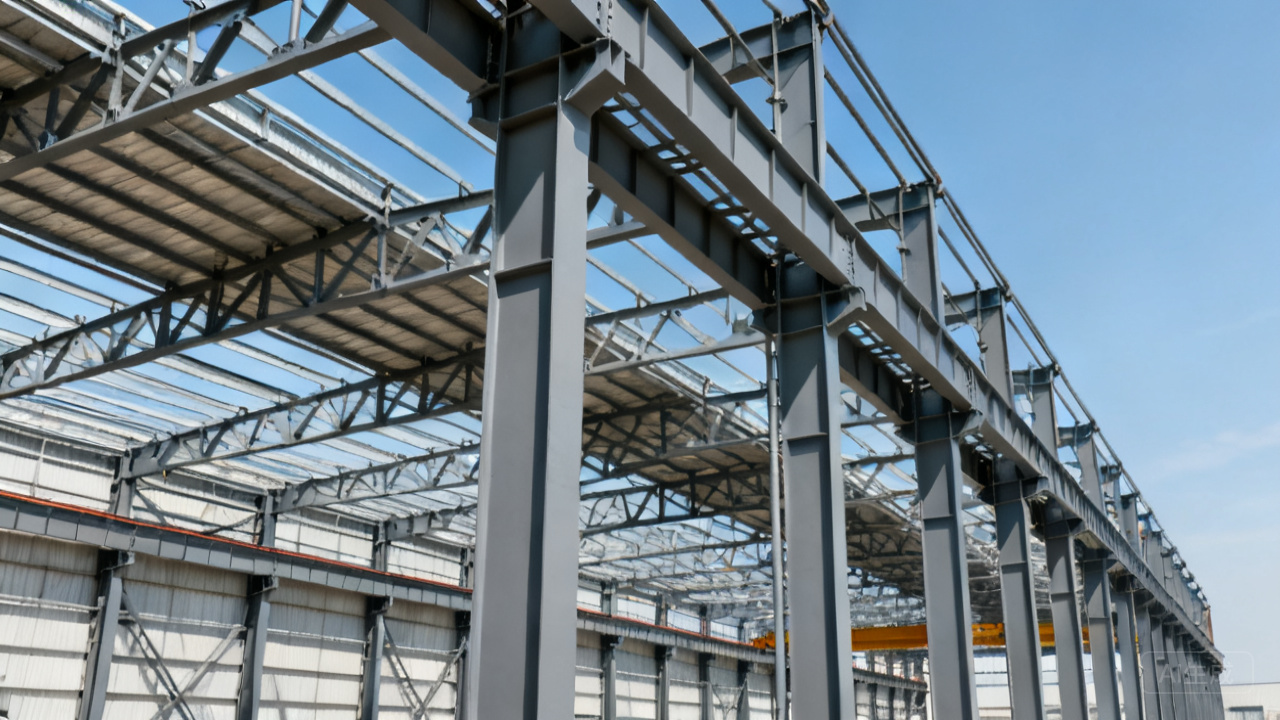
Grandes naves de estructura metálica
Naves industriales, recintos deportivos
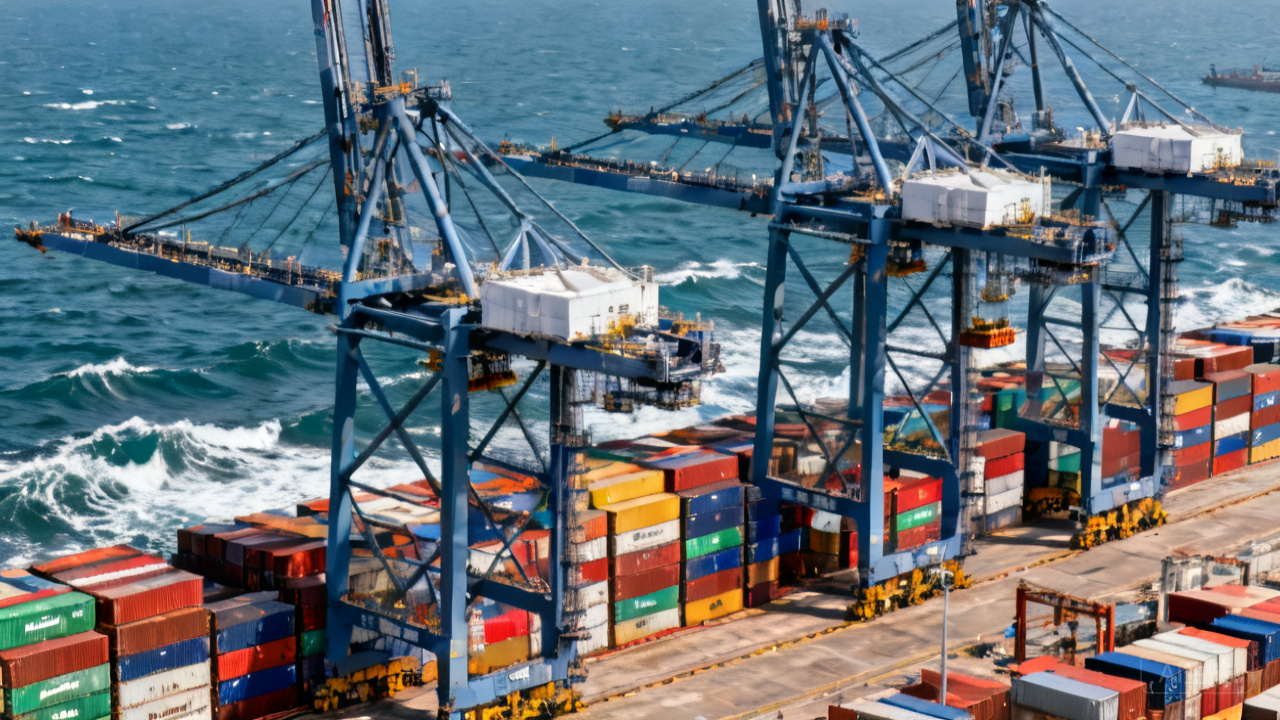
Maquinaria portuaria
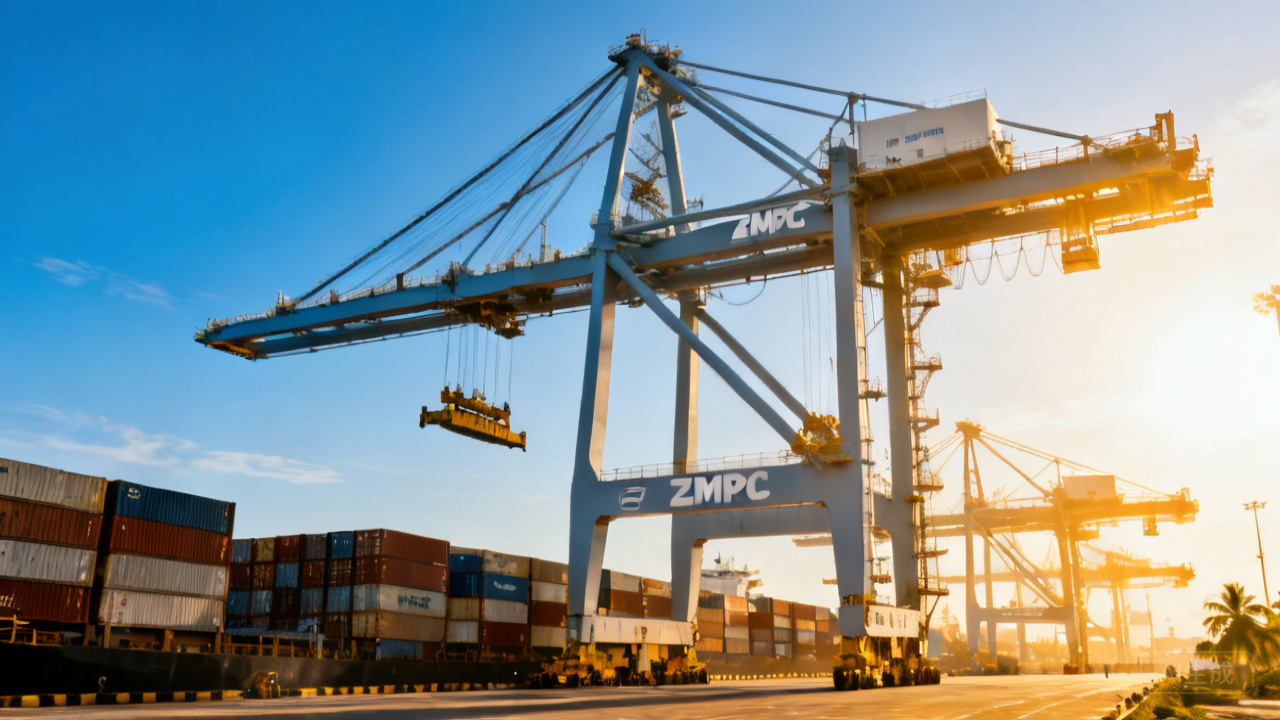
Grúas de muelle, grúas pórtico, descargadores de barcos
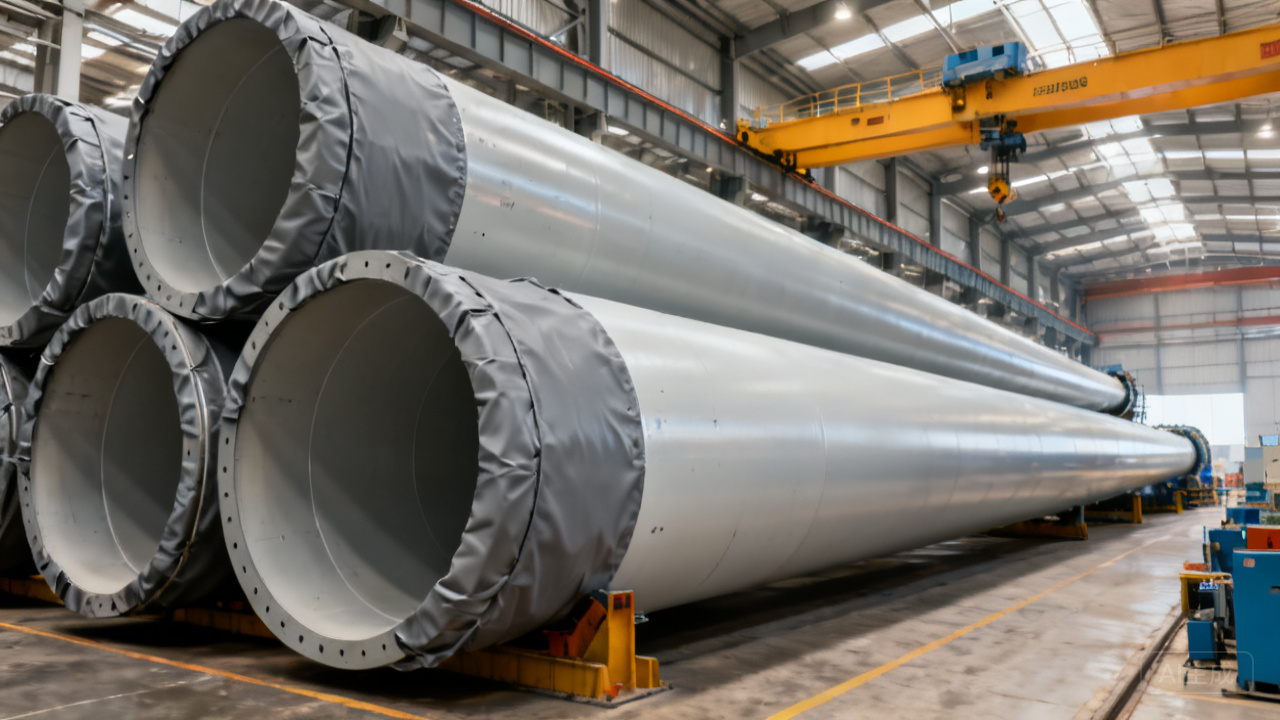
Torres de aerogeneradores
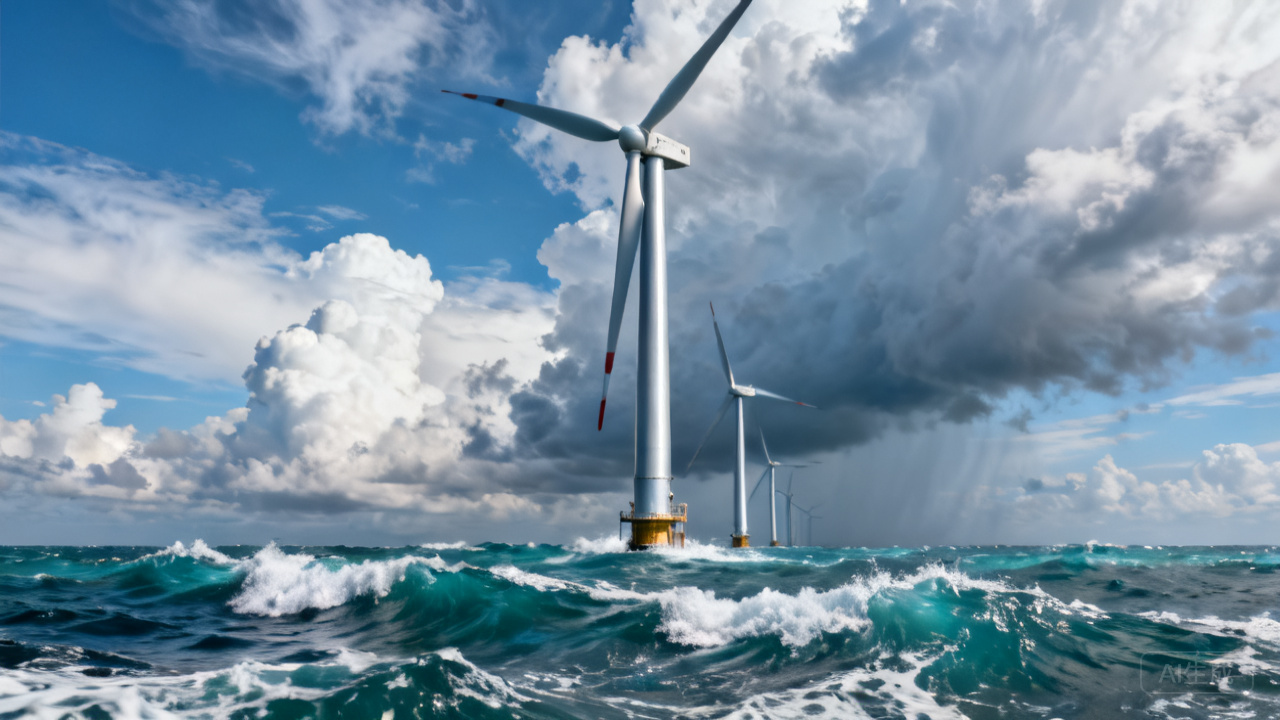
Torres de aerogeneradores terrestres / marinos
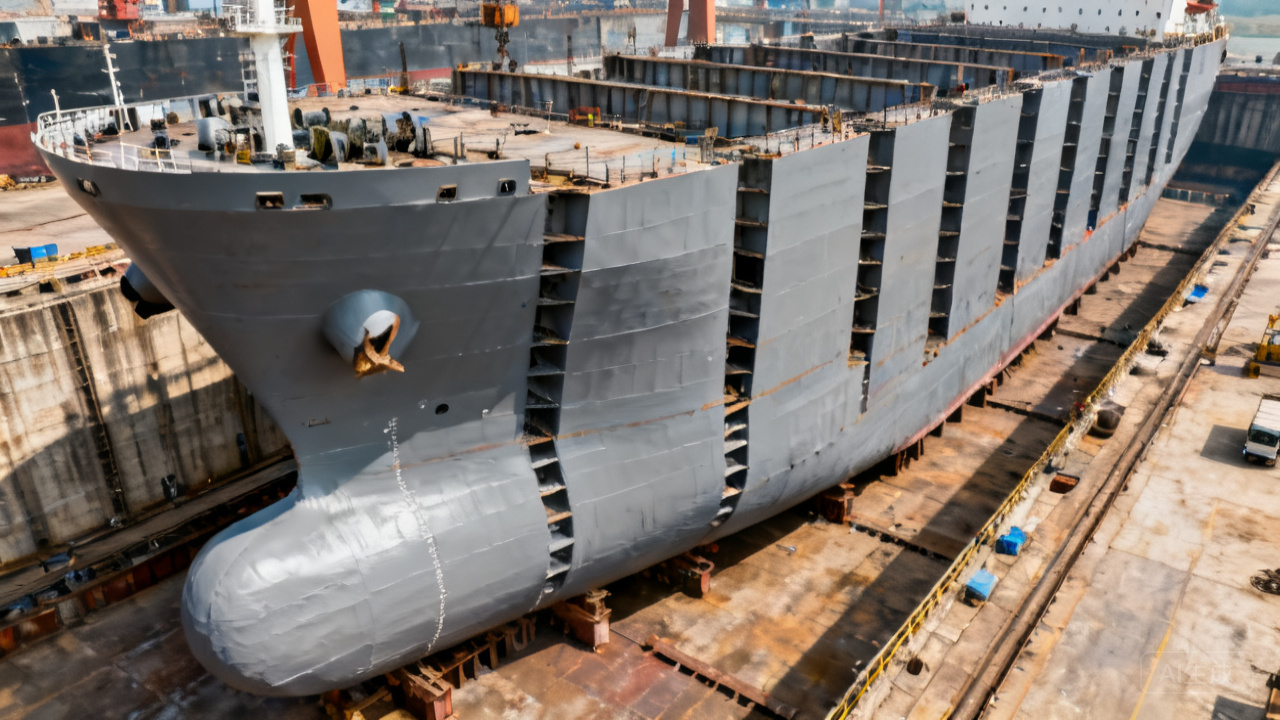
Construcción naval e ingeniería offshore
Bloques de casco, tanques de lastre, cubiertas
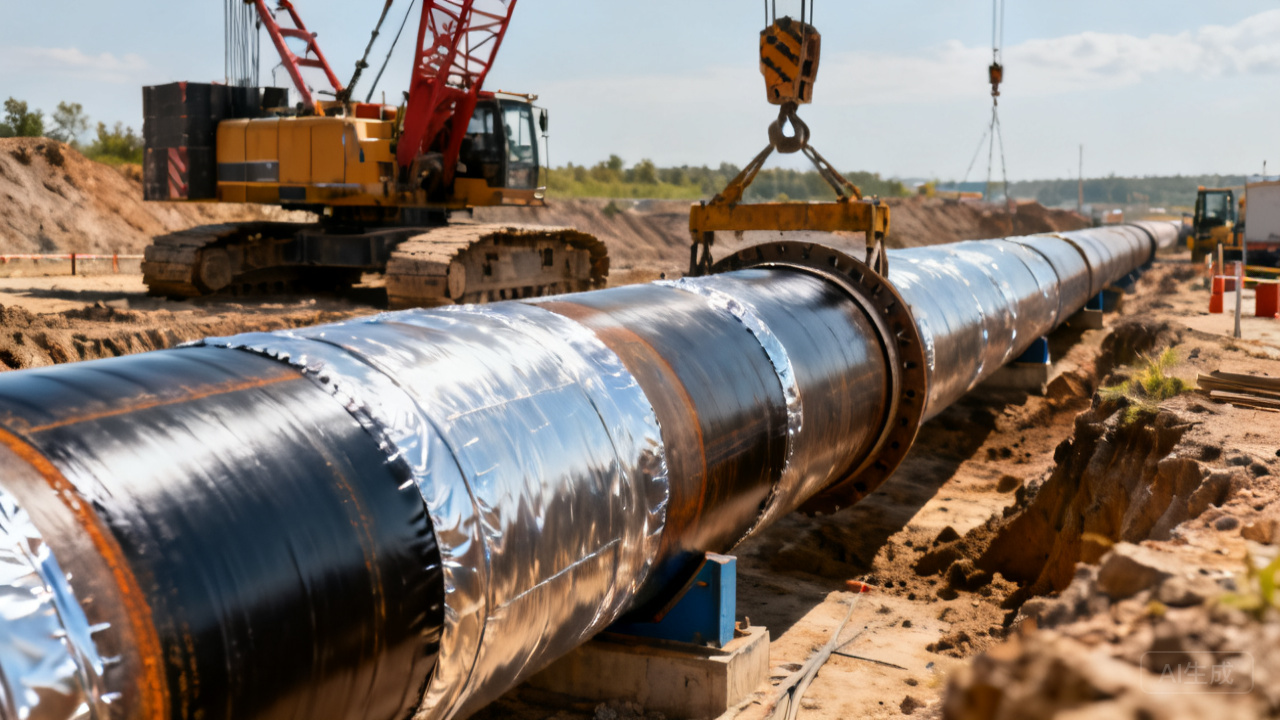
Anticorrosión de paredes externas de tuberías
Tuberías de larga distancia de petróleo, gas y agua
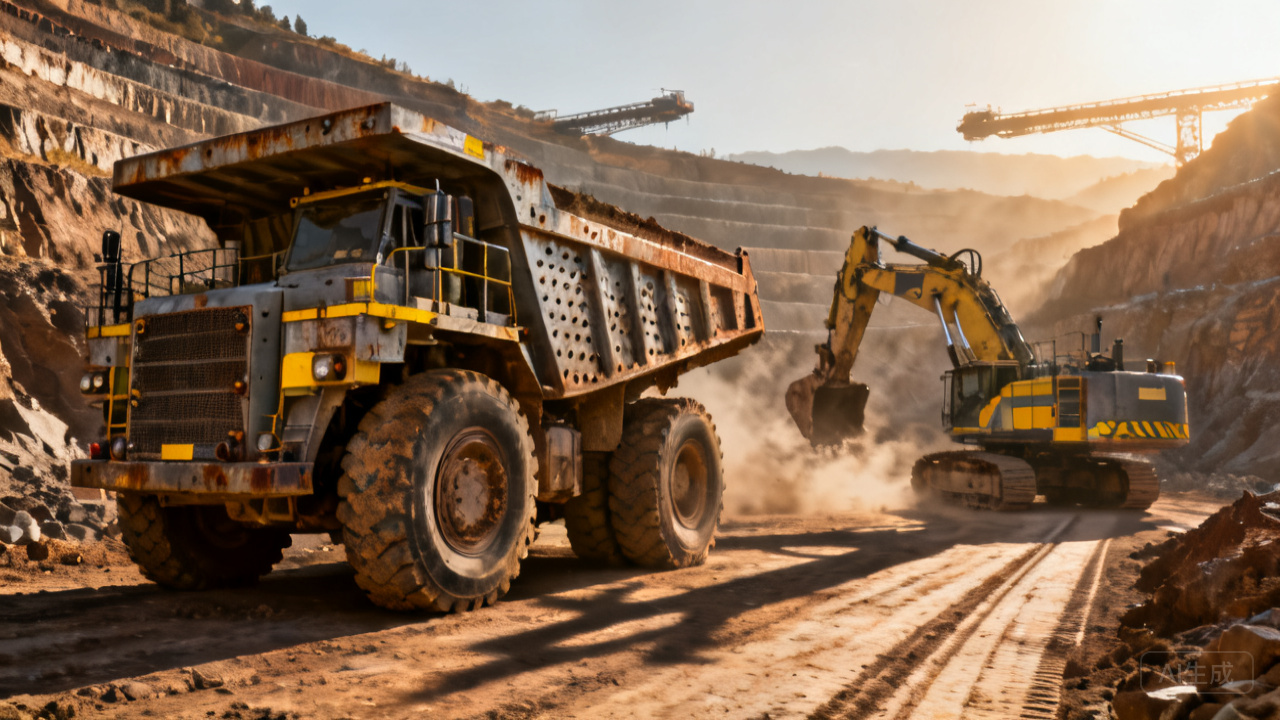
Maquinaria minera / de construcción
Excavadoras, trituradoras, equipos de transporte
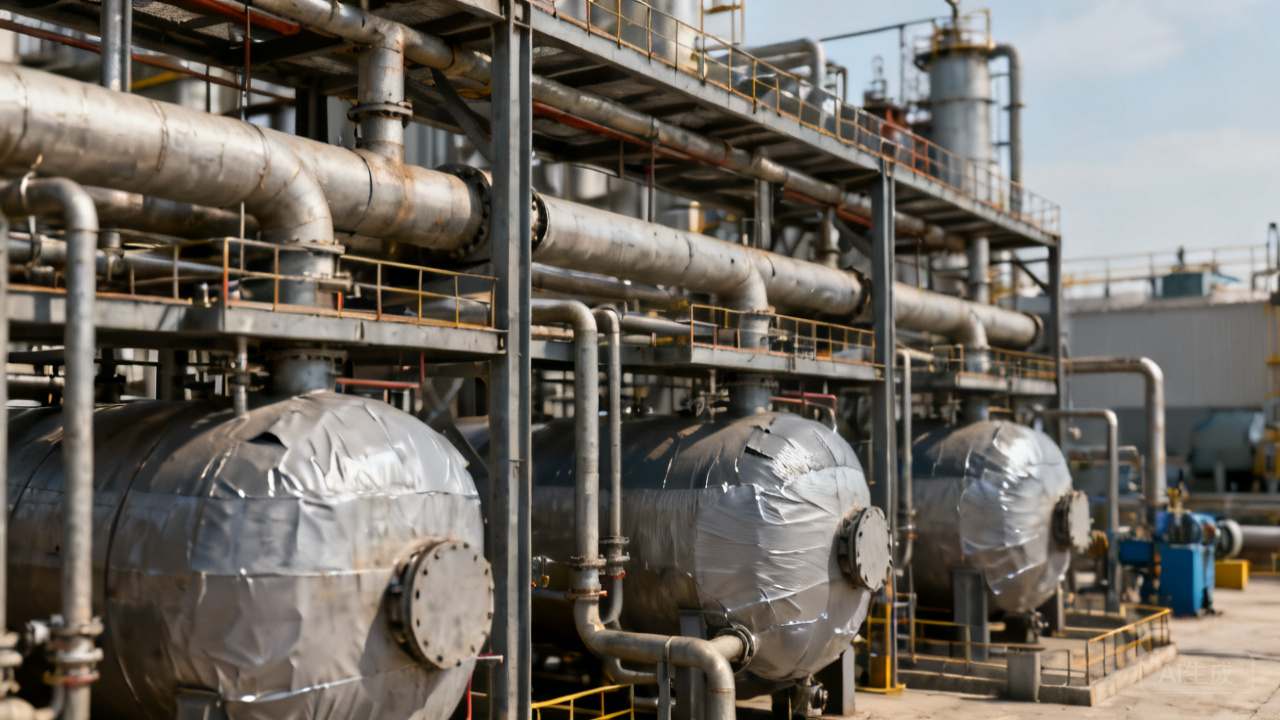
Instalaciones químicas / de refino
Reactores, intercambiadores de calor, estructura de racks de tuberías
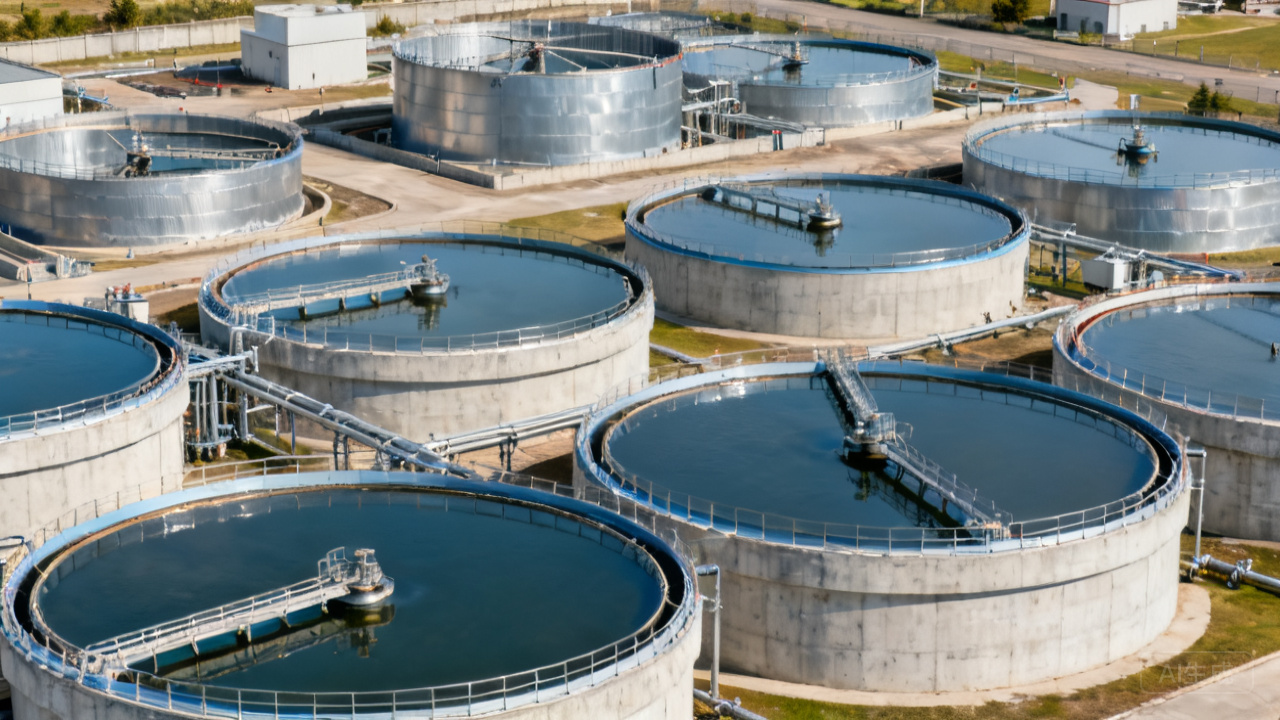
Tratamiento de agua / infraestructuras hidráulicas
Depuradoras, compuertas, rejillas de retención
Preguntas Frecuentes -FAQ
DescargarCentro
TDS - Ficha técnica del producto
Technical Data Sheet
Conforme a la norma HG/T 3668-2020
MSDS - Ficha de datos de seguridad de materiales
Material Safety Data Sheet
16 capítulos · GB/T 16483-2008
Tarjeta de colores del producto
Color Card
Colores estándar gris acero / rojo hierro
Guía de aplicación
Application Guide
Guía completa de aplicación + Solución de defectos
proyectoCasos
Anticorrosión de los cajones de acero del Puente Akashi Kaikyo, Japón
Anticorrosión de altas prestaciones para jackets de plataformas petrolíferas offshore del Mar del Norte
Anticorrosión de las grúas de muelle para contenedores ZPMC del Puerto de Chennai, India
Protección anticorrosión de torres eólicas en un parque eólico marino en el Mar del Sur de China
Epoxy Zinc-Rich Primer·Venta directa de fábrica
Muestras gratuitas para pruebas · Personalización de soluciones técnicas · Asistencia in situ · Fábrica certificada ISO 9001 · Respuesta rápida en 48 horas.
artículos y noticias relacionados
Para saber más: artículos técnicos y noticias del sector de Kexin New Materials