HG/T 3668-2020 Type 2 · Dry film zinc content ≥70%

エポキシジンクリッチプライマー Epoxy Zinc-Rich Primer

二液型エポキシポリアミド/亜鉛粉末重防食プライマー — 犠牲陽極陰極防食

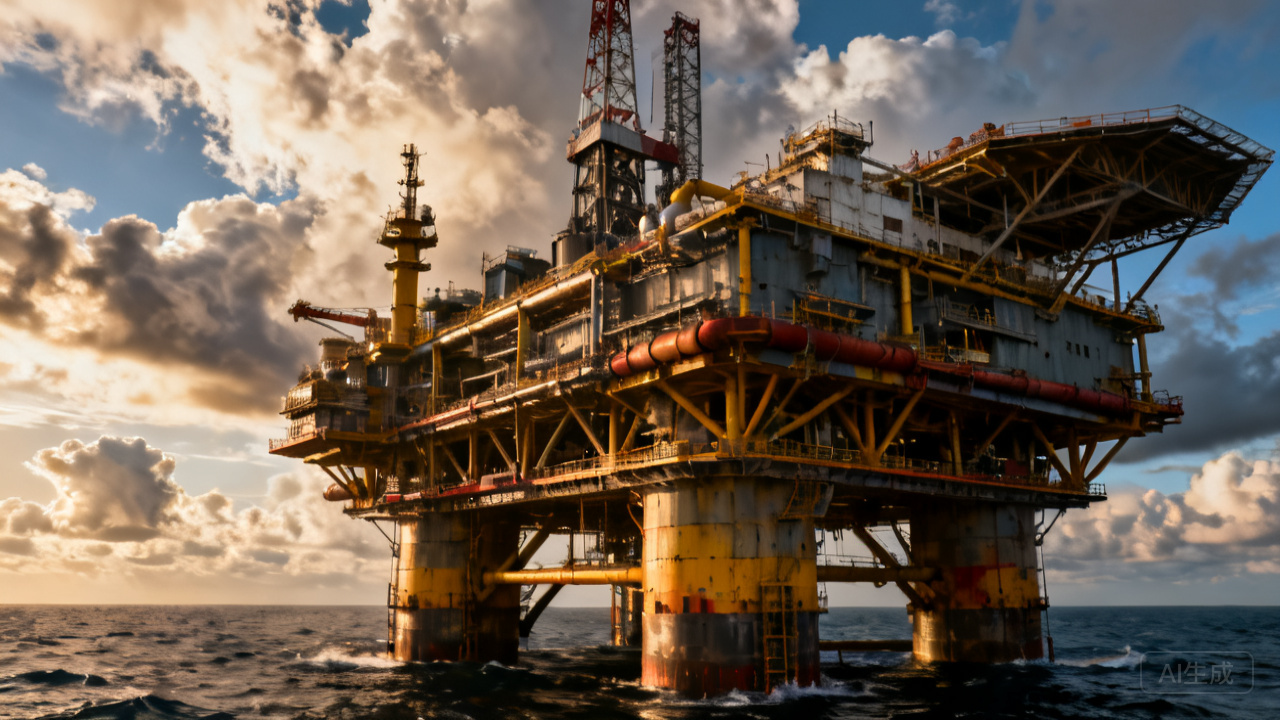
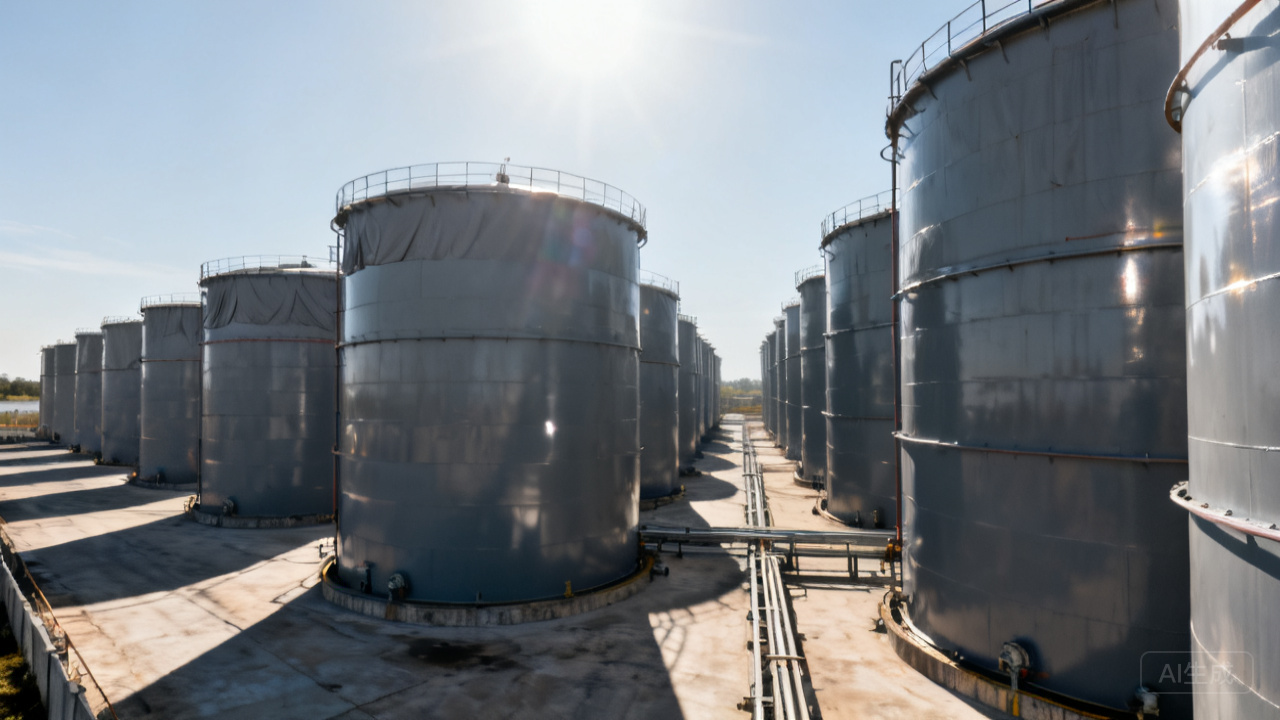
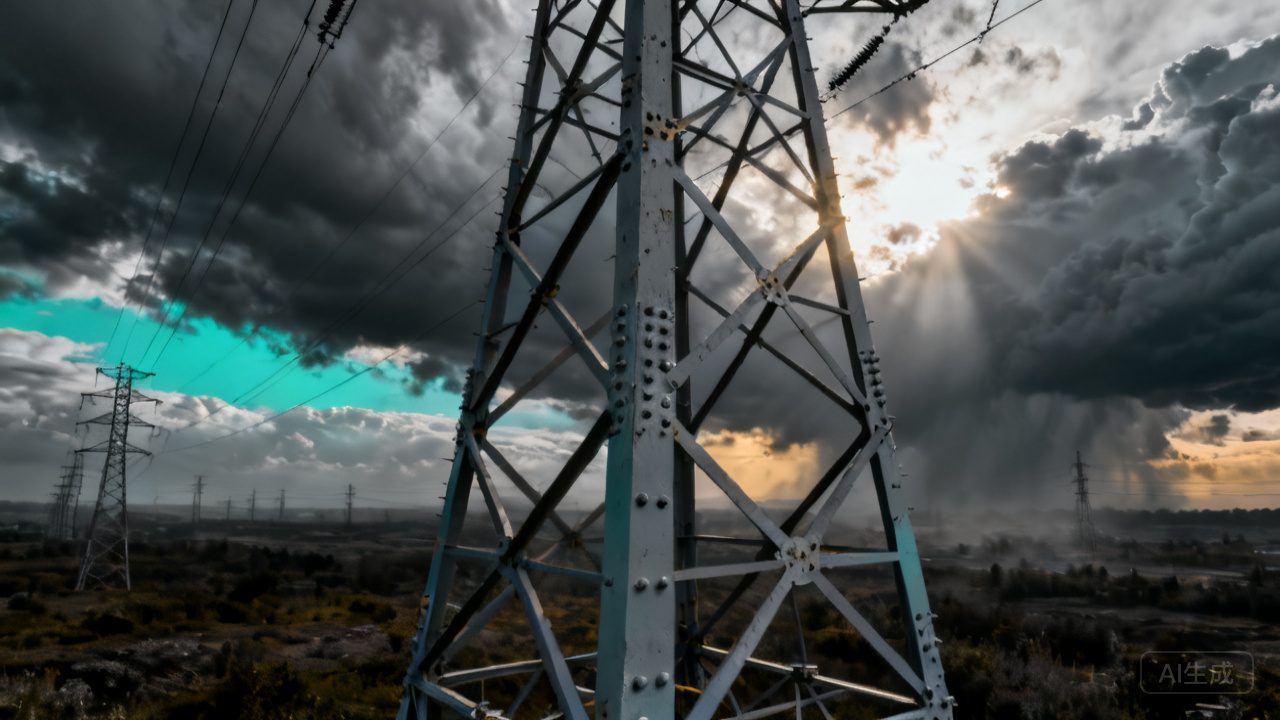
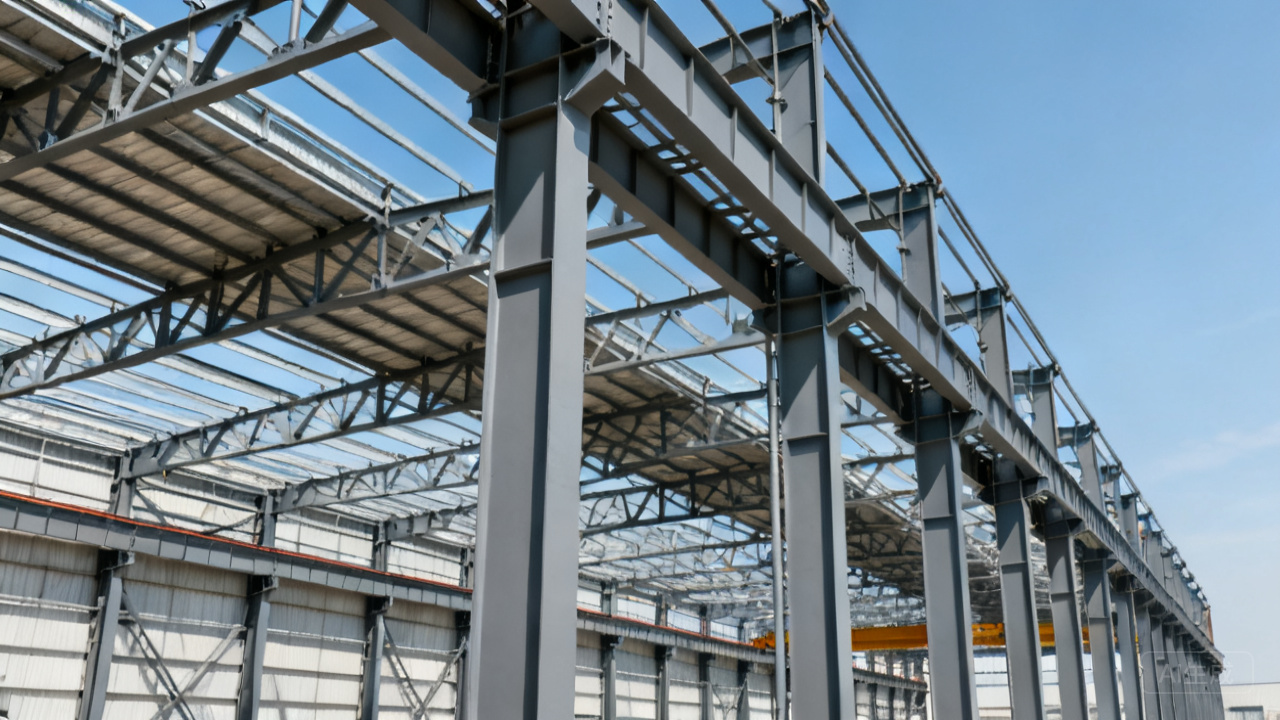
エポキシジンクリッチプライマー(Epoxy Zinc-Rich Primer)は、エポキシ樹脂とポリアミド硬化剤を皮膜形成物質とし、超微細亜鉛粉末(乾燥膜含有量≥70%)を主な防錆顔料とする高性能二液型防食プライマーです。塗膜は亜鉛粉末による鋼材への犠牲陽極・陰極防食機構により能動的な防食を提供します。塗膜が局部的に損傷しても、周囲の亜鉛粉末が露出した鋼材に持続的に電気化学的防食を施します。HG/T 3668-2020「エポキシジンクリッチプライマー」2類基準に適合し、エポキシマイカ状酸化鉄中塗りとポリウレタン/フッ素樹脂上塗りを組み合わせたシステムでは、耐中性塩水噴霧性≥1000hを達成し、ISO 12944 C4-C5高腐食環境グレードの要求を満たします。跨海大橋、海洋石油プラットフォーム、石油化学タンク、送電鉄塔、風力発電タワー、大型鉄骨構造工場など、重要プロジェクトの防食下塗りとして広く使用されています。

≥70%
乾燥塗膜中の亜鉛末含有量
1000h+
体系耐塩霧
≥6MPa
プルオフ方式付着力
≥60%
体積固形分
HG/T3668
製品適用規格
Sa2.5
素地処理等級
5~40°C
施工環境温度
2K/Two-Component10:1
混合比率
ISO12944
C4-C5腐食レベル

製品概要

製品概要:誰向けか?どんな問題を解決するか?

エポキシジンクリッチプライマーは、C4~C5の高腐食環境において15年以上の長期防食保護を必要とする鋼構造物向けに設計された重防食下塗りである。本製品が解決する核心的な課題は、通常の防錆塗料が沿岸部、化学工業大気、高湿度などの過酷な環境下で3~5年で効果を失うのに対し、エポキシジンクリッチプライマーは「カソード防食+遮蔽防護」の二重メカニズムにより、中間塗料および上塗り塗料と組み合わせることで15~25年の長期防護を実現し、ライフサイクル全体のメンテナンスコストを大幅に低減する点である。

製品の定義

エポキシジンクリッチプライマー(Epoxy Zinc-Rich Primer)、中国規格番号HG/T 3668-2020は、エポキシ樹脂(ビスフェノールA型、CAS 25068-38-6)とポリアミド硬化剤(CAS 68410-23-1)を皮膜形成物質とし、超微細球状亜鉛粉末(CAS 7440-66-6、粒径3-8μm、乾燥皮膜中の質量分率≥70%)を防錆顔料とし、キシレン/n-ブタノールを溶剤系とする二液型(2K)常温架橋硬化型防食プライマーである。

防食メカニズム:コーティング中に高含有量の亜鉛粉末粒子間、および亜鉛粉末と鋼材基材との間に連続的な導電経路が形成される。亜鉛の標準電極電位(-0.76V vs SHE)が鉄(-0.44V)よりも低いため、腐食マイクロ電池において亜鉛はアノードとして優先的に酸化反応(Zn→Zn²⁺+2e⁻)を起こし、放出された電子は導電ネットワークを通じて鋼材表面へ流れ、鋼材をカソード分極させて免蝕電位以下にする——これが「犠牲アノード陰極防食」である。同時に、亜鉛の腐食生成物(ZnO、Zn(OH)₂、塩基性炭酸亜鉛など)が徐々にコーティングの空隙を充填し、緻密な二次遮蔽層を形成する——「腐食生成物自己修復効果」。

主要性能データ:

  • 乾燥膜亜鉛粉末含有量は70%以上である(HG/T 3668-2020 カテゴリー2に準拠)。
  • Volume solids content ≥60% (ISO 3233:1998)
  • Pull-off adhesion ≥6 MPa (ISO 4624:2016, test doll diameter 20mm)
  • Single coating resistance to neutral salt spray (NSS) ≥400h (ISO 9227:2022, rust width at the crisscrossing ≤2mm)
  • 完全なシステム(80μmの亜鉛リッチエポキシ + 150μmの雲母状酸化鉄中間層 + 80μmのポリウレタン上塗り層)は、1000時間以上のNSS耐性を有する。
  • Mixed application period: 4-8 hours (23°C, main agent: curing agent = 10:1 w/w)

適用素地と制限:Applicable to carbon steel, low-alloy steel, and cast iron substrates blasted to Sa2.5 (ISO 8501-1:2007). Not recommended for direct application on galvanized steel (the passivation film on the zinc surface will block the conductive path—sweep blasting pretreatment or an epoxy primer transition layer is advised), stainless steel (the surface passivation film must be removed first), or aluminum alloy (risk of galvanic corrosion—the potential difference between zinc and aluminum is too large). Application temperature limits: standard type 5–40°C (below 5°C, the epoxy-amine crosslinking reaction rate is extremely low, resulting in incomplete coating curing).

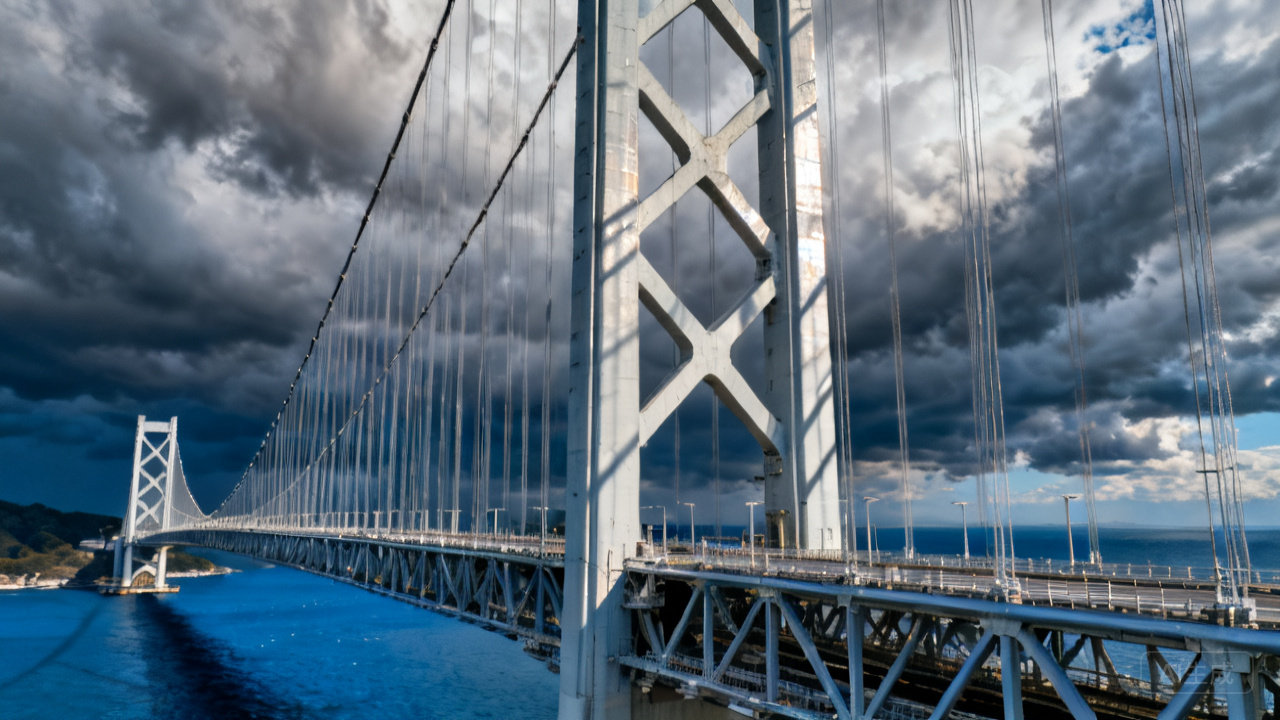
業界での位置づけと用途:エポキシジンクリッチプライマーは、世界の重防食塗装システム(ISO 12944-5:2019 システムA2.08/A3.08/A4.08等)において最も広く使用されているプライマーの一種であり、エポキシマイカ状酸化鉄中塗り、ポリウレタン/フッ素/ポリシロキサン上塗りと組み合わせて、古典的な三重防護システムを構成します。代表的な適用プロジェクトとしては、日本の明石海峡大橋(1998年開通、設計寿命100年)、香港・珠海・マカオ大橋(2018年開通、50万m²の鋼箱桁)、北海海上石油プラットフォーム(NORSOK M-501システム認証取得)などがあります。Grand View Researchのデータによると、2023年の世界の亜鉛リッチプライマー市場規模は約28億米ドルで、アジア太平洋地域が48%のシェアを占めています。

製品Features
阴极保护牺牲阳极原理

1. 陰極防食(犠牲陽極)のメカニズム

塗膜乾膜中に70%以上の亜鉛粉末が含まれ、連続導電ネットワークを形成する。亜鉛の標準電極電位(-0.76V)は鉄(-0.44V)より低く、腐食発生時には亜鉛が優先的に酸化(Zn→Zn²⁺+2e⁻)し、電子を放出して鋼材を陰極分極させ、不働態電位に到達させる。これにより、塗膜に3~5mmの損傷があっても、周囲の亜鉛粉末が露出した鋼材に持続的な電気化学的防食を提供する。このため、エポキシジンクリッチプライマーの防食性能は、物理的遮蔽のみに依存する一般的な防錆プライマーをはるかに上回る。
耐盐雾测试1000小时

2. 優れた耐腐食性と耐久性

単層塗膜NSS≥400h(HG/T 3668 2類)、エポキシ雲母酸化鉄中塗り+ポリウレタン上塗りを組み合わせた系ではNSS≥1000h。ISO 12944-2のC5-M極高腐食環境(海洋飛沫帯)において設計耐用年数15~25年。日本の明石海峡大橋は1998年にエポキシジンクプライマー系を採用し、25年以上経過した現在も塗膜は良好な状態を維持——実耐用年数は設計値を大幅に上回る。
重防腐涂层配套体系

3. 優れた互換性

エポキシ雲母酸化鉄中塗り(MIO遮蔽層)、ポリウレタン上塗り(耐候性・装飾層)、フッ素樹脂上塗り(超耐候性・25年以上)、ポリシロキサン上塗り(高耐候性+高耐薬品性)のいずれに対しても、優れた層間付着力(剥離試験で5MPa以上)を有する。エポキシジンクプライマー+エポキシ雲母酸化鉄中塗り+上塗りは、ISO 12944-5体系における最も古典的な重防食3層システムである。プライマーはカソード防食、中塗りは膜厚と物理的遮蔽、上塗りは耐候性と装飾性を提供する。
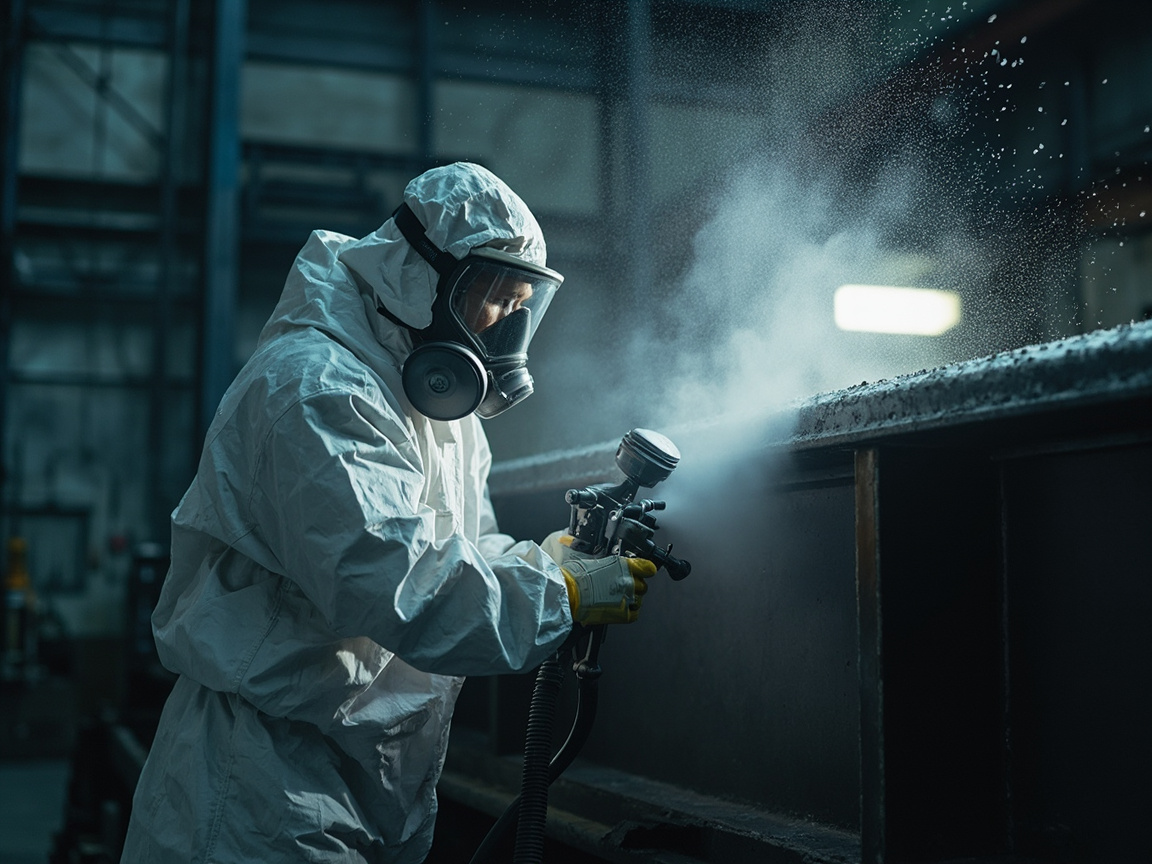
无气喷涂施工

4. 建設現場への幅広い適応性

エアレススプレー(ノズル0.43-0.53mm、15-25MPa)、エアスプレー、刷毛塗り/ローラー塗り(小面積補修)に対応。1回塗りの乾燥膜厚60-80μm、混合比10:1(重量比)、可使時間4-8時間(23°C)。広い温度範囲での施工が可能(5-40°C)、低温用処方では-5°Cまで対応。スプレー塗装中は亜鉛粉の沈殿を防ぐため継続的な撹拌が必要——エア駆動撹拌機付き圧力タンクの使用により塗料の均一性を確保することを推奨。
车间底漆焊接应用

5. ショッププライマーのはんだ付け性

Specialized formulation (dry film 15-25μm) can be used as a shop primer—after application in the steel structure prefabrication plant, the steel remains suitable for welding and cutting. Welding fumes comply with occupational exposure limits (GBZ 2.1-2019), and the pass rate of X-ray inspection of welds is not affected. Suitable for automated spray painting on steel structure production lines—parts can be handled and stacked within 3-5 minutes after spraying. Note: Only the specialized shop primer formulation is weldable—the standard type with a dry film thickness of 60-80μm is not suitable for welding.
环保合规高固含

6.環境コンプライアンス・グローバルスタンダード

HG/T 3668-2020(中国)規格クラス2、ISO 12944-5:2019システム番号A2.08/A3.08/A4.08、NORSOK M-501:2022(ノルウェー石油産業)システム1、SSPCペイント20(米国)亜鉛リッチプライマータイプII(亜鉛粉末77%以上)に準拠。VOCs<420g/L(GB 30981-2020),可合格ROHS 2011/65/EU和REACH (EC) 1907/2006コンプライアンスTesting。製品碳足迹约2.8kg CO₂e/kg(摇篮到大门,SimaPro 9.5计算)——低于無機リッチ亜鉛下塗り(3.5kg CO₂e/kg)。

技術Parameters

物理化学パラメータ

製品タイプ2液型エポキシポリアミド/亜鉛粉塗料(2K EP/Zn)
乾燥塗膜中の亜鉛末含有量70%以上(HG/T 3668-2020 カテゴリー2)
体積固形分60±3%(ISO 3233:1998)
質量基準固形分85±3%(GB/T 1725-2007)
密度(混合後)2.10-2.30 g/cm³(20°C)
混合比率(重量)Main agent: curing agent = 10:1
ポットライフ4-8h(23°C)/ 2h(35°C)
推奨ドライフィルム厚さ(DFT)60~80μm/チャンネル
理論塗布率0.17-0.22 kg/m²(75μm DFT)
VOC含有量<420 g/L(GB 30981-2020)
Packaging Specsベース剤30kg + 硬化剤キット3kg

乾燥と性能

指触乾燥時間≤1時間(23℃、GB/T 1728-2020 方法B)
乾燥硬化時間≤24時間(23℃、GB/T 1728-2020 方法A)
完全硬化7日間(23℃、DSC法によりTgが安定)
最小再塗間隔8h(23°C)
最大再塗間隔7 days (23°C; sand removal is required if the expiration date is exceeded)
プルオフ方式付着力≥6 MPa(ISO 4624:2016,dolly Ø20mm)
クロスカット付着≤1レベル(ISO 2409:2020、間隔1mm)
耐衝撃性≥50 kg·cm(GB/T 1732-2020)
中性塩水噴霧(NSS)耐性Single coating ≥400h / Complete system ≥1000h (ISO 9227:2022)
連続使用温度-20°C ~ 150°C
技術パラメータの根拠
• March 2024, National Coatings Quality Inspection and Testing Center Test Report (No.: NTC-2024-0315-ZR)
HG/T 3668-2020「エポキシジンクプライマー」第2類指標
この表のデータは、標準的な実験室条件下(23±2℃、50±5%RH)における代表値です。実際の値は、基材の状態、施工工程、環境条件によって若干異なる場合があります。バッチごとのCOA(認定証明書)については、テクニカルサポートまでお問い合わせください。

ApplicationProcess

1

表面処理

サンドブラスト処理はSa2.5(ISO 8501-1:2007)まで行い、表面粗さRzは40~75μmとする。手作業による錆除去はSt3以上とする。グリースはSSPC-SP1溶剤を用いて除去すること。プライマー塗布(RH)はサンドブラスト処理後4時間以内に完了すること。<50%可延至8h)。禁忌:雨天/雾天/下地温度低于露点3°C时禁止Application。

2

塗料調合

Stir the main agent for 3-5 minutes until the zinc powder is completely and evenly dispersed. Add the curing agent at a ratio of 10:1 (w/w) and continue stirring for 3-5 minutes. Let it stand for 15-30 minutes (23°C) to mature. Continuously stir during application to prevent zinc powder from settling—a pneumatic mixer is recommended. The mixed usable period is 4-8 hours (23°C). Do not dilute and use materials that have gelled beyond this period.

3

下塗り施工

Airless spraying (recommended): Nozzle 0.43-0.53mm/0.017-0.021", pressure 15-25MPa. Air spraying: Nozzle 1.5-2.0mm, pressure 0.3-0.5MPa. Brush/roller coating is only suitable for small-area pre-coating and repair. Single-coat DFT 60-80μm. Pre-coat welds, free edges, etc.

4

乾燥と塗り重ね

表面乾燥 ≤ 1 時間 (23 °C)、完全乾燥 ≤ 24 時間。最小再塗装間隔 8 時間 (23 °C)。最大再塗装間隔 7 日—この間隔を超えると、表面の亜鉛塩 (塩基性炭酸亜鉛) を除去するためにサンドブラスト (低圧 0.2 ~ 0.3 MPa、非金属研磨材) が必要になります。マッチング: エポキシ雲母状酸化鉄中間コート 100 ~ 150 μm → ポリウレタン/フッ素樹脂トップコート 50 ~ 80 μm × 2。

5

検査・検収

DFT measurement (ISO 2808:2019, SSPC-PA2): 80% of measuring points ≥ specified value, no measuring points<80%规定值。付着性Testing(ISO 4624 プルオフ試験或ISO 2409クロスカット法)。ピンホール検知(湿式スポンジ法,67.5V/90V)。外観検査:无流挂/漏涂/起泡/缩孔/亜鉛粉不均匀。

用途Field/Area
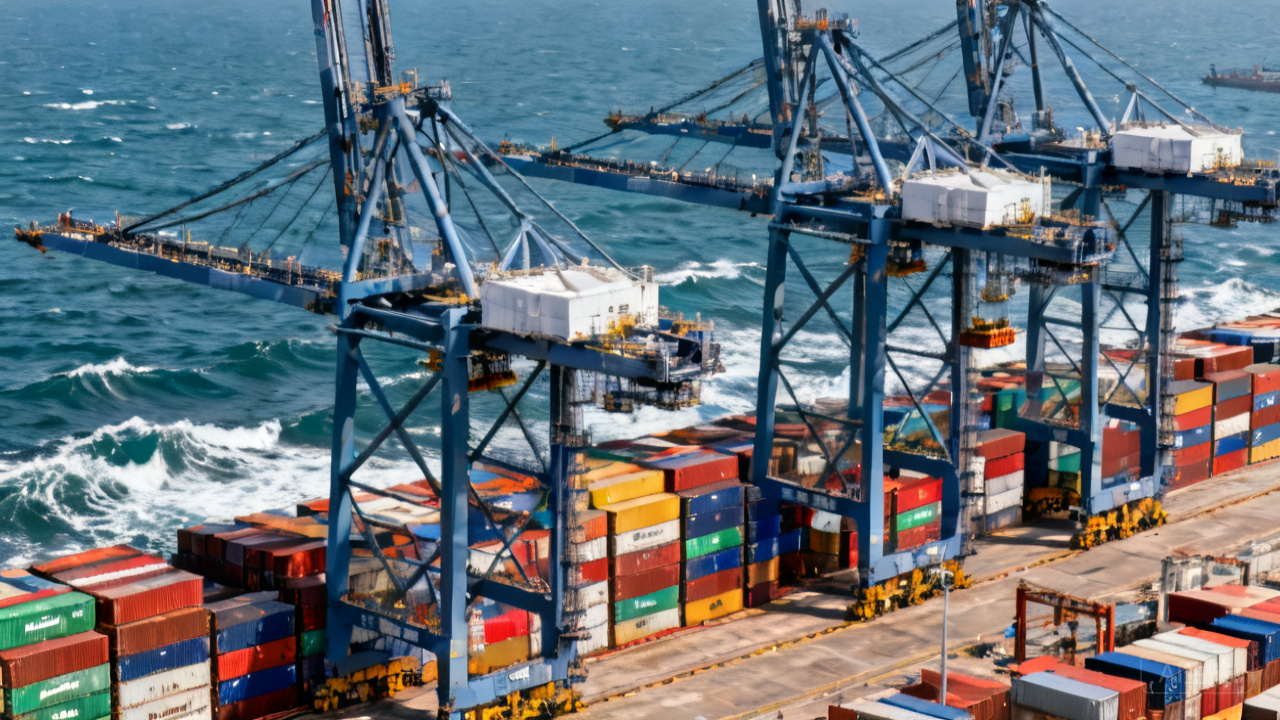
跨海大桥

海上・河川橋梁

鋼箱桁、橋塔、アーチリブ

海上石油平台

海上石油プラットフォーム

ジャケット、デッキ、居住モジュール

石化储罐

石油化学タンク外壁

原油・精製油・化学品タンク

输电铁塔

送電鉄塔・鋼管塔

高圧・特別高圧送電線の鋼構造物

钢结构厂房

大型鉄骨構造工場

産業プラント・スポーツ施設

港口机械

港湾機械

ガントリークレーン、門型クレーン、船用アンローダー

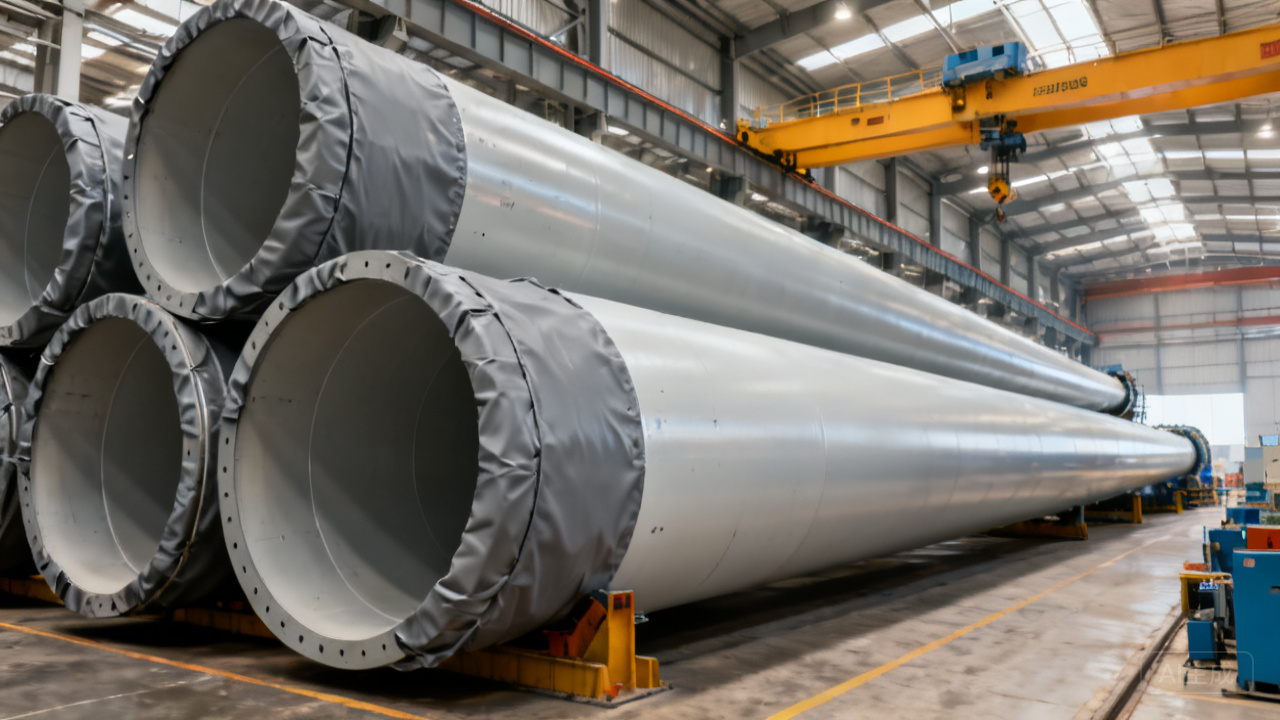
风电塔筒

風車タワー

陸上・洋上風力タワー

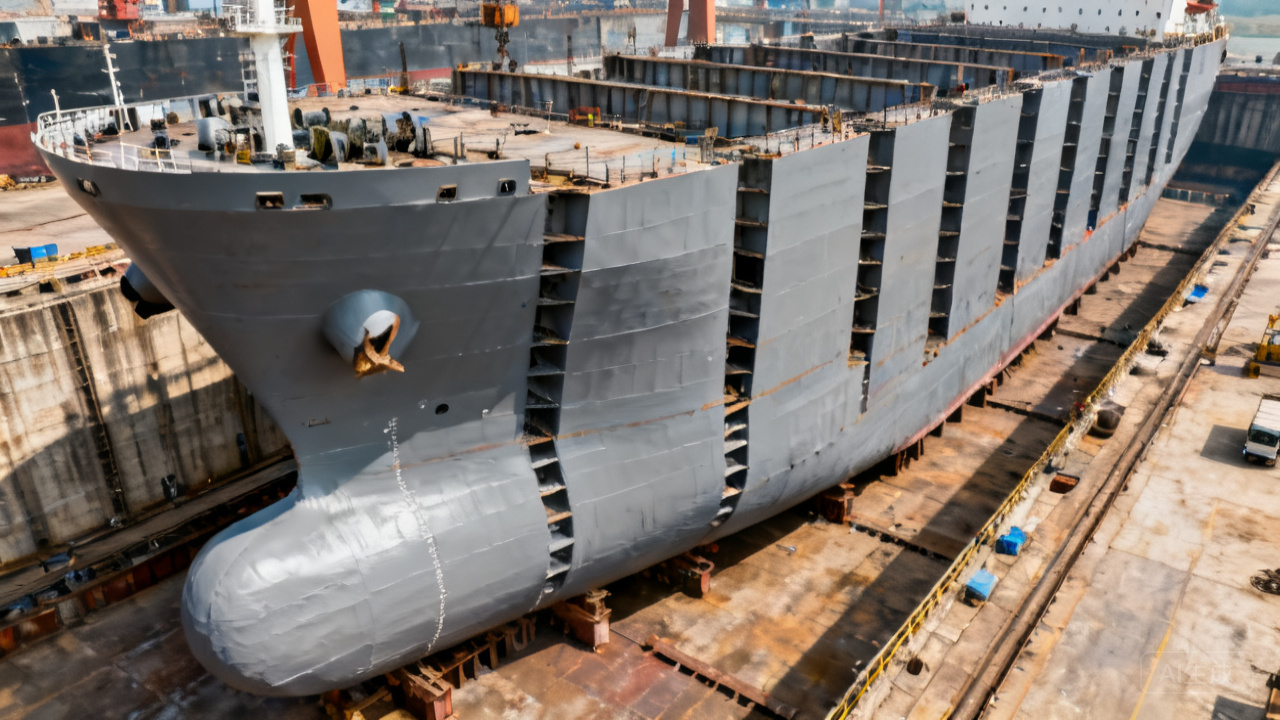
船舶与海洋工程

造船・海洋工学

船体ブロック、バラストタンク、デッキ

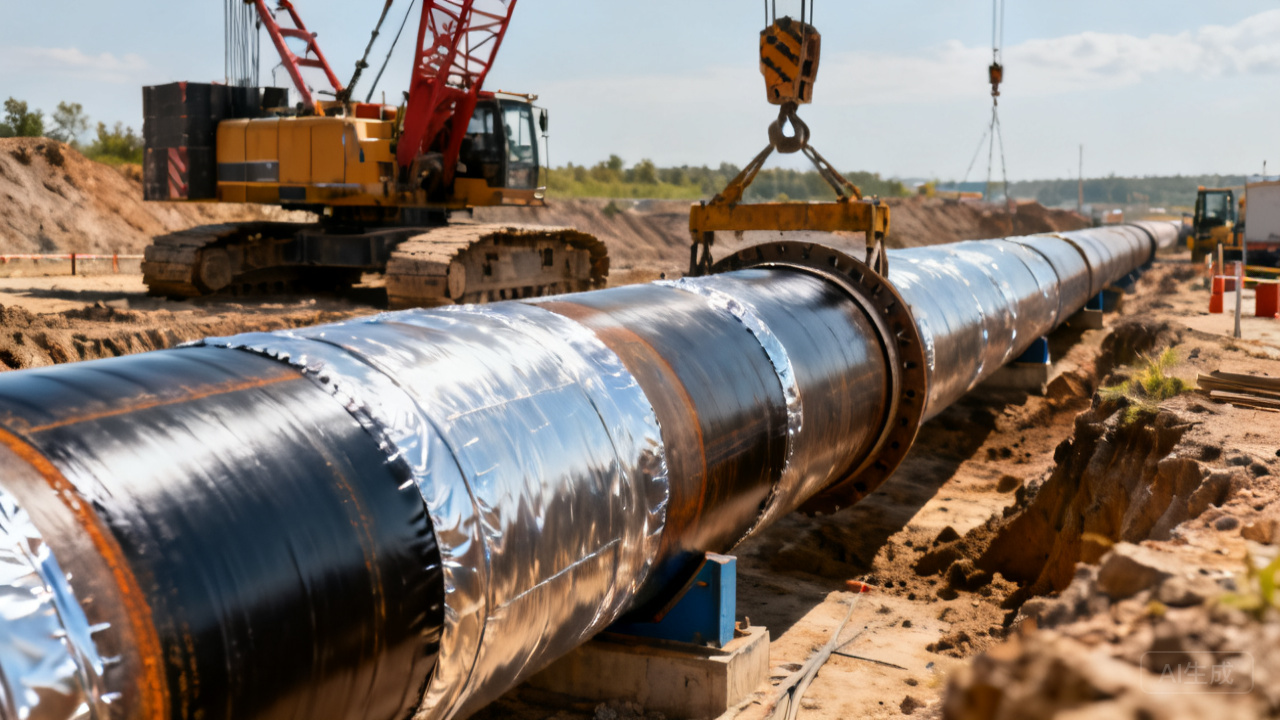
管道防腐

配管外面の防食

油・ガス・水の長距離パイプライン

矿山与工程机械

鉱山・建設機械

掘削機・破砕機・搬送設備

化工装置

化学・精油プラント

反応釜・熱交換器・配管ラック鉄骨

水处理设施

水処理・水利施設

下水処理場・水門・除塵スクリーン

よくある質問

The anti-corrosion mechanism of epoxy zinc-rich primer is based on the electrochemical principle of cathodic protection: the high content (≥70%) of zinc powder particles in the coating forms a conductive pathway and establishes electrical continuity with the steel substrate. Since the standard electrode potential of zinc (-0.76V) is more negative than that of iron (-0.44V), zinc preferentially oxidizes when corrosion occurs: Zn → Zn²⁺ + 2e⁻. The released electrons flow through the conductive network to the steel surface, causing cathodic polarization—when the potential drops below -0.85V (vs Cu/CuSO₄), effective protection is achieved. If the zinc powder content is insufficient (<60%),亜鉛粉颗粒被エポキシ樹脂绝缘包裹无法形成连续导电通路——陰極保護失效——Coating仅剩物理屏蔽功能,Anticorrosive寿命大幅缩短。这就是HG/T 3668規格严格要求亜鉛粉含有量的原因:第1类≥80%(高Anticorrosive),第2类≥70%(規格重Anticorrosive),第3類≥60%(一般Anticorrosive)。
単独では使用できません。Three reasons: (1) Epoxy zinc-rich primer single-layer exposure to acidic (acid rain pH<5.6)或碱性(コンクリート渗出碱液)Environment中,亜鉛粉会被Quick化学消耗(反应速率较中性Environment快3-10倍),丧失陰極保護能力。エポキシ雲鉄中塗り塗料(MIO板状充填剤层叠排列形成"迷路効果(迂回路効果)")Provides物理屏蔽层——保護亜鉛粉不过早消耗。(2)エポキシ樹脂含芳香醚键——紫外光(290-400nm)照射下3-6か月即开始光氧化降解——粉化/变色/失光。ポリウレタン/フッ素上塗り(含UV吸收剂和HALS光稳定剂)Provides耐候保護。(3)推奨塗装システム总DFT更厚(≥280μm)——Anticorrosive等级更高。ISO 12944-5推荐的重Anticorrosive適合する:エポキシジンクリッチプライマー60-80μm + エポキシ雲鉄中塗り塗料100-150μm + ポリウレタン上塗り50-80μm×2。
According to HG/T 3668-2020, three types of zinc content are selected: Type 1 (≥80%) — suitable for C5/CX extremely corrosive environments (offshore splash zones, tidal zones, chemical plant acid mist areas) or major projects with a design life >25 years. It offers the highest cathodic protection efficiency, but excessive zinc powder increases internal stress and reduces flexibility (flexibility ≥3mm vs. Type 2's ≥2mm), and has the highest unit price. Type 2 (≥70%) — a general heavy-duty anti-corrosion primer suitable for C4-C5 environments (coastal industrial areas, sea-crossing bridges, petrochemical storage tanks), offering the best cost-performance ratio — an optimal balance between anti-corrosion performance and mechanical properties. Recommended for most industrial projects. Type 3 (≥60%) — suitable for C3-C4 environments (urban atmosphere, ordinary industrial plants) with general anti-corrosion requirements. Can be selected if the budget is limited and the environmental corrosion level is low. Selection suggestion: When in doubt, choose Type 2 (70%) — the safest universal option.
Zinc powder has a high density (7.14 g/cm³) and tends to settle easily in low-viscosity epoxy resin solutions. Solutions: (1) After opening the container, thoroughly stir with an electric/pneumatic stirrer for ≥5 minutes—completely lift the zinc powder from the bottom until no sediment remains. (2) After adding the hardener, continue stirring for 3-5 minutes until the mixture has a uniform color. (3) Maintain continuous low-speed stirring throughout the application process—a pressure tank with a pneumatic stirrer (rotation speed 30-60 rpm) is recommended to prevent zinc powder from re-settling during spraying, which could cause inconsistent zinc content between the initial and final spray. (4) Paint that has settled and hardened into lumps—do not forcibly stir for use (the zinc powder has separated from the resin and may form lumps, leading to pinholes, uneven zinc distribution, and reduced adhesion after spraying). Paint that has exceeded its mixed pot life and shows gelation—must be discarded. It is recommended to prepare the paint as needed (estimate usage within 2 hours), in small, multiple batches.
Epoxy zinc-rich primer coating exposed to air—surface zinc powder reacts with CO₂ and H₂O to form basic zinc carbonate ("white rust"). After more than 7 days (23°C, 50% RH), the following treatments are required: (1) Visual inspection—white powdery zinc salts must be removed by sweep blasting. Use low-pressure (0.2-0.3 MPa) non-metallic abrasives (garnet/aluminum oxide) for sweep blasting—remove the zinc salt layer and create a 20-30 μm roughness. (2) For coatings within 6 months with no visible zinc salts on the surface—light abrading (manual sanding with 180-240 grit sandpaper) is sufficient. (3) If the coating has extensive chalking/corrosion/peeling—complete abrasive blasting removal and recoating are required. Preventive measures: Apply intermediate paint as close as possible within the minimum recoat interval (8-24 h)—at this stage, the primer surface still has active groups (incompletely crosslinked amine groups), achieving optimal intercoat adhesion without abrading.
核心的な違い:成膜物が異なる。Epoxy zinc-rich — organic epoxy resin + polyamide curing agent; inorganic zinc-rich — inorganic ethyl silicate/lithium silicate hydrolysis condensation. Selection comparison: (1) Anti-corrosion performance: Inorganic zinc-rich primer (zinc content ≥85%) offers higher cathodic protection efficiency, certified under NORSOK M-501 and SSPC Paint 20 Type I (inorganic) — Type II (organic). Both can achieve equivalent anti-corrosion grades, but inorganic is slightly superior. (2) Application tolerance: Epoxy zinc-rich >> inorganic zinc-rich. Epoxy can be applied at 5–40°C/RH<85%宽条件Application;无机对RH要求苛刻——RH需50-90%(ケイ酸エチル水解需要水分),低温(<5°C)和低湿(<40%)均无法正常硬化——施工ウィンドウ窄。(3)层间付着性:エポキシ亜鉛富装+エポキシ雲鉄中塗り塗料的层间结合力(>5 MPa) is superior to inorganic zinc-rich + epoxy intermediate paint (possibly due to the porous nature of the inorganic coating increasing the contact area, but also potentially leading to insufficient adhesion due to surface chalking—requiring sweep blasting). (4) Cost: Epoxy zinc-rich is approximately 0.7–0.8 times the cost of inorganic zinc-rich. Selection recommendations: For conventional heavy-duty anti-corrosion projects, choose epoxy zinc-rich (easy application + high cost-effectiveness); for extreme marine environments (splash zone/tidal zone) or top-tier projects with a design life of ≥30 years—choose inorganic zinc-rich + sealer + epoxy intermediate coat + polysiloxane topcoat.

工事事例

明石海峡大桥
Japan · 1998

日本・明石海峡大橋の鋼箱桁防食

顧客本州四国連絡橋公団(HSBA)
下地橋梁鋼箱桁、Sa3級(ホワイトメタル)
Systemエポキシジンクプライマー80μm+エポキシマイカ鉄中間塗料150μm+フッ素樹脂上塗り塗料80μm
設計耐用年数100年(C5-M 極高海洋腐食)
Area約200,000 m²
仕様本四公団塗装基準+ISO 12944-5
北海石油平台
North Sea · 2015

北海海洋石油プラットフォームジャケットの重防食

顧客Equinor ASA(ノルウェー国営石油)
下地ジャケット鋼構造物、Sa2.5級
Systemエポキシジンクリッチプライマー+エポキシマイカ状酸化鉄中塗り+ポリシロキサン上塗り
CertificationNORSOK M-501:2022 システム 1
Area約50,000平方メートル
設計耐用年数30年(C5-M 飛沫帯)
清奈港岸桥

インド・チェンナイ港のZPMCコンテナ岸壁クレーン防食

顧客PSA Chennai / ZPMC
下地岸壁クレーン鋼構造物、Sa2.5級
System水性エポキシジンクリッチプライマー+エポキシミドルコート+アクリルトップコート
規格ISO 12944 C5、1500h QUV 合格
Area約80,000平方メートル
設計耐用年数
海上风电场

中国南海洋上風力発電所のタワー防食

顧客中国三峡新エネルギー
下地風力タワー鋼管、Sa2.5級
Systemエポキシジンクプライマー70μm+エポキシマイカ鉄150μm+ポリウレタン上塗り
規格ISO 12944-5 C5-M
Area約30,000 m²(6MWタービン50基)
設計耐用年数25年(C5-M 海洋)

エポキシ富亜鉛プライマー·工場直販

無料サンプルテスト・カスタマイズされた技術ソリューション・現場での施工指導・ISO 9001認証工場・48時間以内の迅速対応

無料サンプルテスト
技術ソリューションのカスタマイズ
48時間以内の迅速出荷
ISO 9001認証

関連記事とニュース

関連記事:Kexin新素材の技術記事と業界動向