Contaminant etching of the automotive clearcoat (field slang: "etch marks" or "etching rings") is the failure process in which deposits such as bird droppings, tree sap, insect remains, pollen, diesel and brake-fluid / gasoline spills, and acid rain lose water under direct sun, rise in concentration, heat up together with the acrylic / polyurethane clearcoat, and cycle through local swelling, recrystallization and drying shrinkage, locking permanent depressions and ring-shaped marks inside the film. Its defining feature is that the defect sits inside the film rather than on top of it: washing cannot remove it, mild cases are leveled out by machine polishing, and severe cases can only be handled by reapplying the clearcoat.
Every spring and autumn the body and paint shop gets the same kind of dispute: a car parked under a tree for three days comes back with the hood covered in circular haze marks, and the polisher gets more nervous the more he buffs — some of those marks are mineral deposits floating on the surface, others have already bitten into the clearcoat as micro-pits. At hand-over nobody can say whether the fault lies with the paint, the environment or the application. Breaking this down takes only two questions: what chemical system is the contaminant, and how far has the clearcoat crosslinking actually gone. This article follows the chain "attack path — resistant formulation — test and acceptance — liability assignment" and pins the formulation side and the testing side onto the same table.
TL;DR: the conclusions first
- Etching is an in-film defect; water spotting is an on-film deposit. The terminology section of ASTM D7356/D7356M splits "acid rain spots" explicitly into mineral deposits (the white calcium salts left when water dries, which a decontamination clay bar can pull off) and acid-etch spots (depressions in the paint or clearcoat that will not come off). A field screen is enough for a first call: mist with distilled water, then wipe dry. Marks that fade when wet and reappear when dry are mineral; marks that stay recessed are etching.
- The time scales come from different sources. Public industry figures: bird droppings can leave marks within 24–48 h under full sun; pine-sap type tree gum shows permanent etch marks after 3–7 d and starts bonding to the clearcoat at about 48 h; whereas a pure water bead on a hot plate can leave a mineral spot within minutes of drying. "Minutes" and "two or three days" describe two different mechanisms and must not be advertised as one.
- "Bird droppings equal uric acid burning the paint" is a simplified narrative. The XRD re-evaluation published in Journal of Ornithology in 2019 (6 bird excreta species; Dryad dataset DOI 10.5061/dryad.d39b44r) found the crystalline phases to be mainly ammonium urate and struvite (magnesium ammonium phosphate), not uric acid crystals themselves. The real attack is the combination of "salt slurry concentration + co-heating swelling + dry shrinkage stress", not one strong acid.
- The hard defense on the clearcoat side is crosslink density and film density, not contact angle. A 2K hydroxy acrylic / HDI trimer system (isocyanurate ring, nominally trifunctional) forms a covalent network in the NCO/OH molar ratio range 1.0–1.5 that swells but no longer redissolves; a 1K thermoplastic clearcoat can be redissolved and softened repeatedly by fuel and brake fluid. A high contact angle only shrinks the wetted area — small contaminant molecules still permeate along the free volume.
- Testing has a published method family to follow. Droplet spot testing: ASTM D1308 (current D1308-20, reapproved 2025; 1 mL dropped under a cover glass, usual observation intervals 15 min, 1 h, 16 h) and GB/T 9274-1988 method C (about 0.1 mL per drop). Fuel immersion: ISO 2812-1:2017 (the test liquid family includes EN 590 diesel, EN 228 gasoline and DIN 51604 FAM test fluid). For the "xenon arc + simulated acid rain spray" coupled aging test, ASTM D7356 is a ready-made reference method.
- Acceptance has to state the "condition trio". A chemical test must bind "reagent + temperature × time + rating direction". D1308 §9.1 says outright that the method gives non-quantitative results and that numeric grading relies on a user-defined scale — the industry runs both 0–10 (10 = no change) and 0–5 (0 = no change) directions at the same time, and data without a stated direction are not comparable.
1. Etch marks, water spots and gloss loss: three kinds of paint marks, three different fates
"There are marks on the paint" covers three common situations, and separating them is the starting point of every judgment call. The ASTM D7356 definitions have already split acid rain spots into two classes; add whole-panel weathering and you get three genuinely different failure paths.
1.1 Etch marks: the four-step cycle of concentration — swelling — recrystallization — shrinkage
Most contaminant deposits are water-bearing semi-solid slurries. Under sun the first move is concentration: water evaporates from the edge toward the center, and the local concentration of ammonium salts, urates and organic acids rises several-fold. Then comes co-heating swelling: rising panel temperature increases the free volume of the clearcoat, small molecules and ions diffuse into the film, and the contact zone softens and expands. Then recrystallization and shrinkage: once the slurry has dried through it shells over, the shrinking volume applies uneven tensile stress to the already softened surface, and salt crystals prop open micro-cracks on a microscopic scale. If the clearcoat is under-cured, or the spot is put through repeated "wet — dry" cycles, the micro-pits and rings get locked into the clearcoat as the "depressions, not readily removable" acid-etch spots of the D7356 terminology. Polishing only levels shallow pits: the deeper the pit, the faster the remaining clearcoat reserve is consumed.
1.2 Water spotting: minerals relocating, not chemistry biting in
Tap water and rainwater carry calcium and magnesium bicarbonates and sulfates. On hot panels a bead evaporates within minutes and the solids precipitate as an "edge ring". That is a mineral mark deposited on the surface and partly pressed into the softened outer layer; wiping it with a dilute acid around pH 5 (for example diluted white vinegar — the ASTM D1308 reagent list itself includes 3 % acetic acid) or with a chelating cleaner visibly reduces it. But the two defect types often coexist: a mineral shell covering an acidic or ammonium-salt contaminant actually extends the contact time between slurry and paint, and step by step turns a "mineral mark" into real etching.
1.3 Gloss loss and chalking: whole-film UV aging, not a point attack
When a whole panel hazes and whitens evenly and leaves powder on the hand, you are looking at the gloss loss and chalking process caused by photo-oxidative chain scission in the resin and pigment exposure; rating follows the aging rating system of GB/T 1766. The mechanism and the weatherable formulation are covered in our published articles Clearcoat gloss loss and yellowing: causes and prevention and Automotive paint aging and fading: causes and restoration. The boundary with etching is simple: etching is point-shaped, has a contour, and matches the position of the contamination source; gloss loss is area-shaped and contourless. Polishing gloss loss as if it were etching, or filing a warranty claim for etching as if it were gloss loss, are both common liability-assignment errors.
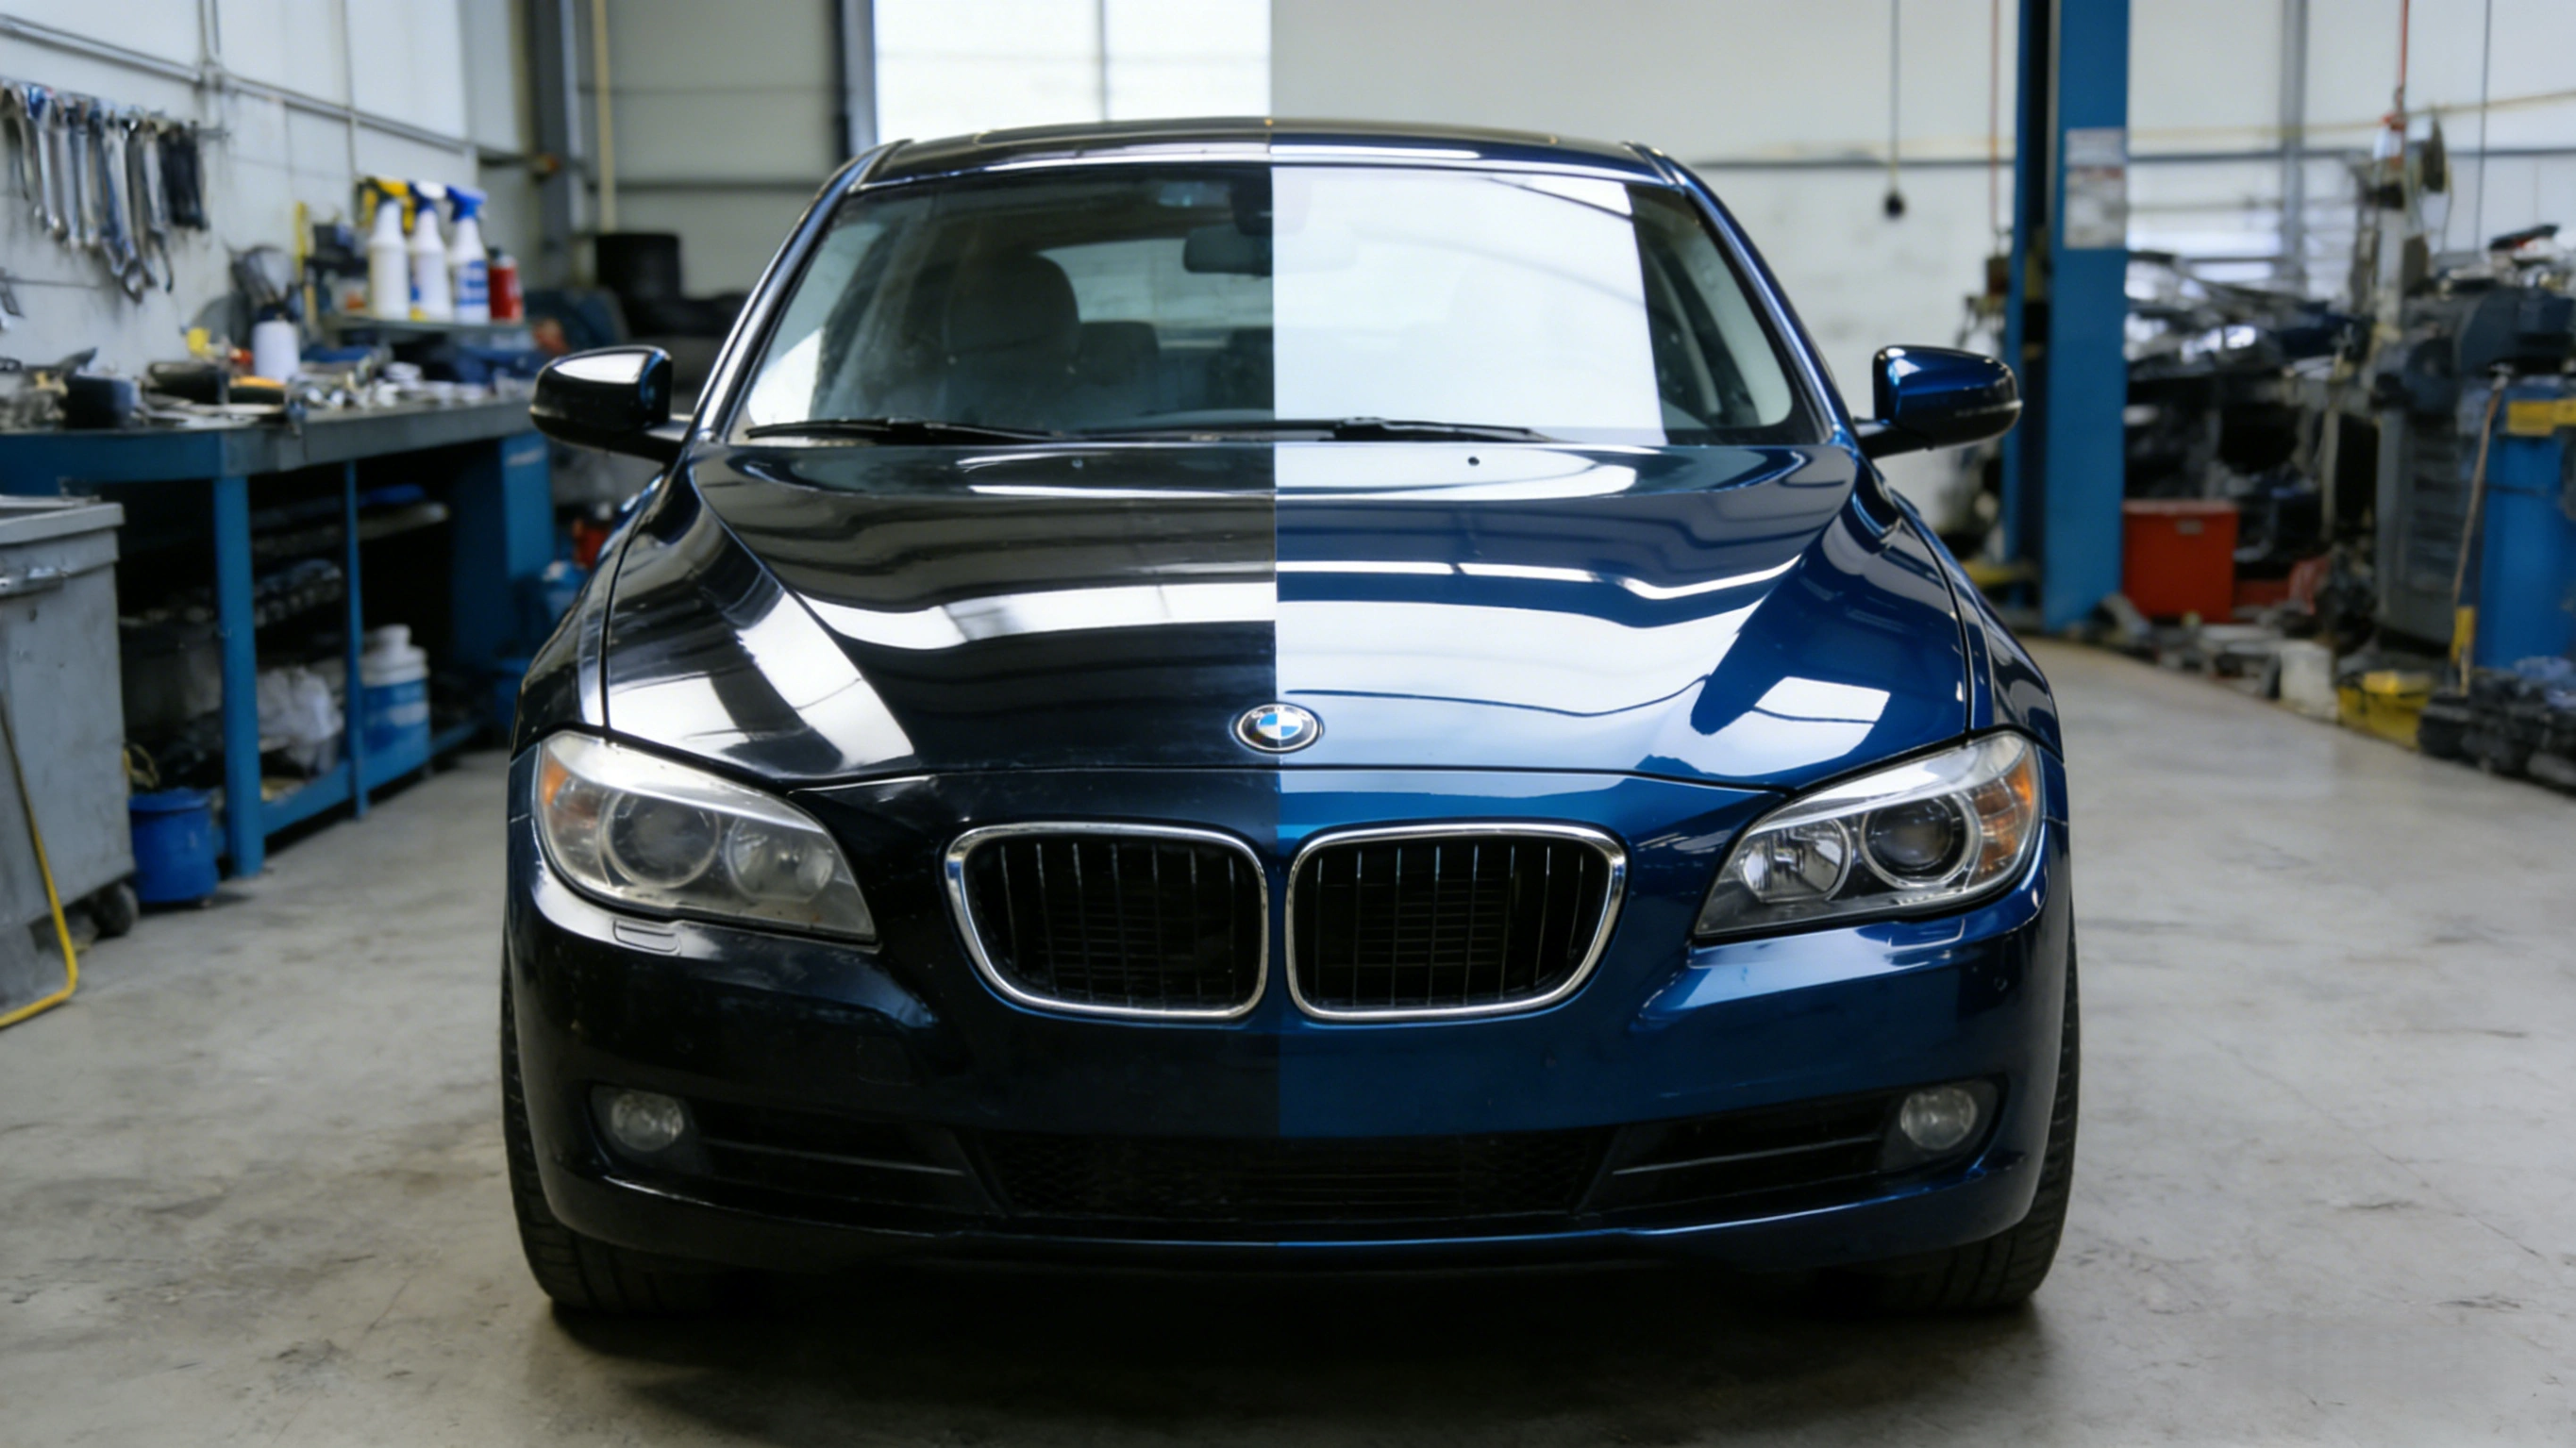
2. Five classes of contaminant: chemical nature and attack path
The stock phrase in "protection" discussions is that "it is all acid". Against the sources that can actually be checked, that generalization does not hold: the active components, the acidity or alkalinity, and even the time scale of attack differ from contaminant to contaminant, and so do the matching formulation and maintenance strategies.
| Contaminant | Main active components (checkable source) | Acidity / alkalinity basis | Behaviour under sun exposure | Marking time per public figures |
|---|---|---|---|---|
| Bird droppings | Crystalline phase of the nitrogen excreta dominated by ammonium urate and struvite (magnesium ammonium phosphate) (2019 Journal of Ornithology XRD re-evaluation, 6 species; uric acid itself pKa1≈5.4, pKa2≈10.3, solubility in water at 20 °C about 6 mg/100 mL) | Vendors commonly quote "pH 3–4.5", which coexists with the XRD result but has no third-party unified calibration; ammonium-salt hydrolysis is locally weakly alkaline, so the concentrated salt slurry attacks on two fronts | Slurry evaporates and concentrates — shells and shrinks — salt crystals prop open micro-cracks | Marks possible within 24–48 h under full sun (car-detailing industry figures) |
| Tree sap / honeydew | Polysaccharides and sugars, terpenic resins, mixed organic acids; aphid honeydew is likewise a high-sugar film | Acidic (qualitative; no unified pH found in public sources) | Light and heat accelerate polymerization and hardening; drying shrinkage pulls at the clearcoat surface; the sugar film traps dust and insects | Pine-sap types show etch marks after 3–7 d in full sun; bonding starts at about 48 h (industry figures) |
| Insect remains | Proteinases and digestive enzymes, chitin fragments, organic acids such as formic acid (the Latin name of formic acid comes from formica, the ant) | Weakly acidic slurry (industry commonly quotes pH 4–5, uncalibrated) | Smashed and embedded by high-speed impact; heat denatures the protein and "activates" the acids and enzymes | Hours to days, faster in hot weather (industry figures) |
| Pollen | Cellulose / pectin outer wall, protein and lipid contents | Forms a mildly acidified paste once wet (qualitative) | Absorbs water into a moisture-retaining film and extends the contact time of other contaminants; soiling in its own right | Marks appearing after 1–2 weeks without washing in pollen season (industry figures) |
| Diesel / gasoline / brake-fluid spills | Hydrocarbon solvents (EN 590 diesel and EN 228 gasoline are the routine test liquids on the ISO 2812-1 relayed basis, plus DIN 51604 FAM test fluid); DOT3/4/5.1 brake fluids are glycol-ether plus borate-ester based and strongly hygroscopic | Near neutral — swelling / solvent attack rather than acid-base attack | Penetrates the clearcoat and re-swells it; 1K films can be redissolved; brake fluid left in place causes whitening and cracking | Fuel and brake fluid must be "rinsed off immediately" (consistent industry figure) |
| Acid rain | Sulfuric and nitric acids formed from SO2/NOx; clean rain equilibrates with CO2 at pH≈5.6, and rainfall below 5.6 is defined as acid rain (US EPA basis) | pH commonly below 5.6, lower still in industrial areas | Droplets evaporate and concentrate into spot-shaped acidic residues (chiefly sulfuric and nitric acids); D7356 reproduces this in the laboratory with xenon arc plus simulated acid rain spray | 12.7 mm (0.5 in) scale spots take one full season of outdoor exposure (Jacksonville outdoor basis) |
2.1 Bird droppings: correcting the "strong acid narrative" into the "salt slurry narrative"
For vehicle makers and refinishing shops the pH dispute does not actually change the scrap decision: whether it is uric acid or ammonium urate / struvite, the behavior of the slurry under sun is concentration — shelling — shrinkage, with raised local chemical potential and mechanical tensile stress acting together. The steadier engineering statement is that the damaging power of bird droppings comes from the combination of "time × temperature × degree of cure", not from any single pH number.
2.2 Tree sap: swelling first, then a hard shell that pulls back
What makes sap special is that it turns into a solid by itself. After the water evaporates, the resinous components polymerize and harden and the whole mass shrinks, applying shrinkage stress to an outer layer that the organic acids have already swollen — the microscopic version of what owners describe as "peeling the sap took the paint with it". Honeydew and sap frequently appear together, because they share the sugar — acid — heat trio.
2.3 Insect remains and pollen: the protein / enzyme route
A considerable share of the attack components in insect remains are proteins and enzymes — the industry calls it "protein etching". That explains a familiar field observation: the dried carcass shell can itself be softened with water, but before it softens it has already delivered its acids and enzymes into a clearcoat that is softening. Pollen follows a similar but milder path: it mainly contributes water retention, a mildly acidic paste layer and dust adhesion. It is an amplifier, not the principal offender.
2.4 Fuel and brake fluid: swelling attack, with a completely different liability chain
Gasoline is the "reverse solvent" of a clearcoat: on 1K thermoplastic films it can cause redissolution (tack, gloss loss, wrinkling); on 2K crosslinked films it causes swelling and plasticization. Diesel evaporates slowly and acts for longer. The glycol-ether fraction of brake fluid spreads readily and is hygroscopic, and the industry consensus is "if it spills, flush with plenty of clean water at once — overnight and it may already whiten and shell". This class is not an environmental deposition problem but a use and maintenance problem, and in intake and liability decisions it should be registered separately from bird droppings and tree sap.
3. Temperature × time: "minutes" and "two or three days" on a hot plate are not the same thing
Why do deposits mark hot panels so much faster? First pin down a few checkable temperature facts:
- Panel-temperature design basis: SAE J1455-1994 (recommended practice for automotive environmental extremes of electrical / electronic equipment) gives a design maximum surface temperature of 115 °C for instrument panels and windshields in direct sun, with an ambient design maximum of 85 °C — engineering standards assume by default that a sun-soaked vehicle surface is far above the human touch threshold.
- In-cabin measurements: the 2005 study from Stanford University School of Medicine (McLaren et al., published in Pediatrics) measured that on clear days with an ambient temperature of 72–96 °F (about 22–36 °C) the cabin air of a parked vehicle rose by roughly 22 °C on average within 1 h; the Arizona State University team's 2018 field measurements in the journal Temperature (Vanos et al.) showed that after 1 h parked in clear 35 °C weather the instrument panel averaged 69 °C.
- Exterior paint surface basis: several public measurement accounts show dark panels reaching 75–80 °C in direct sun at 30 °C ambient, and light panels about 50–55 °C (media and industry thermometer figures, not standard data).
At these temperatures three things happen at once. On the contaminant side, water evaporates faster, the slurry's concentration and viscosity rise, and shelling and shrinkage accelerate. On the film side, free volume increases and the diffusion coefficients of small molecules and ions climb with temperature in an Arrhenius-like way (each step up in temperature shortens the permeation time scale several-fold — the exact multiplier depends on the resin system, and public data are not sufficient for a universal constant, so only the direction is given here). On the substrate side, steel and aluminium conduct heat quickly, so film and substrate heat up together; there is no protective layer in which "only the top 40 μm of surface is heated". Hence: a pure water bead dries in minutes and leaves a mineral water spot (the deposition route); a bird-dropping slurry starts swelling on an hourly scale and leaves locked-in micro-pits on a 24–48 h scale (industry figures, the etching route); and a freshly sprayed clearcoat that has not fully crosslinked drops its resistance floor by another notch — which is precisely the mechanism behind "new car brought home and parked under a tree overnight, haze marks by morning". In engineering communication, keep the time — temperature dose together: talking about exposure duration without panel temperature, or about contamination resistance without degree of cure, does not constitute a criterion.
4. What the clearcoat formulation can do: crosslink density and film density are what count
| Technical route | Film-forming / crosslinking chemistry | Checkable parameter anchors | Etch-resistance behavior | Main price paid |
|---|---|---|---|---|
| 1K thermoplastic acrylic clearcoat | Solvent-evaporation physical drying, linear macromolecules | No measurable degree of crosslinking; redissolvable by its own solvent class | Fuel, brake fluid and strong solvents redissolve and soften it; contaminants pass through easily | Low cost and easy to recoat, but etch resistance is inherently limited |
| 2K hydroxy acrylic + HDI trimer | Urethane covalent network; isocyanurate ring nominally trifunctional | NCO/OH molar ratio commonly 1.0–1.5; aliphatic systems do not yellow; water-crosslinkable variants are covered in our 2K clearcoat article | Swells but no longer redissolves; the more complete the crosslinking, the fewer diffusion channels | Short pot life (waterborne types 4–8 h at 20 °C); excess NCO meeting moisture generates CO2 and pinholes |
| Polysiloxane / polyether-modified surface layer | Low-surface-energy components migrate and enrich at the surface | ASTM D7490 measures surface tension in roughly the 20–60 dyn/cm range | Easy to clean; water beads carry particles away | Contact angle decays with abrasion and UV aging; it is not anti-permeation |
| Nano Al2O3 / SiO2 and polysilazane coatings | Ceramic phase; Si-N hydrolysis-condensation into Si-O-Si | Room-temperature moisture cure to pencil 5H (24–72 h), single layer 0.2–10 μm; RT-cured hardness about 3 GPa, ceramization at 700–1000 °C near 13 GPa — a paint bake oven never gets there, so "9H" is a pencil scale, not an abrasion scale | A dense inorganic layer blocks ionic channels effectively | Thin and scratch-sensitive; demanding application environment and humidity window |
| Heat-activated self-healing clearcoat | Shape-memory / dynamic-bond elastomer top layer | Activation temperature per industry figures 40–50 °C (reachable by sunlight or hot water); Nissan Scratch Shield in series production since 2005 | Effective only on indentations and hairline marks that have not bitten through the clearcoat | Crosslink density is lowered to enable healing, so chemical and etch tolerance drop (soft top layer accelerating aging is an industry observation) |
4.1 Crosslink density is the primary variable: the 1K / 2K watershed
The physical essence of etching is that molecules and ions diffuse into the film and are retained there. In a linear thermoplastic film, solvents and salt solutions can let the macromolecular chains loosen again (redissolution). A covalently crosslinked network can only swell to a given equilibrium; its diffusion coefficients are an order of magnitude lower, and the film springs back once the contaminant is removed. That is why OEM exterior clearcoats are 2K / bake systems, and why the refinishing side insists on "crosslinked through before delivery". The full film-formation derivation is in How automotive paint films form: physical drying and chemical curing, and the HDI hardener, mix ratio and film-build process details in 2K polyurethane clearcoat technology: HDI hardener, mix ratio, film build and VOC.
4.2 NCO/OH index, acid value and residual hydroxyl: three paired variables
Public technical literature commonly puts the 2K NCO/OH molar ratio at 1.0–1.5. As the index approaches 1.0 the network is economical and residual —NCO is low; deliberate excess (1.2–1.5) raises crosslink density and hardness, but in humid conditions excess —NCO hydrolyzes to urea and CO2, bringing pinholes and long-term hydrolysis sites. The hydroxyl-value side works the same way: a high acid value / high hydroxyl resin improves adhesion and crosslink-point density, but carboxyl groups are hydrophilic, and the higher water uptake makes it easier for the contaminant water slurry to linger at the interface. Formulation trade-offs must be tied to the application: where etch resistance is the goal, completeness of crosslinking and low hydrophilic residues come before apparent hardness.
4.3 "Anti-soiling is not anti-etching": contact angle is a cleanability metric, not a barrier metric
Polysiloxane and polyether modification push the surface energy down (the ASTM D7490 measurement range is 20–60 dyn/cm, and that standard itself states it "is not a quality-control or specification test"), with the effect that water beads roll off, less dust sticks and contaminants do not spread. But a high-contact-angle droplet of bird-dropping slurry still sits in contact with the paint and heats with it: a small wetted area does not mean little permeation — swelling and ionic diffusion happen in the film body directly beneath the contact point. High contact angle takes care of "sticks less"; crosslinking and film density take care of "does not penetrate"; the two metric systems cannot corroborate each other. For the same reason, a hydrophobic layer is consumed by car washing, ultraviolet light and friction, and the contact-angle decay interval belongs in the maintenance plan rather than on the acceptance sheet.
4.4 Coatings and self-healing: effective, but recognize the boundaries
Aftermarket "glass / ceramic coatings" use polysilazane or SiO2 sol to build another 0.2–10 μm dense inorganic layer on top of the clearcoat; in essence they add a sacrificial outer shield. "9H" is a pencil hardness scale with no conversion relationship to etch resistance — reader-oriented explainers are in 9H nano ceramic paint coating technology explained and Nano polysilazane ultra-hard automotive coating. Self-healing top layers (the Nissan Scratch Shield route and its TPU film versions) eliminate shallow indentations by heat-activated rebound, at the usual price of a softer top layer with lower crosslink density — chemical tolerance and etch resistance fall with it, and the accelerated aging of "instant self-healing" top layers at 12–18 months is an industry observation; how to trade the two off is covered in Matte / satin self-healing nano automotive topcoat. The companion criteria in the abrasion and scratch direction are in Automotive clearcoat scratch resistance: formulation logic from friction coefficient to critical load.
5. Testing and acceptance: the published method family, coupled tests and correlation
| Method | Scope and media | Test conditions as publicly relayed | Reading basis |
|---|---|---|---|
| ASTM D1308 (current D1308-20, reapproved 2025; first issued 1954) | Effect of household chemicals on clear and pigmented coating systems: 3 % acetic acid, 50 % (volume) ethanol, detergents, lighter fluid, grease and other items on a user-defined list | Cover-glass spot method: 1 mL from a 5 mL pipette, watch glass applied immediately; the open-spot method applies the drop directly; usual observation intervals 15 min, 1 h, 16 h; test environment 23±2 °C / 50±5 % RH; panels aged about 1 week at 25 °C / 50 % RH after preparation | §9.1 states that results are non-quantitative and that numeric grading relies on a user-defined scale; the industry 0–10 and 0–5 directions both exist and the report must state the direction (common wording: 10 = no change, 0 = complete breakdown) |
| GB/T 9274-1988 "Paints and varnishes — Determination of resistance to liquid media" | Three methods — immersion / absorbent media / spotting (A / B / C); adopts the ISO 2812:1974 framework equivalently | Method C (spotting): about 0.1 mL per drop, drop spacing not less than 20 mm and not less than 12 mm from the edge, exposed at (23±2) °C for the specified time; method B absorbent pad (about Ø25 mm, 1.25 mm thick) covered with a watch glass (about Ø40 mm), test period not exceeding 7 d; panel conditioning generally not less than 16 h (23±2 °C / 50±5 % RH) | Gloss loss, discoloration, blistering and peeling graded per GB/T 1766; the pass is judged on not fewer than two panels meeting the product specification |
| ISO 2812-1:2017 (3rd edition) | Immersion in liquids other than water; automotive-context liquids: EN 590 diesel, EN 228 gasoline, DIN 51604 FAM test fluid, 10 % hydrochloric acid, 5 % sodium hydroxide | ISO 1514 standard panels 150 mm × 100 mm × (0.7–1.0) mm or Ø15 mm steel rods; conditioning at 23±2 °C / 50±5 % RH for not less than 16 h; film thickness per ISO 2808; re-inspection 24 h after the test | Blistering rated per ISO 4628-2; the report binds the liquid, temperature and duration trio |
| ISO 2812-2:2007 (2nd edition, 2007-01-15) | Immersion in water (long-term water / condensate contact scenarios) | Same panel preparation and conditioning requirements as Part 1 | Used to establish the hydration / blistering baseline for the contaminant water slurry |
| GB/T 1865-2009 (IDT ISO 11341:2004; issued 2009-06-02, effective 2010-02-01) | Filtered xenon-arc artificial climate aging plus artificial radiation exposure | Publicly relayed figures: chamber air temperature 38±3 °C, black standard temperature BST 65±2 °C; cycle A spray 18 min + drying 102 min; spray-water conductivity not more than 2 μS/cm; exposure dose metered by radiant energy at 340 nm | Aging rated per the GB/T 1766, GB/T 9754 (60° gloss) and GB/T 11186 (color difference) series |
| ASTM D7356/D7356M (current 2025 edition; preceded by -13 and -19) | The dedicated method for accelerated acid-etch weathering of automotive clearcoats: xenon arc (per Practice G155, daylight filter) plus simulated acid rain solution spray, with specimens laid flat so the liquid film stays on the surface | The method states that it reproduces the etching defects of outdoor acid-rain exposure in Jacksonville, Florida from May to mid-August; defects range from small pits to 12.7 mm (0.5 in) scale spots; other acid-etch tests reproduce only pits below 6.35 mm (0.25 in); there is no ISO equivalent method | §5.1 states directly that acid-etch damage is a significant warranty-claim item for vehicle makers; Annex X1 gives side-by-side outdoor and laboratory defect images |
| ASTM D7490-13(2022) | Two-probe liquid contact angle to surface tension and its dispersive / polar components | Measurable range about 20–60 dyn/cm (dyn/cm and mN/m are numerically equal) | For characterization and failure troubleshooting; the standard's own wording is "not a quality-control / specification test" — usable only as supporting evidence |
5.1 Droplet spot methods and the rating direction: the invisible trap on the acceptance sheet
The body of D1308 does not prescribe numeric grading; it only says values may be assigned if a grading scale is used. So the market runs both the "10 = no change" and the "0 = no change" reporting habits at the same time. A test commission to a supplier has to pin down: the method clause (D1308 cover-glass spot or GB/T 9274 method C), the reagent and its concentration, temperature × time, the recovery period, and the rating direction and the target value (for example "10-point scale, 10 = no change, target not below 9"). Miss any one of these and two "passing reports" can contradict each other.
5.2 Simulated contaminants: there is no published standard fluid for bird droppings or sap — what now
The published method family contains no "standard bird-dropping reagent". The workable engineering substitute is a "fingerprint match" built from reagents that are already calibrated: compound an ammonium-salt / urate mixed slurry per the XRD conclusion for ammonium urate and struvite; on the pH side use the two levels given by the 3 % acetic acid in the D1308 list plus an alkaline solution; borrow the sugar — acid route from the qualitative organic acids of tree sap plus the D1308 open-spot method (fruit and beverages are already within the spirit of that reagent list); on the fuel side go straight to EN 590 / EN 228 / DIN 51604 FAM on the ISO 2812-1 relayed basis. The key is to place the two evidence chains — real-contaminant observation (field-exposed panels) plus chemical surrogate liquids (laboratory) — side by side in the acceptance plan, rather than claiming that some house-mixed solution "equals bird droppings".
5.3 Re-exposure after aging: the coupled-test approach
A new factory film and a film 5 years in service differ by a class in etch resistance: UV aging first creates chain scissions and micro-cracks, and contaminants then permeate along "pre-treated channels". The recommended two-stage test is to run a half-aging first per GB/T 1865-2009 xenon-arc exposure (for example 250–1 000 h, or set by radiant energy at 340 nm), then re-run ASTM D1308 / GB/T 9274 method C spot tests on the same batch of panels to assess "residual chemical resistance after aging". ASTM D7356 is itself the integrated xenon-arc plus spray coupling example: light, heat and a retained acidic liquid film are superimposed in one chamber, and its defect spectrum (including 12.7 mm scale spots) covers the large-scale etching that ordinary spot methods cannot reproduce — which is also why it was written into the automotive warranty context as a laboratory-to-Jacksonville-field correlation bridge.
5.4 Accelerated versus outdoor correlation: the honest boundary
Full-spectrum xenon (ultraviolet + visible + near infrared) correlates with natural sunlight better than single short-wave UV fluorescent routes, but all the standards agree on one point: accelerated test hours cannot be converted linearly into outdoor years, and can only be used for relative ranking and lot-to-lot consistency. What D7356 establishes against Jacksonville outdoor exposure is "similarity of defect morphology" (the Annex X1 image comparison), not an "hours to months" conversion table; whenever you meet any "X hours = Y years" claim, first ask which resin system, which region and which defect criterion it refers to. Our overview of automotive paint test standards is Automotive paint test standards: an acceptance map from GB/T to ISO; the furniture industry's stain-resistance logic belongs to the same family (Furniture coating stain and chemical resistance: test methods and formulation logic).
6. Defect attribution and liability: a checklist usable by body shops and OEMs
| Suspected defect | Field criterion | Verifiable evidence | Liability direction |
|---|---|---|---|
| Acid-etch spots (etching) | Does not disappear when wet; with a thin plastic bag over the fingertip you feel catching micro-pits; ring-shaped contours under 15–30° low-angle light | Cross-section microscopy shows depressions inside the film; D1308 reproduction; D7356 defect image comparison | Environment and exposure time dominate; the coating side shares liability where clearcoat crosslinking is insufficient |
| Mineral water spots | Fade as soon as they are misted and reappear on drying; wipe off with dilute acid or a chelating agent | Qualitative ash residue (calcium, magnesium); distilled-water control panel | Use and maintenance practice (washing a hot panel, hard-water rinse) |
| Clearcoat gloss loss / oxidation | Uniform haze over the whole panel, no contour; no pits to the touch | GB/T 9754 gloss comparison against an unexposed area; GB/T 1766 rating | Weatherability formulation and years in service; see Clearcoat gloss loss and yellowing: causes and prevention |
| Chalking | White fingerprint, short-term recovery after a wet wipe, recurrence within weeks | Gauge reading already below the clearcoat reserve floor (industry gauge figures: whole vehicle 100–180 μm, clearcoat 30–50 μm) | End of coating life; repaint — not a polishing liability |
| Application lifting (undercoat attack) | Wrinkling and cratering hours to days after a repair, area equal to the patched zone | Compatibility check between the underlying coat and the topcoat solvent; flash-off time records | Application practice (compatibility and flash-off), not environmental etching |
| Interlayer peeling / whitening (new paint) | Marks appearing after rain once delivered; fixed haze spots in bead patterns that recur | Cure-window records (60 °C / 30 min, or 16 h or more at room temperature); NCO/OH mix-ratio traceability | Exposure before cure — coating-side liability |
Two technical fulcrums carry the judgment. The first is the distilled-water test: mist, observe, wipe dry and check reproducibility, which separates "depositional" from "recessed" defects — the D7356 terminology has already drawn that physical boundary. The second is the paint film thickness gauge: industry paint-correction figures give a total factory build of 100–180 μm with a clearcoat layer of about 30–50 μm, a single polish removing about 2–5 μm, so panels averaging below about 80 μm get only light leveling. Gauging before you accept an etching claim is the same as confirming how much abrasion reserve is left, and it prevents an end-of-life panel from being misjudged as a repairable defect. Lifting and etching are told apart by the occurrence window and the pattern: lifting follows a repair closely and its outline matches the patch; etching corresponds to an exposure event and its outline matches the position of the contamination source. In cosmetic acceptance, record orange peel and distinctness of image separately from etching (Controlling the link between orange peel and distinctness of image DOI in coatings), otherwise a rework quote has nothing to stand on.

7. Engineering recommendations: actionable steps on the application side and the maintenance side
7.1 Application side (OEM and refinishing shop)
- Put a clearcoat minimum film build into the agreement: for refinishing, a 2K clearcoat dry film build of not less than 40–50 μm is recommended (the process figure of 60–80 μm wet per pass for the usual two passes), leaving polishing reserve for later etch rework; an OEM clearcoat of 30–50 μm is the common range of publicly relayed gauge figures.
- Get flash-off and cure right: for 2K systems, force dry at 60 °C / 30 min, or let the film crosslink fully at room temperature for 16 h or more before delivery and before exposure; the resistance floor of an uncured clearcoat against water and contaminants drops by another notch. The matching application window is in 2K polyurethane clearcoat technology.
- Do not spray hot panels: spraying when the panel temperature is clearly above ambient (hot to the touch after sun) raises the risk of solvent entrapment and surface defects; in summer let panels come back to temperature before they enter the booth.
- Write etch resistance into acceptance: commission D1308 / GB/T 9274 spot tests with the "condition trio" of §5.1; for in-service judgment use the two-stage plan of GB/T 1865-2009 half-aging followed by spot re-testing; in an OEM context the method logic of ASTM D7356 can be cited directly.
- Quantify the hand-over note to the customer: remove bird droppings and insect residues within 24 h and tree sap within 48 h (aligned with the industry marking-time figures), and state the "cleaning window" so that after-sales disputes do not escalate into liability arbitration.
7.2 Maintenance side (fleet and end-service figures, for B2B customers to put into manuals)
- Exposure time is the dose: during the hot high-sun season remove contaminants the same day they are found; when immediate action is impossible, cover the spot locally with a wet wipe to cool it and slow down concentration and swelling.
- Wash interval: normally once every 1–2 weeks, shortened to about 1 week in pollen season and in sap-drip areas. Choose a pH-neutral wash liquid (industry figure about 6–8) and avoid strongly alkaline automatic car-wash chemicals; do not wash while the panel is hot, since fast-drying beads leave secondary mineral marks.
- Spill emergency: for fuel or brake-fluid spills rinse immediately with plenty of clean water and keep the panel under observation for 24 h; if whitish haze spots appear, run a spot test first to judge the depth, then decide between polishing and repainting.
- Sacrificial-layer strategy: ceramic coatings and paint protection film (PPF) act as a replaceable outer shield, and contaminants still have to be removed at the intervals in the section above. After hydrophobic decay, sample-check the contact angle with D7490, but do not treat contact angle as evidence against permeation. The maintenance item list is in Automotive paint daily care: washing / waxing / glaze sealing / ceramic coating; the function of the clearcoat itself is recapped in Automotive clearcoat: what it does and the high-solids trend.
Key data: the verifiable parameters used in this article
- Panel temperature: SAE J1455-1994 design maximum of 115 °C for surfaces in direct sun and 85 °C ambient; publicly relayed measurements give 75–80 °C for dark panels (30 °C ambient in direct sun), and an instrument-panel average of 69 °C after 1 h parked in clear 35 °C weather (Temperature, 2018).
- Marking time: bird droppings 24–48 h; pine-sap type tree gum 3–7 d, bonding from about 48 h; a pure water bead on a hot plate leaves a mineral spot after drying within minutes (all flagged as industry figures).
- Bird-dropping crystalline phase: ammonium urate + struvite (XRD, 6 species, J. Ornithology 2019, Dryad DOI 10.5061/dryad.d39b44r); uric acid pKa1 5.4 / pKa2 10.3, solubility about 6 mg/100 mL at 20 °C.
- Acid rain: clean rain pH≈5.6 (CO2 equilibrium), and below 5.6 is defined as acid rain; the main acid formers are sulfuric acid and nitric acid.
- Spot tests: D1308 cover-glass method drops 1 mL at intervals of 15 min / 1 h / 16 h in 23±2 °C / 50±5 % RH; GB/T 9274-1988 method C about 0.1 mL per drop with drop spacing not less than 20 mm, and method B test period not exceeding 7 d.
- Immersion tests: the ISO 2812-1:2017 liquid family includes EN 590 diesel, EN 228 gasoline, DIN 51604 FAM test fluid, 10 % hydrochloric acid and 5 % sodium hydroxide; conditioning for not less than 16 h.
- Xenon-arc aging: GB/T 1865-2009 relayed figures: chamber air 38±3 °C, black standard temperature BST 65±2 °C, cycle A spray 18 min + drying 102 min, spray-water conductivity not more than 2 μS/cm.
- Acid-etch coupling: ASTM D7356/D7356M-25 reproduces the Jacksonville outdoor acid-rain etching of May to mid-August, with a defect spectrum including 12.7 mm scale spots; no ISO equivalent method.
- 2K cure: published NCO/OH molar ratio range 1.0–1.5; waterborne HDI systems have a pot life of 4–8 h (20 °C); force dry at 60 °C / 30 min; resistance is markedly insufficient before full crosslinking.
- Coatings and film build: polysilazane room-temperature moisture cure to pencil 5H (24–72 h), single layer 0.2–10 μm; factory total build 100–180 μm with 30–50 μm of clearcoat (gauge figures); a single polish removes about 2–5 μm.
8. Frequently asked questions (FAQ)
Q1 Rings on the hood — how do I tell etching from water spotting right there at the car?
Three steps. (1) Mist with distilled water and observe: marks that fade noticeably and return as white spots once dry are mineral water spots (mineral deposits in the D7356 terminology); marks that neither disappear when wet nor when dry, and carry a recessed contour, are acid-etch spots. (2) Glide a fingertip covered with a thin plastic bag across the panel: catching micro-pits mean etching, mere surface roughness means deposition. (3) Read the panel with a paint film thickness gauge: an older panel whose total build is already below about 80 μm should not be accepted as "polishable etching" — make the life judgment first. With all three kinds of evidence in hand, rework disputes fall by more than half.
Q2 Are bird droppings really "strong acid burning the paint"? Does the pH dispute change the scrap call?
Popular accounts say "bird droppings at pH 3–4.5 etch the paint like a strong acid", but the 2019 Journal of Ornithology XRD re-evaluation shows the crystalline phase to be mainly ammonium urate and struvite rather than uric acid crystals, and the industry pH numbers generally lack third-party calibration. The engineering scrap decision does not rest on this dispute: the concentration — shelling — shrinkage of the slurry under sun, plus the swelling and permeation of softened clearcoat by ammonium salts and acid residues, are the common failure path. Whichever chemical description you use, what intake looks at is the trio of exposure time × panel temperature × degree of cure, which is consistent with the logic of ASTM D7356 rating damage with xenon arc plus retained simulated-acid-rain spray.
Q3 A car sprayed with 2K clearcoat was parked overnight and woke up covered in haze marks — whose fault is it?
Check the cure window first. Before full crosslinking a 2K clearcoat still contains mobile chain segments and solvent channels, so beads and contaminants leave marks far deeper than on paint that has been in service for years. The commonly accepted industry criterion for full cure is force drying at 60 °C / 30 min, or air drying at room temperature for about 16 h or more (the product TDS governs). Rain, overnight parking or delivery without shielding before that window puts the responsibility on the coating process, not on the environment. The commissioning party should write "cure-condition record plus pre-delivery exposure control" into the work order at acceptance; for rework, first confirm the damage depth with a D1308 spot test, then decide between polishing and repainting.
Q4 How do you write a "chemical resistance" acceptance clause so nobody can argue about it?
Write the method — condition — criterion trio. Method: ASTM D1308 cover-glass spot or GB/T 9274-1988 method C spotting, plus ISO 2812-1:2017 immersion for fuel scenarios. Conditions: reagent and concentration (for example 3 % acetic acid, EN 590 diesel, DIN 51604 FAM); temperature 23±2 °C plus an additional high-temperature point; observation intervals 15 min / 1 h / 16 h; recovery period. Criteria: the rating direction and target value (for example "10-point scale, 10 = no change, target not below 9"), re-checked against the GB/T 1766 aging ratings. D1308's numeric grading is an industry self-defined scale; if the contract does not state the direction and the target value, two "passing reports" can contradict each other.
Q5 Does a 9H ceramic coating prevent etching? Is a higher contact angle safer?
Look at the two separately. "9H" is a pencil hardness scale with no conversion relationship to etch resistance. The real value of a ceramic coating is the dense inorganic outer layer (polysilazane moisture-cured at room temperature reaching pencil 5H, single layer 0.2–10 μm per published figures) plus the sacrificial layer, which keeps contaminants away from the clearcoat and makes cleaning easier. A high contact angle only means a small wetted area — ASTM D7490 itself declares the method a characterization tool, not a specification test — and a high water-bead angle does not stop a load of bird droppings from sitting on the paint, heating with it and concentrating. Cleanability (easy to wash off) and etch resistance (no permeation) are two metric systems; acceptance needs both, but one cannot be used as evidence for the other.
Q6 Can polishing remove etch marks? Will it not just thin the clearcoat further?
Shallow etching can be leveled until the bottom of the micro-pit is no longer optically visible; with deep etching, once you polish down to the base color it is pointless. Gauge before starting: industry gauge figures give a total factory build of 100–180 μm with 30–50 μm of clearcoat, and a single correction polish consuming about 2–5 μm, so panels averaging below 80 μm get only light treatment. Verify the 60° gloss after polishing per GB/T 9754 and record the result together with orange peel and DOI (Controlling the link between orange peel and distinctness of image DOI), so that "boundary steps" or "gloss loss" are not accepted as "repairable etching".
Q7 What has acid rain got to do with car washing — should I wash right after it rains?
The acid-rain threat happens after the droplet has dried: the sulfuric and nitric acids formed from SO2/NOx concentrate into spot-shaped residues as the water evaporates, and only then do swelling and etching follow. So rinsing surface residue off with clean water soon after rain is an effective action, but do not wash panels that are still hot — fast-drying beads leave calcium and magnesium mineral marks at the same time, producing a combined "acid etch plus mineral" defect. Keep a routine wash rhythm of once every 1–2 weeks with a pH-neutral wash liquid (about 6–8); heavy industrial areas may shorten the interval (maintenance items and intervals: Automotive paint daily care, industry maintenance figures).
Q8 Diesel, gasoline or brake fluid splashed on the paint — which does the damage fastest, and what is the emergency response?
By attack speed the rough order is: brake fluid (glycol ether plus borate ester, hygroscopic and strongly swelling to the clearcoat) and gasoline (a strong solvent that can directly redissolve 1K films) act on a minutes-to-hours scale, while diesel (slow-evaporating, long-acting) acts on an hourly scale. The emergency response is the same in every case: flush immediately with plenty of clean water to dilute, repeatedly; do not rub, which only widens the contact area; keep under observation for 24 h, and if whitish haze spots appear, first decide whether it is interfacial swelling or an actual depression — the former may recover as the solvent evaporates, the latter is treated as etching. That is why ISO 2812-1:2017 lists EN 590 diesel and EN 228 gasoline among its routine test liquids (publicly relayed basis): fuel resistance is a required test item in clearcoat acceptance, not an optional one.
9. References and basis of figures
- ASTM D1308-20 (reapproved 2025, DOI 10.1520/D1308-20R25) "Standard Test Method for Effect of Household Chemicals on Clear and Pigmented Coating Systems"; previous version D1308-02(2013), first issued 1954; the cover-glass spot 1 mL, intervals 15 min / 1 h / 16 h, 23±2 °C / 50±5 % RH and the reagent list (3 % acetic acid, 50 % ethanol, etc.) are taken from the standard's publicly relayed description.
- ASTM D7356/D7356M-25 "Standard Test Method for Accelerated Acid Etch Weathering of Automotive Clearcoats Using a Xenon-Arc Exposure Device" (preceded by the -13 and -19 editions); the terminology definitions, the Jacksonville outdoor window (May to mid-August), the 12.7 mm scale defect spectrum, the G155 xenon arc plus simulated acid rain spray, laying the specimens flat to retain the liquid film, the absence of an ISO equivalent and the §5.1 warranty-claim statement are all taken from the standard abstract and public relays.
- GB/T 9274-1988 "Paints and varnishes — Determination of resistance to liquid media" (current; adopts ISO 2812:1974 equivalently): method A immersion / method B absorbent media (test period not exceeding 7 d) / method C spotting (about 0.1 mL per drop), conditioning at (23±2) °C / 50±5 % RH for not less than 16 h, with rating referred to GB/T 1766 "Paints and varnishes — Rating methods for the degradation of coatings".
- ISO 2812-1:2017 "Paints and varnishes — Determination of resistance to liquids — Part 1: Immersion in liquids other than water" (3rd edition) and ISO 2812-2:2007 (Part 2: immersion in water, 2007-01-15); the EN 590 diesel, EN 228 gasoline, DIN 51604 FAM test fluid and ISO 1514 test panel conditions are on the public relayed basis of testing laboratories.
- GB/T 1865-2009 "Paints and varnishes — Artificial weathering and exposure to artificial radiation — Filtered xenon-arc radiation" (issued 2009-06-02, effective 2010-02-01, IDT ISO 11341:2004, superseding GB/T 1865-1997); the parameters 38±3 °C / BST 65±2 °C and cycle A spray 18 min + drying 102 min are taken from public relays.
- ASTM D7490-13(2022) "Standard Test Method for Determining Surface Tension of Solid Coatings, Substrates and Pigments using Contact Angle Measurements": the two-probe liquid method, the measurable range of about 20–60 dyn/cm and the positioning as "not a quality-control / specification test" are taken from the standard's public abstract.
- SAE J1455-1994 recommended practice for commercial vehicle environmental extremes: design maximum surface temperature of 115 °C in direct sun for windshields and instrument panels, and an ambient design maximum of 85 °C (relayed from Table 1A/1B).
- Crouch N. M. A., Lynch V. M., Clarke J. A.: A re-evaluation of the chemical composition of avian urinary excreta, Journal of Ornithology (2019); accompanying data Dryad DOI 10.5061/dryad.d39b44r — the XRD crystalline phases are ammonium urate and struvite, with no uric acid crystals detected.
- Uric acid base data (pKa1 5.4 / pKa2 10.3, solubility about 6 mg/100 mL at 20 °C): relayed from HandWiki / the CRC Handbook; the acid-rain pH 5.6 threshold and the SO2/NOx acid-formation path: US EPA basis (relayed in a University of Minnesota open textbook).
- Vehicle temperature evidence: McLaren, Quinn & Null (Pediatrics, 2005, reported by Stanford University School of Medicine); Vanos et al. (Temperature, 2018, Arizona State University / University of California San Diego) — instrument panel average of 69 °C inside the vehicle.
- Bauer F. et al. (Prog. Org. Coat. 2005, 53: 183–190, DOI 10.1016/j.porgcoat.2005.02.006), Zhan Y. et al. (Prog. Org. Coat. 2022, 167: 106872), Kozuka H. et al. (ACS Appl. Mater. Interfaces 2013, DOI 10.1021/am400845y) and Barroso G. et al. (J. Mater. Chem. A 2019, 7: 1936–1963): polysilazane moisture-cure kinetics, the PHPS-to-silica conversion and hardness data.
- The Safic-Alcan crosslinker technical review and the Chemzip waterborne 2K hardener comparison (NCO/OH 1.0–1.5; waterborne HDI pot life 4–8 h at 20 °C; 60 °C / 30 min to promote full cure) are on the basis of vendor technical data.
- Public industry figures (no standard number, cited qualitatively): marking windows of bird droppings 24–48 h, tree sap 3–7 d, insect remains hours to days; factory total build 100–180 μm, clearcoat 30–50 μm, 2–5 μm removed per single polish; Nissan Scratch Shield in series production from 2005 and self-healing top-layer activation temperature 40–50 °C; dark panel surfaces at 75–80 °C (30 °C ambient) from media measurements.
Basis of figures: the standard parameters in this article are taken from abstracts of the official standard texts, the announcements on China's national public service platform for standards information, and technical relays by third-party testing laboratories, for use in engineering selection and acceptance communication; before any formal arbitration, the current edition of the standard text governs. Items marked "industry figures" are public experience data from the car-detailing and paint-correction field, without unified laboratory calibration, and are not a numeric basis for scrap decisions. Bird-dropping pH and crystalline phase diverge between the popular-science account and the research re-measurement; this article presents both side by side and states that the divergence does not affect the scrap conclusion. The 2K cure parameters are ranges from vendor public data and vary with resin hydroxyl value and catalyst system.
Last updated: 2026-11-03 | Byline: Kexin New Materials (Guangdong) Co., Ltd. (B2B technical document; trade terms basis EXW / FOB)