ایپوکسی MIO انٹرمیڈیٹ کوٹ Epoxy MIO Intermediate
Two-component epoxy polyamide/micaceous iron oxide high-build intermediate paint — MIO labyrinth effect physical barrier
ایپوکسی MIO انٹرمیڈیٹ کوٹ(Epoxy MIO Intermediate)یہ ایک اعلیٰ کارکردگی والا دو جزوی (2K) اینٹی کاروسن پرائمر ہے، جس میں پولی امائڈ ہیڈنر سے سخت ہونے والا ایپوکسی ریزن فلم بنانے والا مادہ ہوتا ہے اور انتہائی باریک زنک پاؤڈر (خشک فلم میں مقدار ≥70٪) بنیادی زنگ روکنے والا پنجم ہوتا ہے۔یہ کوٹنگ فولاد پر زنک کے قربانی اینود کیتھوڈک طریقے سے فعال زنگ تحفظ فراہم کرتی ہے؛ چاہے خشک فلم مقامی طور پر نقصان پہنچے، آس پاس کا زنک پاؤڈر نقٹے ہوئے فولاد کو برقی کیمیائی تحفظ دیتا رہتا ہے۔CompliesHG/T 3668-2020《ایپوکسی MIO انٹرمیڈیٹ کوٹ》ٹائپ 2 کے مطابق؛ جب اسے ایپوکسی MIO (مائیکا آئرن آکسائیڈ) درمیانی کوٹ اور پولی یوریثین/فلورو کاربن بالائی کوٹ کے ساتھ ملا کر استعمال کیا جائے تو یہ نظام نیوٹرل سلٹ سپرے ≥1000h برداشت کرتا ہے اور ISO 12944 کی اعلیٰ کاروسن ماحول کلاس C4-C5 کی ضروریات پوری کرتا ہے۔سمندر کو پار کرنے والے پلوں، سمندری تیل کے پلیٹ فارمز، پٹرو کیمیکل ذخیرہ ٹینکوں، ٹرانسمیشن ٹاورز، ونڈ ٹربائن ٹاورز اور بڑے فولادی ڈھانچے والی عمارتوں جیسے بڑے منصوبوں میں اینٹی کاروسن پرائمر کے طور پر وسیع پیمانے پر استعمال ہوتا ہے۔
Productsجائزہ
پروڈکٹ کا جائزہ: کس کے لیے؟ کون سا مسئلہ حل کرتا ہے؟
Epoxy MIO intermediate paint is a heavy-duty anticorrosive primer designed for steel structures requiring long-term anticorrosive protection of over 15 years in C4-C5 highly corrosive environments.The core problem it solves is: ordinary anti-rust paints fail within 3-5 years in harsh environments such as coastal areas, chemical atmospheres, and high humidity, whereas epoxy MIO intermediate paint, through the dual mechanism of "cathodic protection + barrier protection", can provide 15-25 years of long-term protection when combined with intermediate paint and topcoat — greatly reducing whole-life-cycle maintenance costs.
مصنوعه کی تعریف
Epoxy MIO Intermediate, Chinese standard number HG/T 3668-2020, is a two-component (2K) ambient-temperature crosslinking-curing anticorrosive primer that uses epoxy resin (bisphenol A type, CAS 25068-38-6) and polyamide curing agent (CAS 68410-23-1) as film-forming substances, ultrafine spherical zinc powder (CAS 7440-66-6, particle size 3-8μm, mass fraction in dry film ≥70%) as anti-rust pigment, and xylene/n-butanol as solvent system.
زنگ سے تحفظ کا طریقہ کار:High-content zinc powder particles in the coating form continuous conductive pathways between themselves and with the steel substrate. Since the standard electrode potential of zinc (-0.76V vs SHE) is lower than that of iron (-0.44V), zinc acts as the anode in corrosion microcells and preferentially undergoes oxidation (Zn → Zn²⁺ + 2e⁻). The released electrons flow through the conductive network to the steel surface, cathodically polarizing the steel below its immune potential—this is known as "sacrificial anode cathodic protection." Meanwhile, the corrosion products of zinc (ZnO, Zn(OH)₂, basic zinc carbonate, etc.) gradually fill the coating pores, forming a dense secondary barrier layer—the "corrosion product self-healing effect."
اہم کارکردگی ڈیٹا:
- The dry film zinc powder content is ≥70% (compliant with HG/T 3668-2020 Category 2).
- Volume solids content ≥60% (ISO 3233:1998)
- Pull-off adhesion ≥6 MPa (ISO 4624:2016, test doll diameter 20mm)
- Single coating resistance to neutral salt spray (NSS) ≥400h (ISO 9227:2022, rust width at the crisscrossing ≤2mm)
- The complete system (epoxy zinc-rich 80μm + epoxy micaceous iron oxide intermediate coat 150μm + polyurethane topcoat 80μm) has an NSS resistance of ≥1000h.
- Mixed application period: 4-8 hours (23°C, main agent: curing agent = 10:1 w/w)
موزوں بنیادیں اور پابندیاں:Applicable to carbon steel, low-alloy steel, and cast iron substrates blasted to Sa2.5 (ISO 8501-1:2007). Not recommended for direct application on galvanized steel (the passivation film on the zinc surface will block the conductive path—sweep blasting pretreatment or an epoxy primer transition layer is advised), stainless steel (the surface passivation film must be removed first), or aluminum alloy (risk of galvanic corrosion—the potential difference between zinc and aluminum is too large). Application temperature limits: standard type 5–40°C (below 5°C, the epoxy-amine crosslinking reaction rate is extremely low, resulting in incomplete coating curing).
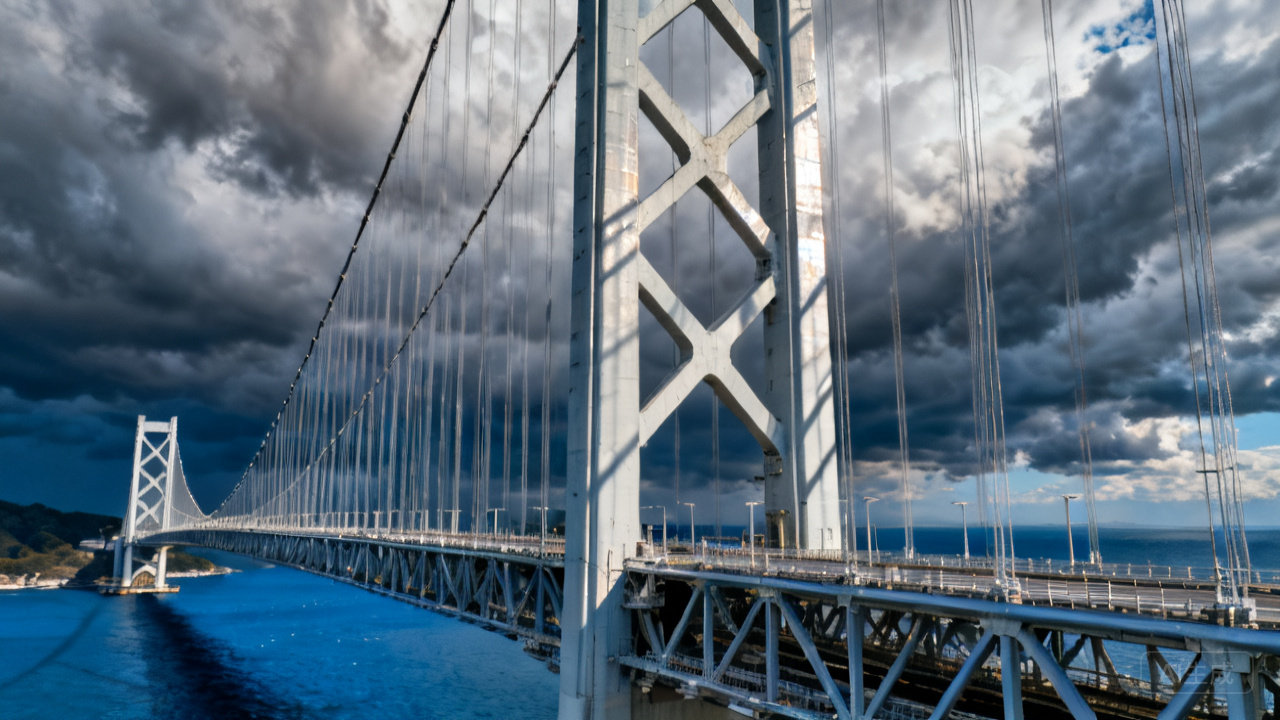
صنعت میں مقام اور اطلاق:ایپوکسی MIO انٹرمیڈیٹ کوٹis one of the most widely used primer types in global heavy-duty anticorrosive coating systems (ISO 12944-5:2019 systems A2.08/A3.08/A4.08, etc.), forming a classic triple-protection system with epoxy MIO intermediate coat and PU/fluorocarbon/polysiloxane topcoat. Typical applications include: Akashi Kaikyo Bridge Japan (opened 1998, 100-year design life), Hong Kong-Zhuhai-Macao Bridge (opened 2018, 500,000m² steel box girders), North Sea offshore oil platforms (NORSOK M-501 system certification), etc. According to Grand View Research, the global zinc-rich primer market was approximately USD 2.8 billion in 2023, with Asia-Pacific accounting for 48% share.
ProductsFeatures
1. Cathodic protection (sacrificial anode) mechanism
The dry film of the coating contains ≥70% zinc powder, forming a continuous conductive network. The standard electrode potential of zinc (-0.76V) is lower than that of iron (-0.44V). When corrosion occurs, zinc preferentially oxidizes (Zn→Zn²⁺+2e⁻), releasing electrons that cathodically polarize the steel to its immunity potential — even if the coating has 3-5mm damage, the surrounding zinc powder can still provide continuous electrochemical protection for the exposed steel, which makes the anticorrosive performance of epoxy MIO intermediate paint far superior to ordinary anti-rust primers that rely only on physical barrier.
2. Superior corrosion resistance and durability
Single coating NSS≥400h (HG/T 3668 Class 2), and the system with epoxy MIO intermediate paint + polyurethane topcoat achieves NSS≥1000h. Under the C5-M extremely high corrosion environment (marine splash zone) of ISO 12944-2, the design service life is 15-25 years. The Akashi Kaikyo Bridge in Japan adopted an epoxy MIO intermediate paint system in 1998, and the coating remains intact after more than 25 years — the actual service life far exceeds the design value.
3. Excellent compatibility
It has excellent intercoat adhesion (pull-off method ≥5MPa) with epoxy MIO intermediate paint (MIO barrier layer), polyurethane topcoat (weather-resistant decorative layer), fluorocarbon topcoat (ultra-weather-resistant ≥25 years), and polysiloxane topcoat (high weather resistance + high chemical resistance). Epoxy MIO intermediate paint + epoxy MIO intermediate paint + topcoat is the most classic three-coat heavy-duty anticorrosion system in ISO 12944-5 — the primer provides cathodic protection, the intermediate paint provides thickness and physical barrier, and the topcoat provides weather resistance and decoration.
4. Wide adaptability to construction
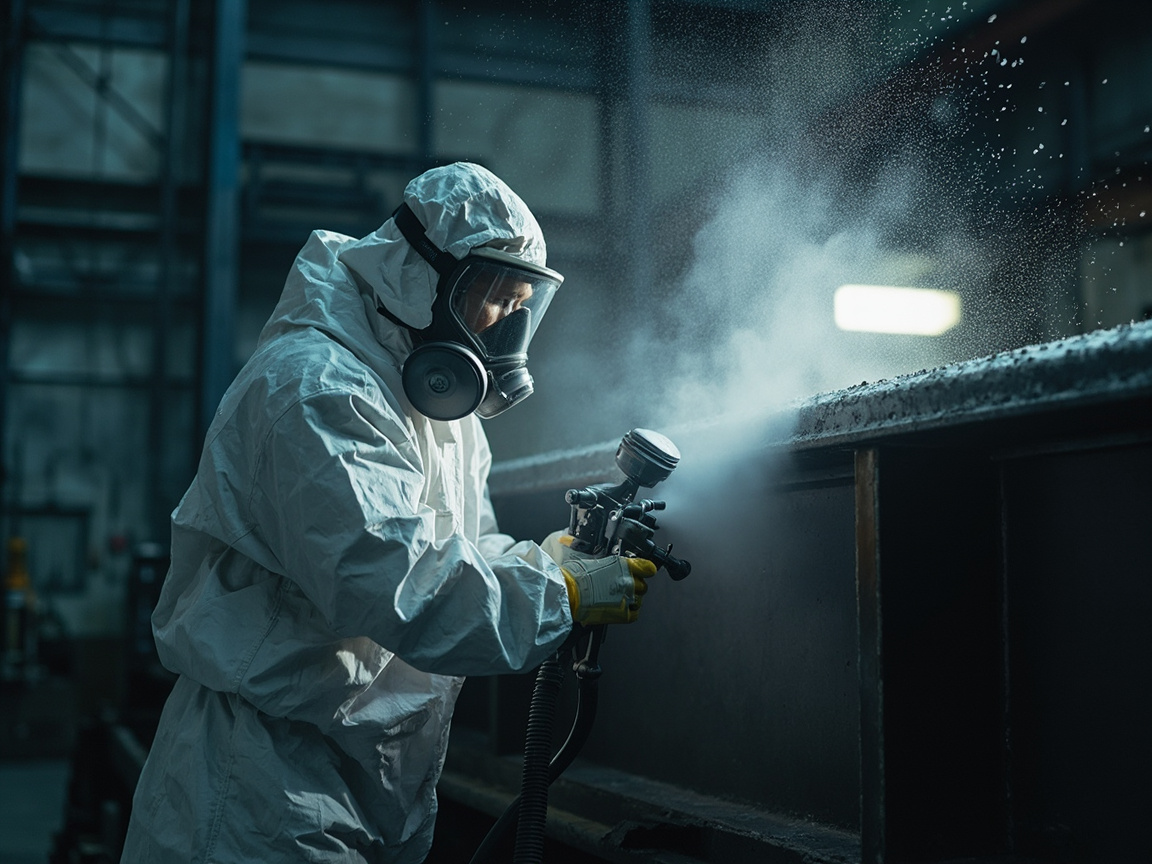
Supports airless spray (nozzle 0.43–0.53 mm, 15–25 MPa), air spray, and brush/roller application (for small-area touch-ups). Single-pass dry film thickness: 60–80 μm. Mixing ratio: 10:1 (w/w). Pot life: 4–8 h (23°C). Wide temperature range for application (5–40°C); low-temperature formulation can be applied down to –5°C. Continuous stirring is required during spraying to prevent zinc powder sedimentation—use of a pressure pot with a pneumatic agitator is recommended to ensure coating uniformity.
5. Shop Primer Solderability
Specialized formulation (dry film 15-25μm) can be used as a shop primer—after application in the steel structure prefabrication plant, the steel remains suitable for welding and cutting. Welding fumes comply with occupational exposure limits (GBZ 2.1-2019), and the pass rate of X-ray inspection of welds is not affected. Suitable for automated spray painting on steel structure production lines—parts can be handled and stacked within 3-5 minutes after spraying. Note: Only the specialized shop primer formulation is weldable—the standard type with a dry film thickness of 60-80μm is not suitable for welding.
6. Environmental Compliance · Global Standards
Complies with HG/T 3668-2020 (China) Standard Class 2, ISO 12944-5:2019 system numbers A2.08/A3.08/A4.08, NORSOK M-501:2022 (Norwegian Petroleum Industry) System 1, SSPC Paint 20 (USA) Zinc-rich Primer Type II (≥77% zinc powder). VOCs<420g/L(GB 30981-2020),可通过ROHS 2011/65/EU和REACH (EC) 1907/2006ComplianceTesting。Products碳足迹约2.8kg CO₂e/kg(摇篮到大门,SimaPro 9.5计算)——低于غیر نامیاتی زنک امیر پرائمر(3.5kg CO₂e/kg)。
تکنیکیParameter
طبعی کیمیائی پیرامیٹرز
خشک ہونا اور کارکردگی
• March 2024, National Coatings Quality Inspection and Testing Center Test Report (No.: NTC-2024-0315-ZR)
· HG/T 3668-2020 "Epoxy MIO Intermediate Paint" Class 2 indicators
The data in this table are typical values under standard laboratory conditions (23±2°C, 50±5%RH). Actual values may vary slightly depending on the substrate condition, construction process, and environmental conditions. Please contact technical support to obtain the batch COA (Certificate of Appointment).
ApplicationProcess
سطح کی تیاری
Sandblast to Sa2.5 (ISO 8501-1:2007), roughness Rz 40-75μm. Manual rust removal ≥ St3. Grease must be removed with SSPC-SP1 solvent. Primer application (RH) must be completed within 4 hours after sandblasting.<50%可延至8h)。禁忌:雨天/雾天/سبسٹریٹ کا درجہ حرارت低于露点3°C时禁止Application。
کوٹنگ کی تیاری
Stir the main agent for 3-5 minutes until the zinc powder is completely and evenly dispersed. Add the curing agent at a ratio of 10:1 (w/w) and continue stirring for 3-5 minutes. Let it stand for 15-30 minutes (23°C) to mature. Continuously stir during application to prevent zinc powder from settling—a pneumatic mixer is recommended. The mixed usable period is 4-8 hours (23°C). Do not dilute and use materials that have gelled beyond this period.
پرائمر اطلاق
Airless spraying (recommended): Nozzle 0.43-0.53mm/0.017-0.021", pressure 15-25MPa. Air spraying: Nozzle 1.5-2.0mm, pressure 0.3-0.5MPa. Brush/roller coating is only suitable for small-area pre-coating and repair. Single-coat DFT 60-80μm. Pre-coat welds, free edges, etc.
خشک ہونا اور دوبارہ کوٹنگ
Surface dry ≤ 1h (23°C), hard dry ≤ 24h. Minimum recoating interval 8h (23°C). Maximum recoating interval 7d—exceeding this interval requires sandblasting (low pressure 0.2-0.3MPa, non-metallic abrasive) to remove surface zinc salts (basic zinc carbonate). Matching: Epoxy micaceous iron oxide intermediate coat 100-150μm → Polyurethane/fluorocarbon topcoat 50-80μm × 2.
Inspection and Acceptance
DFT measurement (ISO 2808:2019, SSPC-PA2): 80% of measuring points ≥ specified value, no measuring points<80%规定值。چپکنے کی طاقتTesting(ISO 4624 پل-آف ٹیسٹ或ISO 2409کراس کٹ طریقہ)。سوراخوں کی جانچ(گیلے سپنج کا طریقہ,67.5V/90V)。ظاہری معائنہ:无سگنگ/漏涂/起泡/缩孔/زنک پاؤڈر不均匀。
استعمالاتField/Area
سمندری/دریائی پل
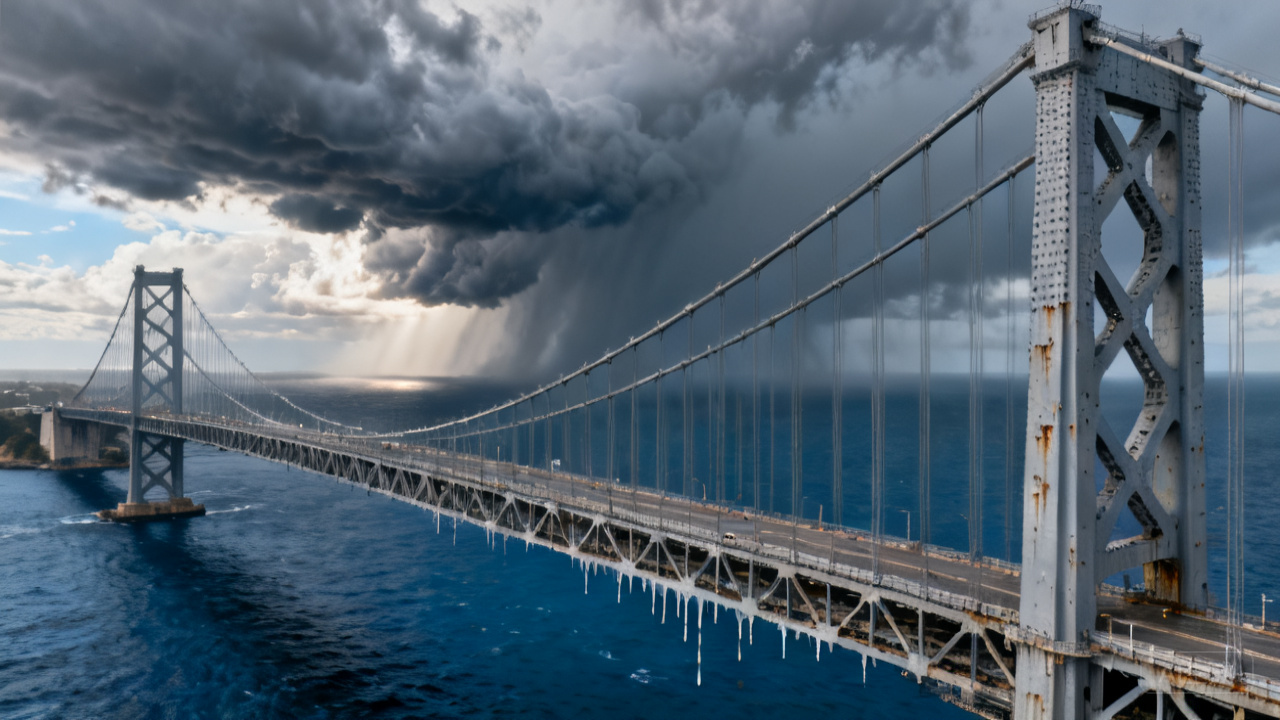
اسٹیل باکس گرڈر، پل کے مینار، محرابی پسلیاں
آف شور آئل پلیٹ فارم
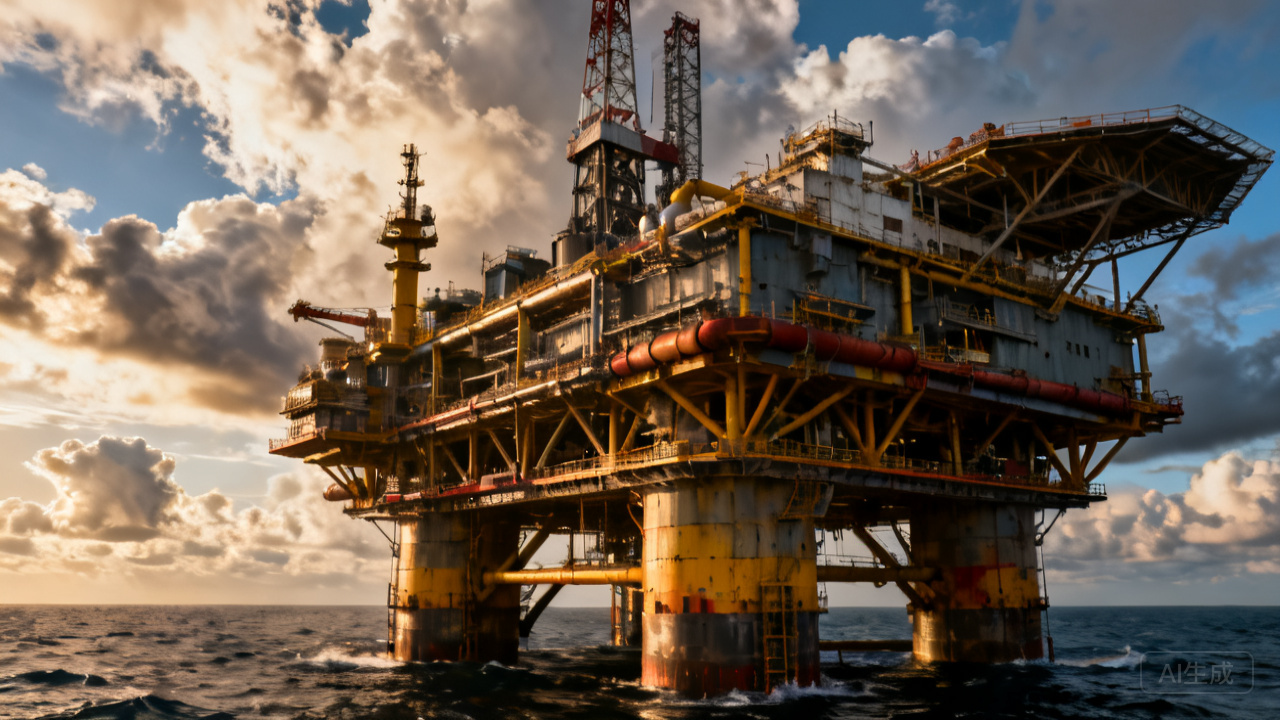
جیکٹ، ڈیک، رہائشی ماڈیول
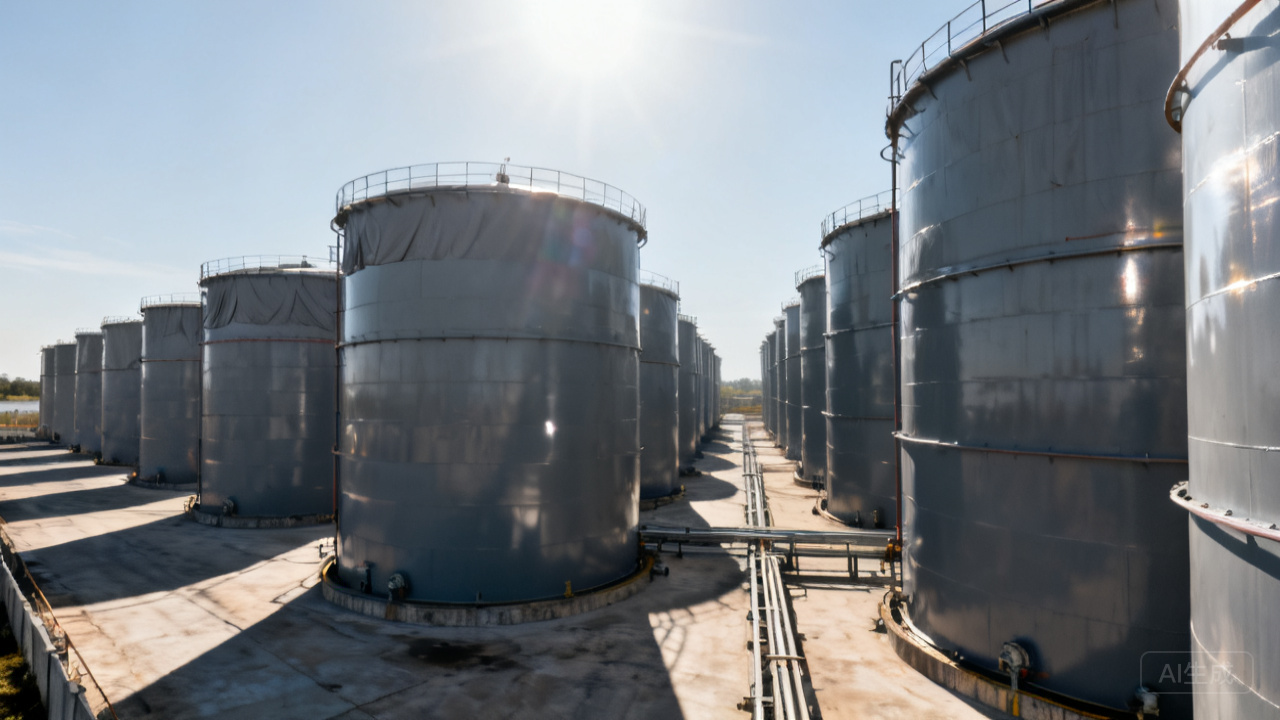
پیٹرو کیمیکل ٹینکوں کی بیرونی دیوار
خام تیل/ریفائنڈ پروڈکٹس/کیمیکل ٹینک
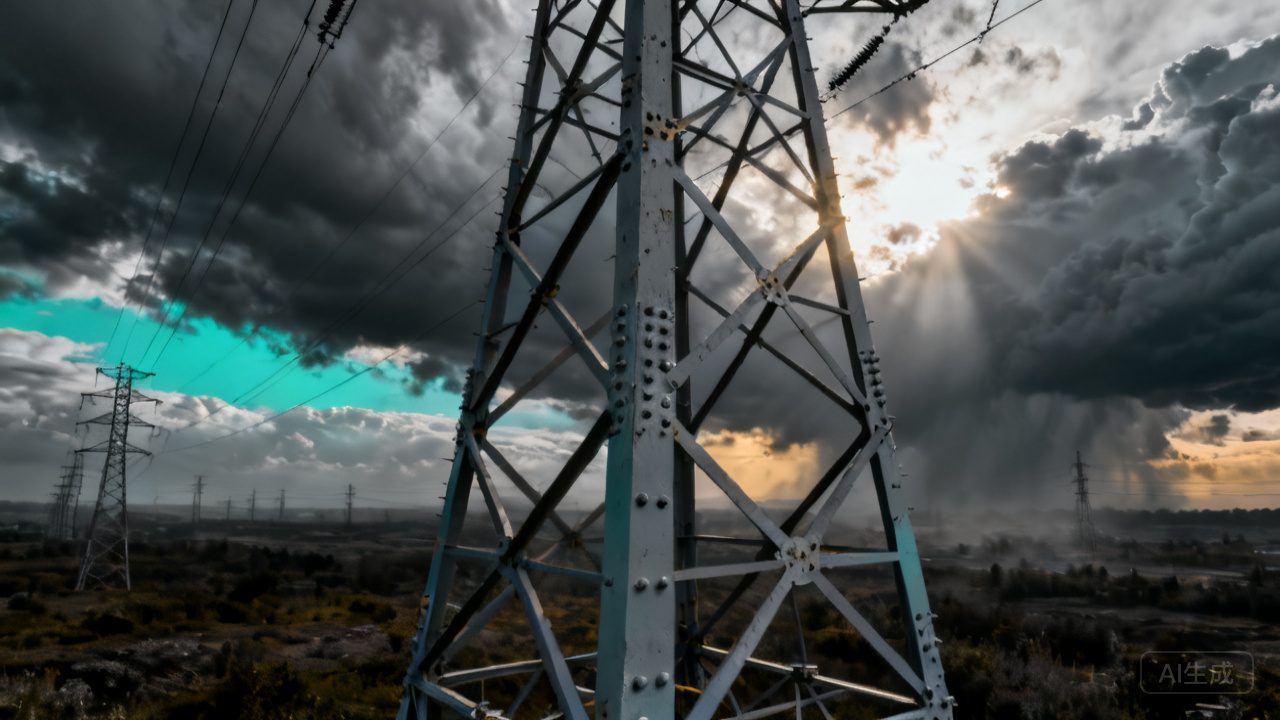
ٹرانسمیشن ٹاورز/نلی نما ٹاورز
ہائی وولٹیج/الٹرا ہائی وولٹیج لائنوں کے اسٹیل ڈھانچے
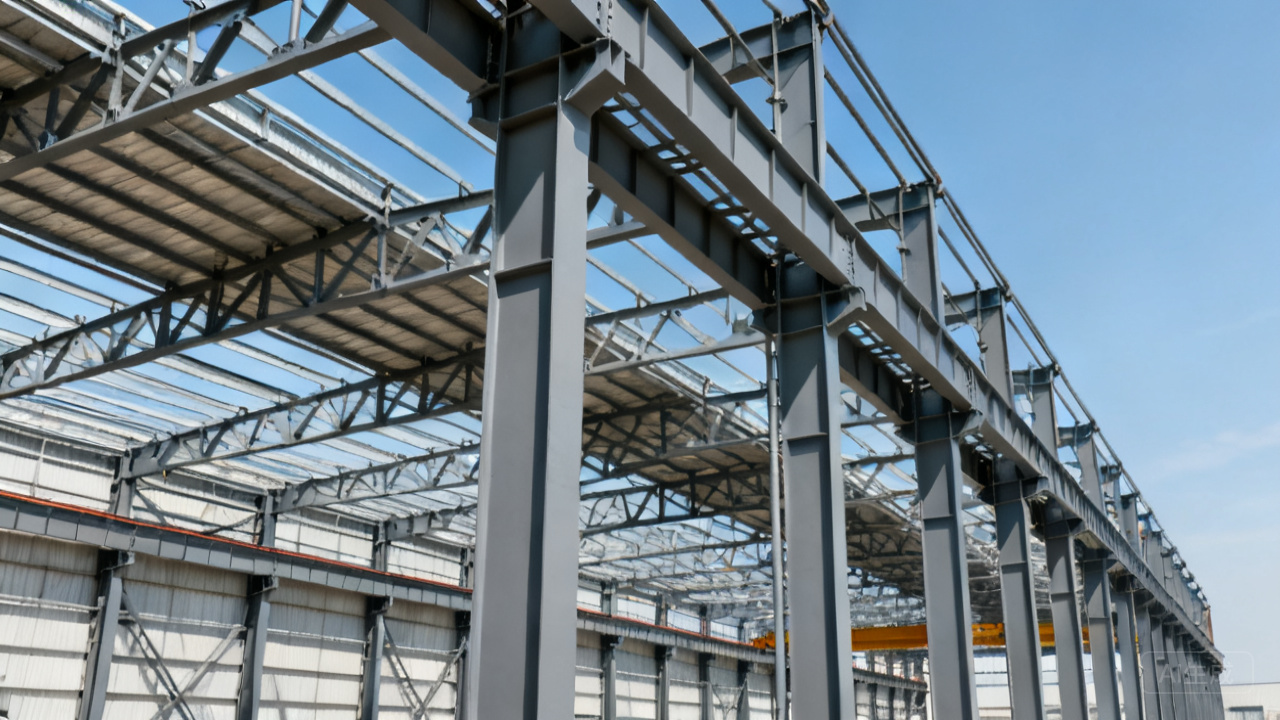
بڑے اسٹیل اسٹرکچر فیکٹریاں
صناعتی عمارات، کھیلوں کے میدان
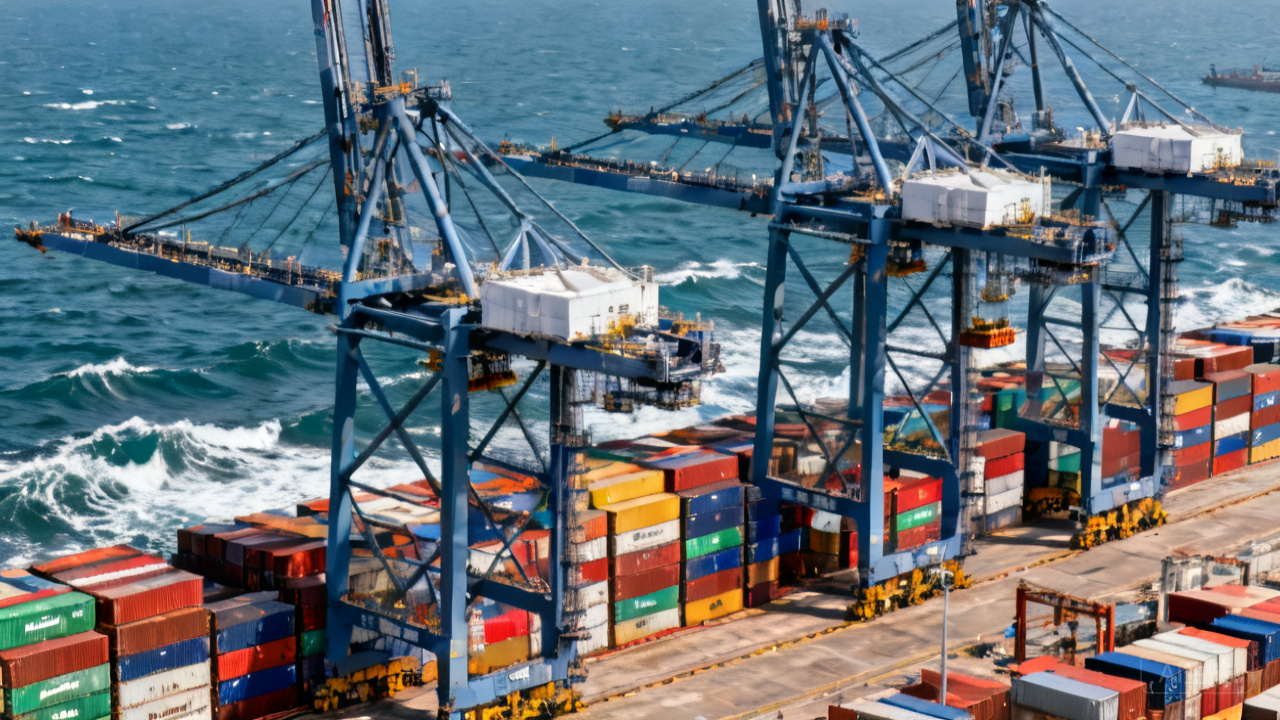
بندرگاہی مشینری
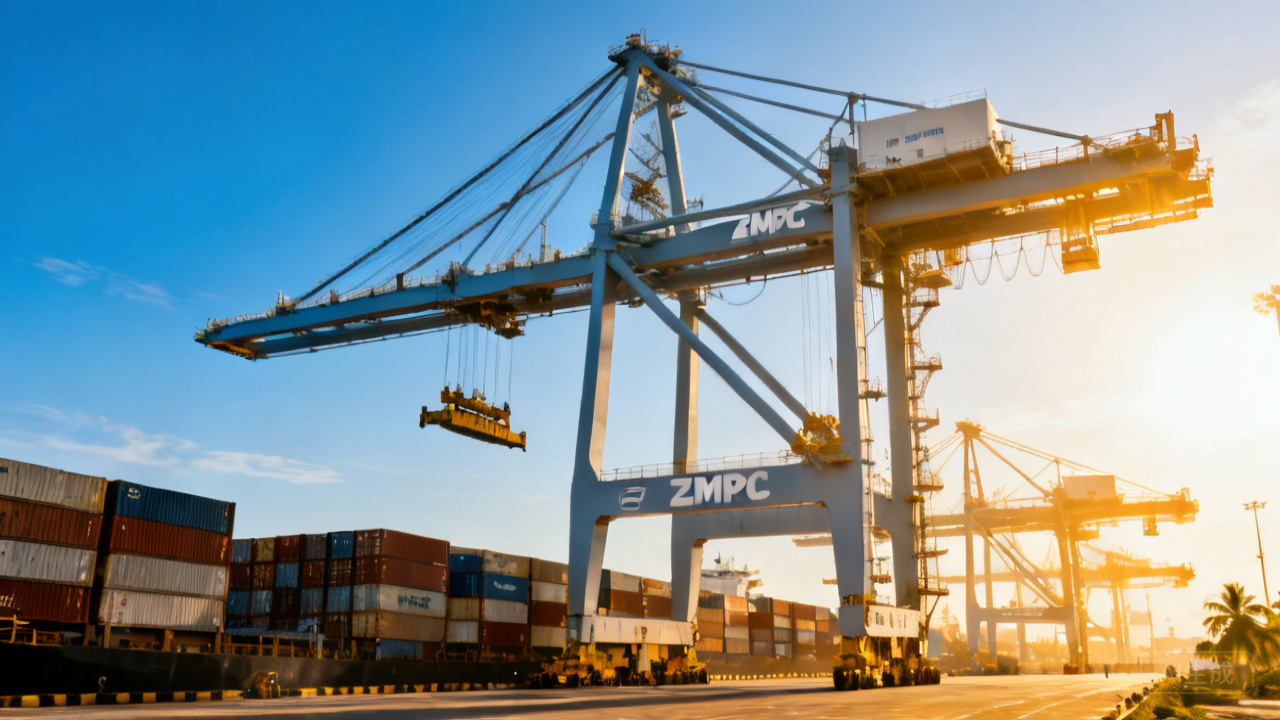
برتھ کرین، گینٹری کرین، شپ انلوڈر
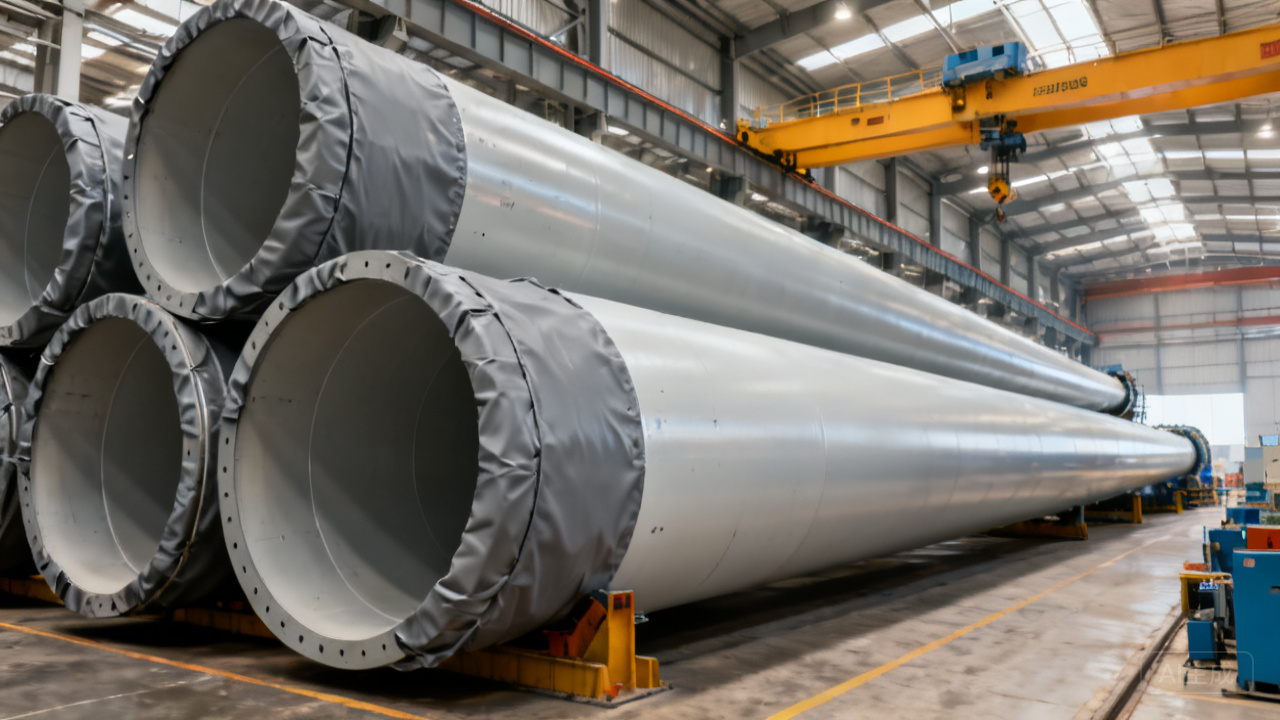
ونڈ ٹربائن ٹاور
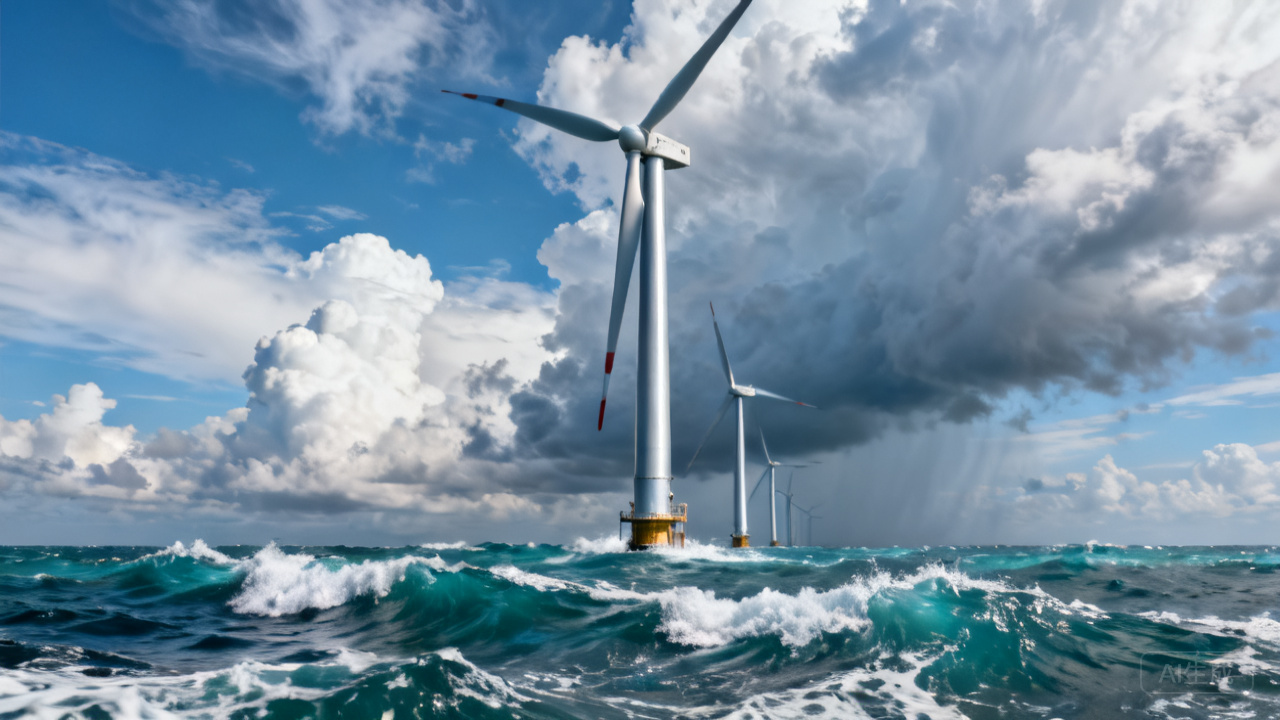
خشکی/سمندری ونڈ ٹربائن ٹاورز
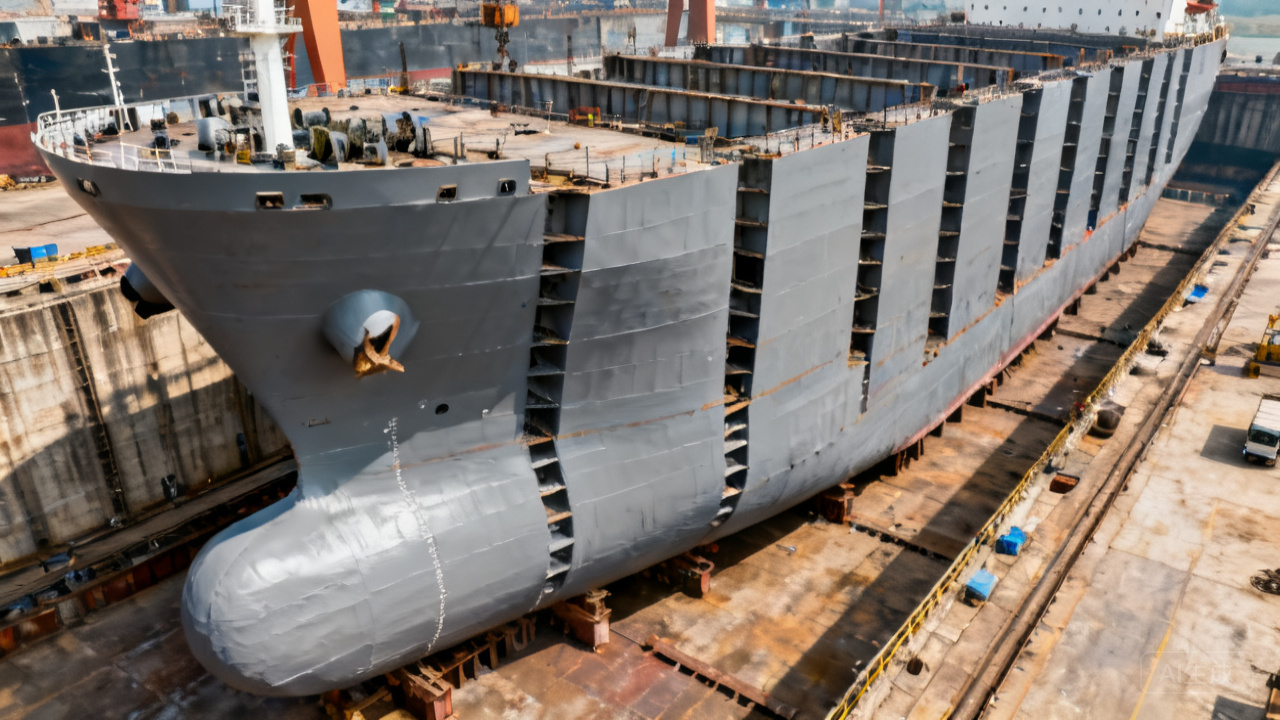
جہاز سازی اور سمندری انجینئرنگ
ہل بلاکس، بیلاسٹ ٹینک، ڈیک
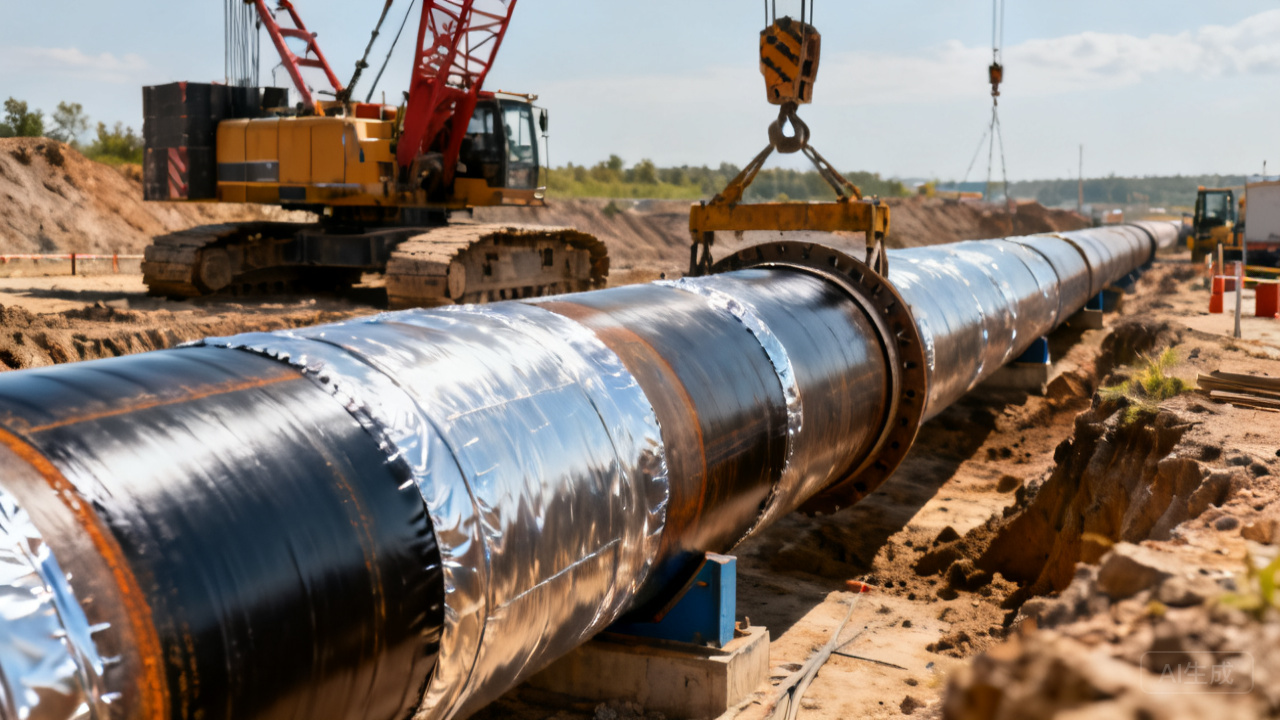
پائپ کی بیرونی دیوار کی اینٹی کوروشن
تیل/گیس/پانی کی طویل فاصلہ پائپ لائنیں
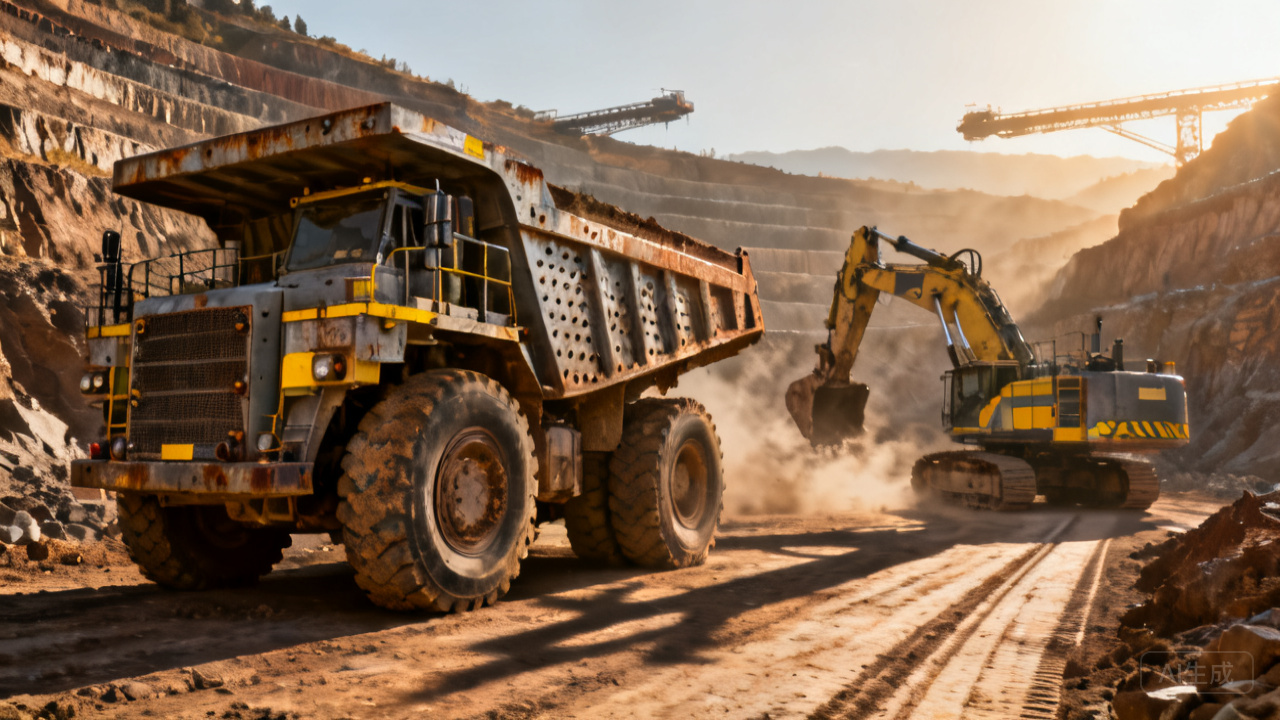
کان کنی/تعمیراتی مشینری
ایکسکیویٹر، کولہو، کنویئنگ آلات
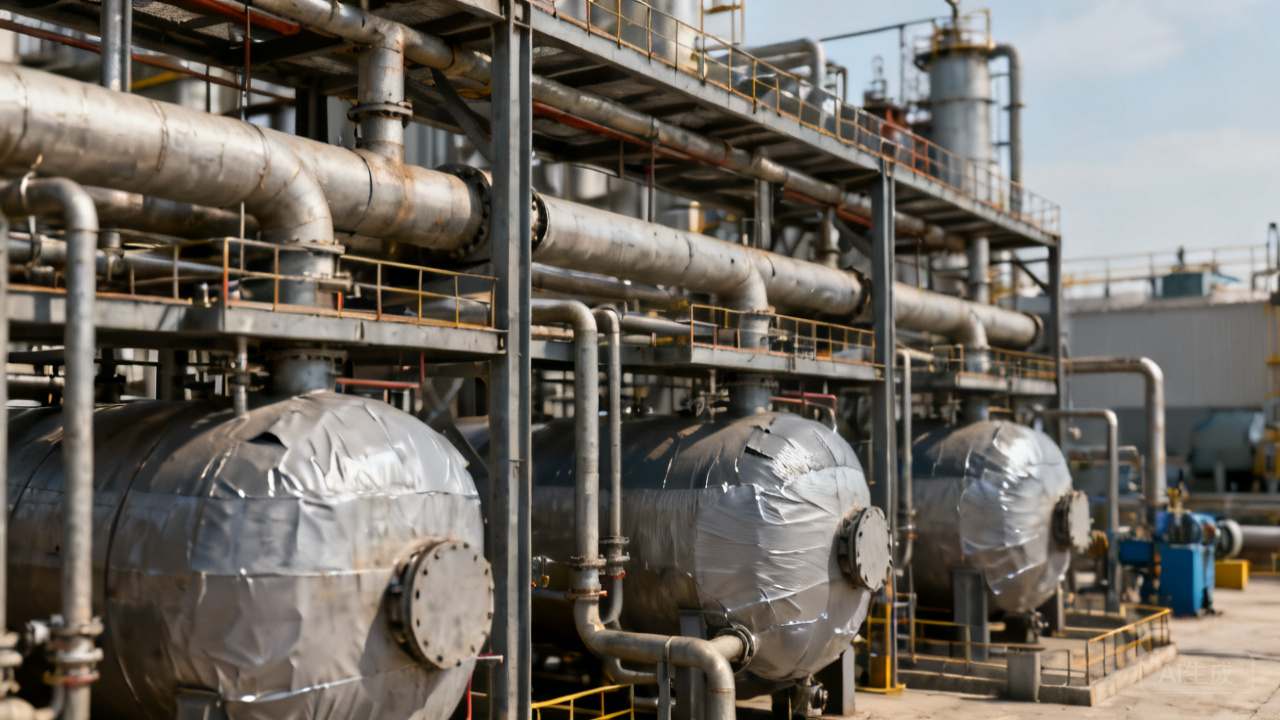
کیمیائی/ریفائنری پلانٹس
ری ایکٹر، ہیٹ ایکسچینجر، پائپ ریک اسٹیل اسٹرکچر
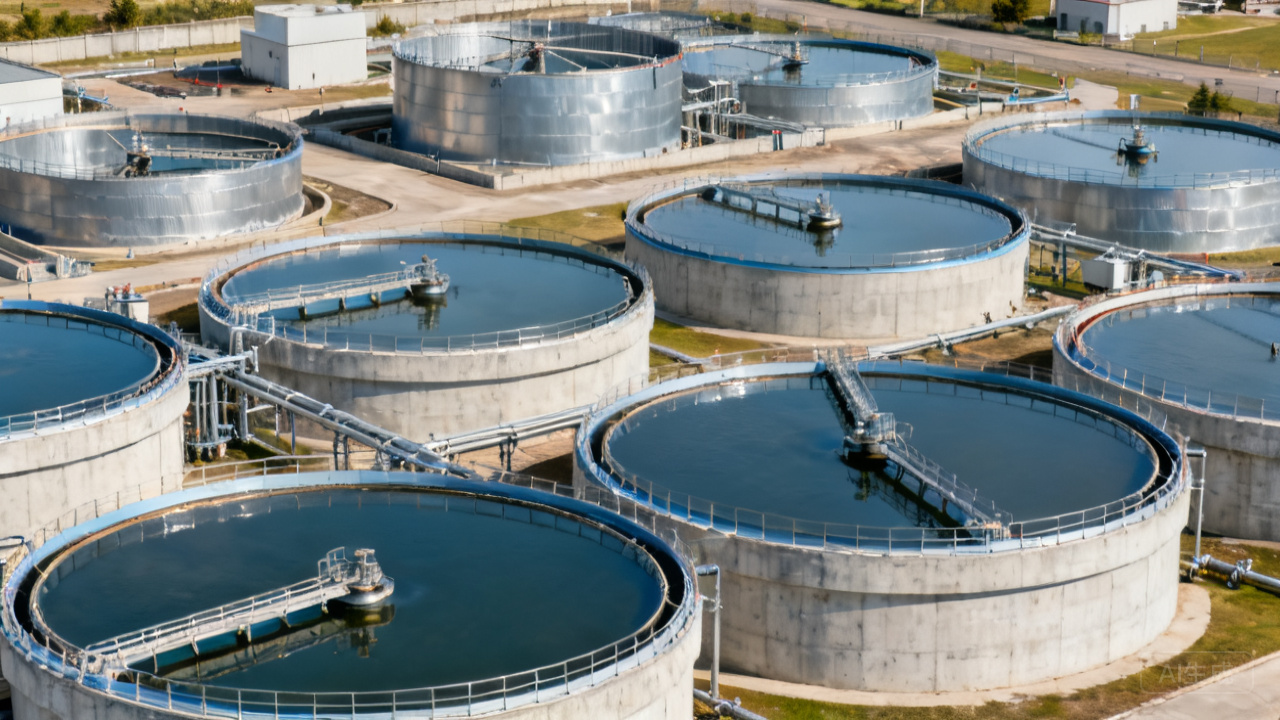
واٹر ٹریٹمنٹ/آبی تنصیبات
سیوایج پلانٹس، سلویس گیٹس، ٹریش ریکس
اکثر پوچھے گئےسوالات
ڈاؤن لوڈسینٹر
TDS Product Technical Specifications
Technical Data Sheet
Compliant with HG/T 3668-2020 standard
MSDS (Material Safety Data Sheet)
Material Safety Data Sheet
16 Chapters · GB/T 16483-2008
Color Card (Product Color Card)
Color Card
سٹیل گرے/آئرن ریڈ معیاری رنگ
درخواستی گائیڈ
Application Guide
Complete construction guidance + defect countermeasures
انجینئرنگکیس
جاپان کے اکاشی کائیکیو پل کے اسٹیل باکس گرڈر کی اینٹی کوروشن
بحیرہ شمالی کے سمندری تیل پلیٹ فارم جیکٹس کے لیے بھاری اینٹی کوروشن
انڈیا کی چنئی بندرگاہ پر ZPMC کنٹینر برتھ کرین کی اینٹی کوروشن
جنوبی چین سمندر میں آف شور ونڈ فارم کے ٹربائن ٹاورز کی زنگ سے حفاظت
Epoxy micaceous iron oxide intermediate paint·سیدھا کارخانے سے
Free sample testing · Customized technical solutions · On-site construction guidance · ISO 9001 certified factory · 48-hour rapid response