
Scratch resistance and abrasion resistance of a furniture coating film are two indicators that judge different objects. Scratch resistance measures the ability of the coating film to withstand a sharp, localised contact such as a scratch stylus without producing a visible scratch at least 0.30 mm wide under a specified load; the result is expressed in newtons (N) and the test method standard is GB/T 4893.10-2024. Abrasion resistance measures the ability of the coating film to resist wear-through, material loss by abrasion and exposure of the substrate under repeated rubbing; the result is expressed in abrasion revolutions (r), abrasion loss (mg/100 r) or a wear grade from Grade 1 to Grade 5, and the test method standard is GB/T 4893.8-2023. Neither indicator can replace the other, and neither can be represented by one generic “hardness” figure.
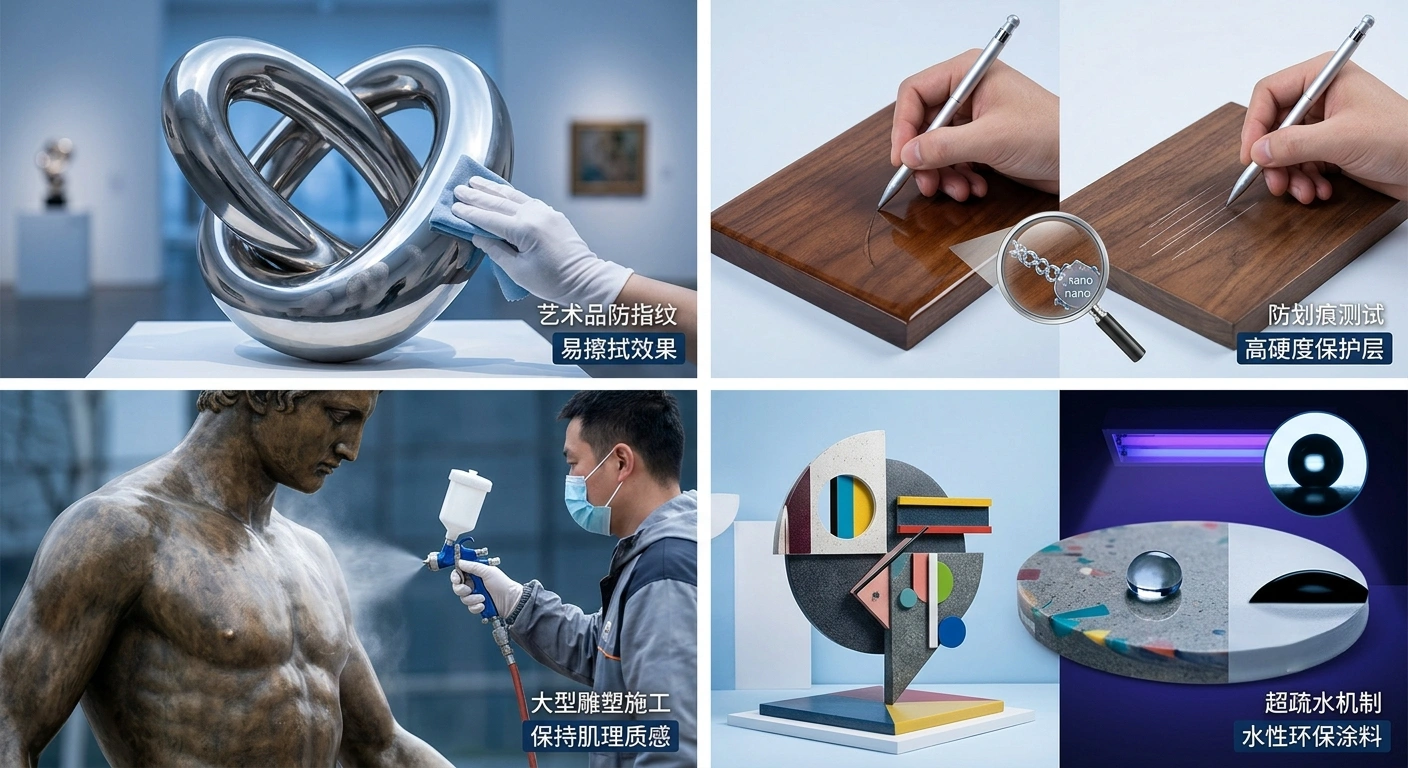
A furniture maker exporting sintered-stone and solid-wood dining table tops once met a typical complaint: the customer reported that “a few weeks of wiping with a damp cloth left the surface hazy and white, and one pass of a key leaves a white line”, while the factory’s outgoing inspection sheet showed a green pass for “abrasion resistance, 1 000 r, ≥ Grade 3 acceptable”. Third-party retesting produced two sets of data. On the abrasion path of GB/T 4893.8 the film showed no whitening after 1 000 r and was graded Grade 2; on the stylus path of GB/T 4893.10-2024 a continuous scratch 0.30 mm wide appeared at 5.0 N, which means the final scratch resistance value was only the 5.0 N grade. The post-mortem pointed to three linked causes — ① to force the gloss below 5 the formulation used an 8 μm grade fumed silica and took the total matting component to 8%, so rigid particles cut into the continuous phase of the film-forming resin; ② the share of soft matting (polyethylene wax micropowder) was too low, leaving no lubricating layer at the surface and a friction coefficient that ran high; ③ the measured dry film thickness of the top coat was only about 35 μm, so the stylus easily penetrated the top coat and reached the primer interface. The corrective direction was not a blanket “make it harder” but a redesign of particle-size grading, hard/soft matting blends, film thickness and sealer/top-coat pairing. This case shows that scratch resistance and abrasion resistance are two different matters, with different criteria, different instruments and different corrective paths.
TL;DR: quantified criteria you can write straight into a technical agreement
- Two separate criteria sets: scratch resistance gives a minimum load (N) under GB/T 4893.10-2024 (issued 2024-09-29, implemented 2025-04-01, administered by the National Furniture Standardization Technical Committee SAC/TC 480); abrasion resistance gives abrasion revolutions, abrasion loss or a Grade 1 to Grade 5 classification under GB/T 4893.8-2023 (issued 2023-09-07, implemented 2024-04-01, modified adoption of ISO 4211-5:2021).
- Stylus geometry decides the result: diamond conical head with rounded-tip radius R=(0.30±0.01) mm and cone angle α=(60.0±1.0)°; load range 1.0 N to 20.0 N with increments of 1.0±0.1 N; relative speed of stylus against surface (20±2) mm/s over a travel length of ≥22 mm; the acceptance threshold is a scratch width ≥0.30 mm, measured with equipment accurate to ±0.05 mm.
- Conditioning is part of the result: test atmosphere (23±2) ℃ and relative humidity (50±5)%; GB/T 4893.10-2024 requires specimens to be pre-conditioned in the same atmosphere for at least 48 h and the scratch to rest 24 h in the same atmosphere before width is measured; the EN 15186 series requires the test surface to be conditioned at the same temperature and humidity for at least 1 week.
- The first visible mark has its own ring method: EN 15186 Method B uses a hemispherical diamond tip R=(0.090±0.003) mm with an apex angle of (90±1)°, loads from 0.1 N to 10.0 N, a turntable at (5±1) r/min, a viewing box with a 70 W halogen lamp (1 200 lm, 2 800 K) at an illuminance of 950±150 lx, and a 100 mm×100 mm template with 8 viewing slots; the verdict is reached when continuous marks appear in at least 6 slots, and the result is quoted to 0.1 N.
- A matt finish is bought at a price: on published figures, bringing 60° gloss down to about 30 usually takes a 3 μm to 5 μm matting agent, while getting below 5 often requires 8 μm and coarser. Hard/soft matting blends are the usual way to soften the disruption of the continuous phase by rigid particles — in a semi-matt system hard matting is 70% to 80% and soft matting 20% to 30%, in a full matt system 50% to 60% and 40% to 50%.
- Do not accept on one number any more: the product standard GB/T 3324 series lists the physical and chemical properties of the coating film as mandatory items (liquid resistance, damp heat resistance, dry heat resistance, adhesion, abrasion resistance, impact resistance and others), whereas the scratch load has no unified acceptance line in purchase specifications and must be agreed between supplier and buyer in terms of method and load threshold.
I. Four easily confused terms: scratch resistance, abrasion resistance, scrape resistance and blocking
1. Load-based and revolution-based: the fundamental difference in what is judged
Scratch resistance follows a load-based logic: a stylus of fixed geometry is pressed onto the surface of the coating film, drawn across a specified length, and the question is what minimum load will cut a mark whose width reaches 0.30 mm. It simulates damage of the “local, high-stress, single-event” type — keys, cutlery, pet claws, dragged hard objects. Abrasion resistance follows a revolution-based or mass-loss logic: rubber abrasion wheels or sandpaper are run repeatedly over the same area under a given load, and the question is after how many revolutions whitening or wear-through to the substrate appears, or how many milligrams are lost per unit of revolutions. It simulates damage of the “areal, cumulative, many-cycle” type — cleaning wipes, objects shifted repeatedly, handling friction. With one and the same formulation the two rankings can be exactly reversed: a highly crosslinked system may show an impressive stylus load yet lose material early under the abrasion wheel because of its brittleness, while a flexible system may show very little abrasion loss yet be pushed into a plastic ridge under the stylus and reach the width limit early.
2. Whitening and gloss change do not mean “not damaged”
Two appearances are common after a matt wood coating film has been scratched: a white line on a dark substrate (stress whitening, where micro-voids inside the film scatter light) and a bright patch (where the raised scratched face has turned diffuse reflection into specular reflection). GB/T 4893.10-2024 uses “width ≥0.30 mm” as its measurable threshold and converts whitening and raised ridges alike into a geometric dimension; EN 15186 Method B deliberately takes as its object the “first visible mark, which may be no more than a change of gloss”, and with a viewing box and a template turns subjective visibility into a count of “6 of 8 slots”. Our related article on this site, Matte gloss stability and matting agent settling control, deals with the batch-to-batch stability of gloss itself; this article deals with how gloss is read after mechanical damage, and the two together cover the full quality line for matt furniture top coats.
II. GB/T 4893.10-2024: how the 0.30 mm scratch criterion is measured
1. Instrument and geometry: stylus radius, load increment and speed
The standard separates two types of scratch tester: one places the weights directly on the stylus to obtain the test load, the other slides the weights along the load beam to obtain a progressive load, but the technical parameters are the same — load range 1.0 N to 20.0 N, load increment 1.0±0.1 N, linear velocity of the stylus tip relative to the test surface (20±2) mm/s, travel length ≥22 mm. The stylus tip is made of diamond, with a rounded-part radius R=(0.30±0.01) mm and an apex angle α=(60.0±1.0)°; the junction between the spherical part and the cone cross-section must be such that scratches with a width greater than or equal to 0.30 mm are produced. Equipment used to measure scratch width must be accurate to ±0.05 mm, and equipment used to inspect the stylus tip geometry to ±0.01 mm. The stylus is inspected visually before every test and replaced as soon as loss of flatness, pitting or any other damage is found.
2. Specimens, environment and the moment of measurement
A specimen may be a section cut from a finished piece of furniture, or a test panel made from the same materials with the same finishing method. Pre-conditioning requires at least 48 h in an atmosphere of (23±2) ℃ and relative humidity (50±5)%. Before testing, the surface is wiped with a soft, absorbent white cleaning cloth and must not be scratched; test points are kept at least 20 mm from the edge of the panel and at least 5 mm between two adjacent scratches. The first test surface starts at 1.0 N and the load is increased in 1.0 N steps up to 20.0 N or until the scratch width is not less than 0.30 mm, whichever is reached first; the second and third test surfaces start at a load 3.0 N below the result of the first surface. The scratches rest for 24 h under the test atmosphere before width is measured, and where necessary a suitable dye is applied to the scratch to make measurement easier; where applicable, scratches are made along the direction of the wood grain. For data treatment, where 1 inspector takes the measurements the preliminary assessment value is used as the intermediate assessment value, and the average of the intermediate assessment values from the 3 test surfaces is taken as the final value, quoted to 1.0 N; in a dispute, 3 inspectors take the measurements and the average is used. If no scratch of the specified width is obtained even at the maximum load of 20.0 N, the test report records the scratch width actually obtained at 20.0 N.
| Item | Specified value or range | Effect on the result |
|---|---|---|
| Scratch width acceptance threshold | ≥0.30 mm | Fixed threshold; whitening and raised ridges are both converted into geometric width |
| Stylus tip radius R | (0.30±0.01) mm, diamond | A larger radius lowers contact stress and biases load readings systematically high |
| Apex angle α | (60.0±1.0)° | With the spherical cap it defines the shape of the scratch walls |
| Load range and increment | 1.0 N to 20.0 N, increment 1.0±0.1 N | Result resolution is 1.0 N; differences within 2 N carry no interpretive meaning |
| Travel speed | (20±2) mm/s | A higher speed makes a viscoelastic system respond as if “harder” |
| Travel length | ≥22 mm | Too short makes the width unstable to measure, too long runs into panel defects |
| Environment and pre-conditioning | (23±2) ℃, (50±5)% RH, at least 48 h | Departures in temperature and humidity change film modulus and reading directly |
| Time of measurement | Rest 24 h after scratching | Measuring width too early underestimates the residual mark after rebound |
| Width measurement accuracy | ±0.05 mm | Reading differences at the 0.05 mm level are method noise |
| Result expression | Quoted to 1.0 N, average of 3 surfaces | The report must state whether the threshold was missed at 20.0 N |
III. EN 15186 Method A and Method B: penetrating marks and visible marks divided
1. Method A linear test: almost the same origin as the national standard
The European standard EN 15186 (covering the DIN EN 15186:2022 and EN 15186:2024 editions) specifies methods for assessing the resistance of surfaces to visible scratches of various kinds. It applies to all finished rigid surfaces regardless of substrate, and not to leather or textile coverings. Method A uses a conical diamond scratch head (radius 0.30±0.01 mm, angle 60±1°), loads from 1 N to 20 N in steps of 1 N, a linear (non-manual) traverse across the surface, width measured with optical equipment accurate to ±0.05 mm, and reports the minimum load that produces a scratch at least 0.30 mm wide, with the final value quoted to 1 N; its traversing device must satisfy the linear-motion principles of EN ISO 1518-1. Method A is explicitly not applicable to melamine-faced panels (EN 14322) or high-pressure decorative laminates HPL (EN 438-1) — for those two surface families the European system uses a different test philosophy, while GB/T 17657-2022 gives, for the scratch resistance of wood-based panels and decorated panels, a decorative-overlay criterion at two load levels, 1.5 N and 2.5 N.
2. Method B ring test: catching the moment “the gloss changed”
Method B is applicable to surfaces of all types. A hemispherical diamond tip (radius 0.090±0.003 mm, apex angle 90±1°) is loaded in decreasing steps (0.1 N to 10.0 N) along a circular track on a turntable running at (5±1) r/min. After 24 h the marks are assessed visually in the 8 viewing slots of an opaque template, inside a viewing box fitted with a 70 W halogen lamp (1 200 lm, 2 800 K) and a matt black interior at an illuminance of 950±150 lx; the verdict is the minimum load at which continuous marks appear in at least 6 slots, and the result is quoted to 0.1 N. Conditioning requirements are the same for both methods — at least 1 week at (23±2) ℃ and (50±5)% RH — and some coating systems need longer curing time. The resolution of Method B (0.1 N) is far higher than that of a single linear pass, which makes it especially sensitive to the hairline marks on high-gloss clear coats and soft-touch films and well suited to formulation screening; Method A agrees with the national standard and suits acceptance testing and trade hand-over.
| Comparison item | GB/T 4893.10-2024 | EN 15186 Method A | EN 15186 Method B |
|---|---|---|---|
| Scratch head geometry | Diamond conical head R=(0.30±0.01) mm, α=(60.0±1.0)° | Conical diamond head 0.30±0.01 mm, 60±1° | Hemispherical diamond head 0.090±0.003 mm, 90±1° |
| Load range | 1.0 N to 20.0 N | 1 N to 20 N | 0.1 N to 10.0 N |
| Loading mode | Progressive, increment 1.0±0.1 N | Progressive, 1 N steps | Decreasing load along a circular track |
| Track | Straight line, length ≥22 mm | Straight line, non-manual motion | Turntable at (5±1) r/min |
| Criterion | Scratch width ≥0.30 mm | Mark width ≥0.30 mm | Continuous visible marks in at least 6 of 8 slots |
| Result resolution | 1.0 N | 1 N | 0.1 N |
| Conditioning | (23±2) ℃, (50±5)% RH, ≥48 h | ≥1 week in the same atmosphere | ≥1 week in the same atmosphere, assessed 24 h after testing |
| Excluded objects | Leather and textile surfaces | Melamine-faced panels, HPL | Leather and textile coverings |
| Typical use | Acceptance of finished furniture and test panels in China | Penetrating-scratch acceptance for export to Europe | Formulation screening; hairline marks on high-gloss and soft-touch films |
On the coatings side there is a further group of coating-film scratch resistance methods that must be told apart. ISO 1518-1:2023 is the constant-loading method: it can be used as a pass/fail test at one specified load, or with a progressive load to determine the minimum load at which the coating is scratched through to the substrate, or to an intermediate layer in a multi-layer system. ISO 1518-2:2019 uses a sharp-edged scratch head with continuously increasing load and is intended mainly for comparing differences between panels in a batch. ISO 12137 specifies the method with a curved-surface scratch head. The official abstracts of all three standards state that the choice of method depends on the specific problem to be solved, and that no one of them can simply be called “more accurate”. The furniture industry habitually mixes EN 15186, a furniture-side test, with ISO 1518, a coatings-side test, so any technical agreement must state the standard number and edition.
IV. Abrasion resistance: how the criteria changed after GB/T 4893.8 was revised
1. The 2013 edition: rubber abrasion wheels plus a wear grade scale
GB/T 4893.8-2013 addressed the coating film on the wooden components of furniture. It used a film abrasion tester with nitrile rubber abrasion wheels (hardness (60±5) IRHD, 100# abrasive, diameter (50±0.5) mm, thickness (12±0.5) mm), a turntable speed of (60±2) r/min and a (1±0.01) kg weight on the loading arm. A preliminary run of 50 r produced a flat, even wear ring, after which testing continued to the agreed number of abrasion revolutions (the recommended series covers 200, 300, 400, 500, 1 000, 2 000, 3 000, 4 000, 5 000, 8 000 and 10 000 r) until the end point, and the result was graded from Grade 1 (no whitening) to Grade 5 (severe wear-through to the substrate) according to the degree of film damage. After application, specimens were stored for 7 d in circulating air at a temperature not lower than 15 ℃ before testing, and were pre-conditioned for 24 h at (20±2) ℃ and 60% to 70% relative humidity. Abrasion wheels were not to be changed during the test and the dust extraction device had to be running.
2. The 2023 edition: switched to a gravimetric method with a wider scope
GB/T 4893.8-2023, Furniture — Determination of physical and chemical properties of surface — Part 8: Method for the determination of abrasion resistance, was issued on 2023-09-07, implemented on 2024-04-01 and fully replaces the 2013 edition; technically it is based on the modified adoption of ISO 4211-5:2021, Furniture — Tests for surface finishes — Part 5: Assessment of resistance to abrasion. The revised clauses extend the scope from “coating film on wooden components” to foil finishes, laminates (including high-pressure decorative laminates HPL of thermosetting resin-impregnated paper), resin-impregnated paper-finished panels, and pigmented and transparent clear coat surfaces, and the instrument list correspondingly includes an abrasion tester, calibration panels, sandpaper strips, a balance and a constant temperature and humidity chamber — that is, abrasion resistance is expressed as the mass difference before and after abrasion, and calibration panels allow a consistency check of the whole system. Testing can be carried out either on unused components of finished furniture or on panels of the same material and process whose dimensions meet the requirement. The most common error when dealing with customers is mixing up the editions: the 2013 edition reports a grade, the 2023 edition reports abrasion loss, and the two reports cannot be accepted in each other’s place.
| Comparison item | GB/T 4893.8-2013 | GB/T 4893.8-2023 (current) |
|---|---|---|
| Effective date | Issued in 2013 (now superseded) | Issued 2023-09-07, implemented 2024-04-01 |
| Adoption basis | In-house industry method | Modified adoption of ISO 4211-5:2021 (MOD) |
| Scope | Coating film on the wooden components of furniture | Foil finishes, laminates, resin-impregnated paper-finished panels, pigmented and clear coat surfaces |
| Abrasive | Nitrile rubber wheels, (60±5) IRHD, 100# abrasive, Φ(50±0.5) mm × (12±0.5) mm | Sandpaper strips (used with the abrasion tester) |
| Load and speed | (1±0.01) kg weight, turntable (60±2) r/min | Run to the method parameters of ISO 4211-5 |
| Result expression | Grade 1 to Grade 5 (by area of whitening and wear-through) | Abrasion loss as the primary figure, supported by visual records |
| Consistency check | No calibration requirement | Calibration panels provided |
| Typical agreed threshold | Purchase specifications often state “1 000 r ≥ Grade 3” | Must be re-expressed as abrasion loss; do not carry over the old threshold |
At the measurement level, one example published by a third-party laboratory for a solid-wood table coating tested at a 500 g load with CS-10 wheels over 1 000 r gave parallel-specimen abrasion loss between 176.98 mg/100 r and 181.54 mg/100 r, a range of 4.56 mg/100 r and an expanded uncertainty U=3.03 mg/100 r (k=2). These are illustrative data given by that body under its own published basis and are not guaranteed measured values from our factory. Their practical meaning lies in the dispersion: for products from a stable process the range between parallel specimens is kept within 2.5%; conversely, when the range widens, what is usually exposed first is wheel wear or a swing in the application process rather than “the formulation has deteriorated”. The two concepts of abrasion loss and mass loss must also be separated — the first is the loss of film material per unit of revolutions, while the second can be disturbed by moisture uptake and dust adhesion, so the report should state the basis on which weighing and calculation were done. Abrasion resistance is not collinear with chemical or stain resistance; the formulation-side reading of those properties is covered in our related article on this site, Furniture coating stain and chemical resistance: test methods and formulation logic.
V. Why a coating film is damaged by scratching: hardness, modulus, toughness and the rebound window
1. Pendulum, pencil and stylus measure three different things
None of the three “hard” indicators most used in the industry can directly replace scratch resistance. Pendulum damping hardness (methods such as ISO 1522 and GB/T 1730) measures elastic energy dissipation in the film and is sensitive to crosslink density and degree of cure. Pencil hardness (methods such as ISO 15184 and GB/T 6739, graded from 6B to 9H) measures the resistance of the coating to being scratched or indented by a pencil lead, on a scale of tens of micrometres at the very surface. The scratch stylus load measures the stress needed to displace and cut through the material under a specific tip geometry, and it is controlled very strongly by the tip radius. Our related article on this site, Coating deformation test criteria: cupping, cylindrical mandrel bend and pendulum damping hardness, covers acceptance of deformation and cohesion; the scratch criteria in this article are complementary to it — one asks whether the film can be stretched without cracking, the other whether it can be pushed without sinking. In engineering practice the three sets of data must be read together, so that a self-check sheet showing pencil 2 H is never used to answer a customer’s scratch complaint.
2. Viscoelasticity and the rebound window: why width is measured only after 24 h
Wood clear coat is a typical viscoelastic material. At the instant the stylus passes, material is pushed aside and ridges form on both flanks of the groove; over time part of the ridge rebounds, the groove narrows, but whitening (micro-voids) may remain. Both GB/T 4893.10-2024 and EN 15186 Method B require the scratch to rest for 24 h before assessment precisely in order to fix this rebound process — measuring width too early underestimates the residual mark. The glass transition temperature (Tg) and the crosslink density decide how fast the rebound is: acrylic or polyurethane systems with a low Tg and mobile chain segments can partly back-fill shallow marks at room temperature or under mild heating, whereas highly crosslinked UV systems have little rebound margin, so once the film is cut through the mark is permanent. Hardness development and pot-life control in two-component polyurethane furniture coatings are covered in our related article on this site, Two-component polyurethane furniture coatings: NCO/OH ratio, pot life and hardness development, and thick-build PE unsaturated polyester systems in PE unsaturated polyester furniture coatings: initiation and cure, thick flow coating and engineering limits — a thick build raises both the stylus penetration load and the abrasion margin, at the cost of shrinkage and interfacial risk.

VI. Matt and matting systems: the price of particle size, porosity and loading level
1. Matting works through microscopic roughness, not through the finest particle
The consensus in publicly available technical literature is that matting comes from microscopic roughness at the surface of the coating film: silica with too fine a particle size sinks with the resin during drying, the surface becomes flatter instead and gloss will not come down. The rule of thumb is that bringing 60° gloss down to about 30 usually takes a 3 μm to 5 μm matting agent, while getting below 5 often requires 8 μm and coarser. Fumed silica matting agents are mostly micron-scale granules agglomerated from nano-scale primary particles (bulk particle size commonly 2 μm to 10 μm, specific surface area up to 100 m²/g to 380 m²/g), and with a refractive index of about 1.46 they sit close to that of most resins, so the loss of transparency is limited. Matting efficiency also depends on porosity and on surface treatment: porosity is generally in the range of 60% to 80%, and higher porosity produces a more pronounced difference in volume shrinkage. Wax-treated grades feel smooth and resist scratching better, but their matting efficiency is lower. The same logic is used in our related article on this site, Matte gloss stability and matting agent settling control, to explain gloss drift; here it explains why a matt finish and scratch resistance are natural opponents.
2. Rigid particles cut the continuous phase; wax micropowders supply the lubricating layer
Silica is a rigid inorganic particle. Dispersed in the continuous phase of the film-forming resin it disrupts that continuity and lowers overall toughness and cohesion; under friction the particles become stress-concentration points and are the first to be pulled out, leaving pits, and the higher the loading level the more obvious the disruption. The mitigation route given in published formulation practice is a hard/soft matting blend: for semi-matt (60° gloss 10 to 30) the total matting component is about 3% to 5% of the mass of film-forming resin, with hard matting at 70% to 80% and soft matting (polyethylene wax micropowder, particle size 2 μm to 4 μm, loading 0.6% to 1.5%) at 20% to 30%; for full matt (60° gloss below 10) the total is 6% to 8%, with hard matting reduced to 50% to 60% and soft matting raised to 40% to 50%; and for furniture and flooring coatings with high abrasion demands a ternary blend of coarse hard matting, fine hard matting and soft matting is used (40% / 20% / 40%). In practice the soft matting agent is first pre-dispersed in a small amount of resin into a 10% to 20% dispersion and then blended with the hard matting, with the dispersion temperature held between 30 ℃ and 40 ℃ so that the wax does not melt and then agglomerate on cooling. Reference loading levels in most supplier technical data sheets fall between 3% and 15% (of the total formulation), with dispersion recommended at 1 000 r/min to 1 500 r/min for 10 min to 15 min, and a clear instruction not to grind or to mix at high speed for long periods, because that destroys matting efficiency. These ratios are published-literature and supplier-data-sheet figures, quoted to show the order of magnitude and the direction, and they are not guaranteed values for any specific batch.

VII. Film thickness, sealer and top-coat pairing and wood anisotropy: the physical ceiling of a load criterion
The coupling between stylus load and film thickness is direct: to cut a 0.30 mm wide track through a coating film, the thicker the film the greater the displacement and the load needed to penetrate to the interface; conversely, with a thin film a “high load” often says only something about the modulus of the resin itself, not about the resistance of the whole system. Coating film thickness is measured to GB/T 4893.5-2013, Furniture — Determination of physical and chemical properties of surface coating — Part 5: Method for the determination of thickness. Furniture top coats are commonly applied at film thicknesses of a few tens of micrometres, and on open-grain woods (oak vessels, for example) the result differs markedly depending on whether the tip lands on the edge of a pore or on solid film — the interference of pore filling, filler type and sanding schedule with the criterion is covered in our related article on this site, Wood coating sanding practice: grit grading and intercoat sanding control. On the wood side, anisotropy and moisture content are further variables: late wood and early wood differ in hardness along and across the grain, and the standard allows scratches to be made along the grain direction “where applicable”, but the report must state the direction. A deviation of moisture content from the equilibrium moisture content changes both the support stiffness of the substrate and the internal stress in the coating film; the related basis is given in Wood moisture content and furniture coating: equilibrium moisture content, gradient control and defect prevention. In addition, soft-touch and excimer systems carry their surface structure into sub-micron fold textures, where a scratch is more likely to show up as a gloss change — texture ironed flat — than as a measurable width; for such systems it is advisable to report both a Method B result and a Method A result measured 24 h after rebound. The mechanism and the energy window are covered in Excimer UV-cured soft-touch wood coatings: 254 nm surface texturing, energy window and gloss block-back verification.
VIII. Key data and criteria quick reference (with units)
- Acceptance threshold: scratch width ≥0.30 mm; width measurement equipment accuracy ±0.05 mm; stylus inspection accuracy ±0.01 mm (GB/T 4893.10-2024).
- Stylus geometry: conical head radius R=(0.30±0.01) mm, cone angle α=(60.0±1.0)°; ring-method hemispherical head radius (0.090±0.003) mm, apex angle (90±1)° (EN 15186).
- Loads: the national standard and European Method A use 1.0 N to 20.0 N with steps of 1.0±0.1 N; Method B uses 0.1 N to 10.0 N, with results quoted to 0.1 N.
- Motion parameters: linear speed (20±2) mm/s, travel length ≥22 mm; Method B turntable (5±1) r/min.
- Environment and timing: (23±2) ℃, (50±5)% RH; pre-conditioning ≥48 h, panel conditioning ≥1 week, width measured after 24 h rest following scratching.
- Abrasion resistance (2013 edition): turntable (60±2) r/min, weight (1±0.01) kg, rubber wheel hardness (60±5) IRHD, 100# abrasive, preliminary 50 r, recommended revolutions covering 200 r to 10 000 r.
- Abrasion resistance (third-party published example): 500 g load, CS-10 wheels, 1 000 r; parallel specimens 176.98 mg/100 r to 181.54 mg/100 r, range 4.56 mg/100 r, U=3.03 mg/100 r (k=2).
- Published matting system figures: semi-matt total loading 3% to 5%, full matt 6% to 8%; supplier data-sheet reference loading 3% to 15%; dispersion at 1 000 r/min to 1 500 r/min for 10 min to 15 min, 30 ℃ to 40 ℃.
IX. Writing the criteria into a technical agreement: 6 clauses for acceptance and quality control
1. Fix the method and the edition before the threshold
The agreement must lock four items clause by clause: the test method standard and its edition (GB/T 4893.10-2024 or EN 15186 Method A/B, stating whether ISO 1518-1 or 1518-2 applies), the measured quantity (minimum load in N, abrasion revolutions in r, or abrasion loss in mg/100 r), the origin of the specimen (cut from the finished product or a panel made with the same process), and the conditioning points (48 h, 1 week, 24 h after scratching). Writing only “good scratch resistance” or “abrasion resistance ≥ a certain grade” without fixing the edition will almost certainly produce a dispute at acceptance, above all because the way results are expressed changed between the 2013 and the 2023 edition of GB/T 4893.8. Supplier and buyer should also confirm in the agreement the scratch direction (along or across the grain) and whether a record of the threshold not being reached at 20.0 N is acceptable.
2. Hold the criteria with four formulation and process factors
What keeps the load and the abrasion loss stable at the same time are four controllable factors: the soft/hard matting ratio and the particle-size grading; the dry film thickness of the top coat and its uniformity (together with sealer sealing and pore filling); the degree of curing and crosslinking (UV energy, PU ratio and open time); and the sanding schedule and intercoat cleanliness. A drift in any one of them can move the load reading by 2 N to 3 N, while the resolution of the method itself is only 1.0 N. For outgoing inspection, a fast pass/fail check at a single fixed load is recommended (the same idea as the pass/fail use of ISO 1518-1), for instance agreeing 6.0 N or 8.0 N as the threshold, and keeping batch dispersion monitoring separate from third-party progressive-load reports; at the same time the incoming substrate inspection related to Wood moisture content and furniture coating: equilibrium moisture content, gradient control and defect prevention should be retained, so that swings in substrate moisture content do not make the coating film criteria incomparable.
X. Frequently asked questions (FAQ)
1. A customer asks “is this lacquer scratch resistant?” — which number should I answer with?
Ask about the damage scenario first, then choose the method. For sharp localised contact such as keys, cutlery or pet claws, report the minimum load in N under GB/T 4893.10-2024 (or EN 15186 Method A), stating the threshold width of 0.30 mm, the maximum load of 20.0 N and the method resolution of 1.0 N. For loss of gloss and wear-through caused by cleaning wipes and objects shifted repeatedly, report abrasion loss or the wear grade under GB/T 4893.8-2023 (the 2013 edition may still appear in older agreements). The two numbers are each valid on their own terms, cannot be converted into each other, and should not be replaced by pencil hardness or pendulum hardness — the tip geometry and load conditions of those methods are completely different from scratching, and they cannot answer the question about the customer’s actual service condition.
2. Two runs on the same panel gave 6.0 N and 8.0 N — is the instrument broken?
Not necessarily. The usual factors that affect the reading, in order of weight, are stylus tip wear (replace it once the radius is outside 0.30±0.01 mm), conditioning time and environment (less than 48 h, or not at (23±2) ℃ and (50±5)% RH), whether the scratch landed on a wood pore or a sanding defect, whether it ran along the grain, and whether the second and third surfaces followed the rule of starting 3.0 N below the first result. In addition, the standard itself quotes results to 1.0 N and requires the average of 3 test surfaces, so a difference at the 2 N level lies within the dispersion the method allows. The recommendation is to average 3 surfaces as the standard requires, fix the grain direction, verify stylus geometry every day, and then run an instrument-to-instrument comparison on the same panel.
3. Is Method B (ring test) stricter than Method A?
The two are not a loose-versus-tight relationship; they differ in sensitivity and in object. Method B has a tip radius of only 0.090 mm, starts loading at 0.1 N and quotes results to 0.1 N, and is designed to capture the “first visible mark”, including hairline marks that show as a change of gloss only; Method A uses a tip radius of 0.30 mm with a threshold of ≥0.30 mm width and is closer to the acceptance logic for penetrating and deformable scratches. On high-gloss clear coats and soft-touch films the Method B reading appears earlier, which makes it useful for formulation screening and additive comparison, whereas for trade hand-over and finished-goods acceptance Method A (and GB/T 4893.10, which is consistent with it) maps more easily onto contract clauses. Using the two together is more valuable than letting one replace the other.
4. If I take gloss from 10 down to 5, how much scratch resistance will I lose?
The direction is clear; the magnitude depends on the system. On published figures, holding 60° gloss reliably below 5 usually needs matting agent of 8 μm and coarser with a total loading that commonly reaches 6% to 8% of the resin mass; as the volume fraction of rigid particles rises, the continuous phase becomes less continuous and the stress-concentration points multiply, so the visibility of shallow scratches (the Method B reading) usually deteriorates first, followed by the penetration load (the Method A or national standard reading). Workable compensation includes hard/soft matting blends (raising soft matting to 40% to 50% in a full matt system), bimodal particle-size grading (coarse particles to build roughness, fine ones to fill the gaps), and wax-treated silica or polyethylene/polytetrafluoroethylene composite wax micropowders to form a lubricating layer at the surface. All magnitudes should be confirmed by comparative testing in your own system; published ratios indicate direction only.
5. Can the matting agent be milled to a finer dispersion?
No. Most supplier technical data sheets explicitly advise against grinding or prolonged high-speed mixing. The reason is that silica matting particles work through their granulated bulk particle size and pore structure, which create the microscopic roughness at the surface of the coating film; milling shatters the particles and collapses the pores, matting efficiency falls sharply, and settling or coarsening becomes more likely. The recommended practice is medium-to-high speed stirring dispersion, commonly at 1 000 r/min to 1 500 r/min for 10 min to 15 min with the temperature held between 30 ℃ and 40 ℃; wax-treated grades can first be pre-dispersed with resin into a 10% to 20% master batch and then blended in. If agglomeration is caused by insufficient fineness, switch to a grade with a narrower particle size distribution or add an anti-settling system instead of trying to solve it by milling.
6. Does a thicker film always mean better scratch resistance?
Film thickness raises the displacement and the load needed to cut through to the interface, but only on condition that cohesion within the film and adhesion at the interface keep up. Thick-build systems (PE unsaturated polyester flow coating, thick UV builds) show clear gains in the stylus reading, yet where curing is insufficient, intercoat adhesion is weak or shrinkage stress is high, the scratch propagates along the interface and may even delaminate in sheets, and abrasion testing then shows wear-through earlier. Engineering judgement should read thickness together with adhesion (GB/T 4893.4-2013 cross-cut method), intercoat sanding and cure parameters: looking at thickness alone merely postpones the problem to the customer. Our related articles on this site, PE unsaturated polyester furniture coatings: initiation and cure, thick flow coating and engineering limits and Two-component polyurethane furniture coatings: NCO/OH ratio, pot life and hardness development, set out the boundary conditions for thick builds and crosslinking control.
7. My customer in Europe works to EN 15186 and the domestic one to GB/T 4893.10 — do I have to issue two reports?
One test with two sets of records is better than two reports that cite each other. The two methods differ in tip geometry (conical 0.30 mm versus hemispherical 0.090 mm), load range (1.0 N to 20.0 N versus 0.1 N to 10.0 N), criterion (width ≥0.30 mm versus visible marks in at least 6 of 8 slots), result resolution (1.0 N versus 0.1 N) and conditioning time (≥48 h versus ≥1 week), and mixing any of these makes the readings lose comparability. The practical approach is to prepare and condition panels from the same batch separately to each standard, and to state in the report the standard number and edition, the scratch direction, the origin of the specimen and any deviations. EN 15186 Method A is not applicable to melamine-faced panels and HPL, so for those surfaces a board-side method must be used instead (such as the 1.5 N and 2.5 N two-level decorative-overlay criteria of GB/T 17657-2022), and the reason should be recorded in the technical documentation.
8. Scratches have already appeared at the customer’s — can only the affected area be recoated?
It can be done, but acceptance should be judged on system consistency, not on whether it looks the same. The success of a local repair depends on how clean and how de-glossed the old film surface is (grit schedule in Wood coating sanding practice: grit grading and intercoat sanding control), the time boundary of the recoat window (recoat and anti-blocking conditions for waterborne top coats are covered in a separate article on this site), and the consistency of gloss and texture in the repaired zone (a local repair on a matt film very easily leaves bright spots and cloudy boundaries). After the repair, a pass/fail quick check at the same single fixed load, compared against the outgoing records, is recommended; where the repaired area covers more than a small part of the visible face or sits in a high-gloss zone, recoating the whole panel is the safer choice.
References and explanation of the data basis
- GB/T 4893.10-2024, Furniture — Determination of physical and chemical properties of coating film — Part 10: Method for the determination of scratch resistance, issued 2024-09-29, implemented 2025-04-01, administered by the National Furniture Standardization Technical Committee (SAC/TC 480) and proposed by the China National Light Industry Council; the statements in this article on tip geometry, load and speed, 48 h pre-conditioning, 24 h rest, the 3 test surfaces and results quoted to 1.0 N are taken from the published text of that standard and from the project notice on the national public service platform for standards information.
- GB/T 4893.8-2023, Furniture — Determination of physical and chemical properties of surface — Part 8: Method for the determination of abrasion resistance, issued 2023-09-07, implemented 2024-04-01, fully replacing GB/T 4893.8-2013, modified adoption of ISO 4211-5:2021 “Furniture — Tests for surface finishes — Part 5: Assessment of resistance to abrasion”; the rubber wheel, rotational speed, weight and grading practice of the 2013 edition are taken from published standard abstracts and the public material of testing bodies.
- The other parts of the GB/T 4893 series: Part 1 resistance to cold liquids (2021 edition), Part 2 resistance to damp heat (2020 edition), Part 3 resistance to dry heat (2020 edition), Part 4 adhesion cross-cut (2013 edition), Part 5 thickness (2013 edition), Part 6 gloss (2013 edition), Part 7 resistance to temperature cycling (2013 edition), Part 9 impact resistance (2013 edition).
- EN 15186 (including the DIN EN 15186:2022 and EN 15186:2024 editions), “Furniture — Assessment of the surface resistance to scratching”; the tip, load, criterion and viewing box parameters of Method A linear and Method B ring tests are taken from published introductions to the method and the public notes of testing bodies, and the reference relationship of this method also appears in the project notice for GB/T 4893.10.
- ISO 1518-1:2023 “Paints and varnishes — Determination of scratch resistance — Part 1: Constant-loading method”, ISO 1518-2:2019 (progressive-loading method) and ISO 12137 (curved-surface scratch head method); scope and differences are taken from the published abstracts of the International Organization for Standardization; ISO 15184 is the pencil hardness method.
- The two-level 1.5 N and 2.5 N scratch load criteria for decorative overlays in GB/T 17657-2022, Methods of testing the physical and mechanical properties of wood-based panels and surfaced wood-based panels, together with the application boundaries of EN 14322 (melamine-faced) and EN 438-1 (HPL), are taken from published standard introductions.
- The list of surface physical and chemical property items in GB/T 3324, General technical specifications for wooden furniture (the 2017 edition implemented from 2018-05-01, the 2024 edition implemented from 2025-05-01 replacing the 2017 edition), is taken from published introductions to the standard and examples of purchase specifications; thresholds of the “1 000 r ≥ Grade 3” type are purchase-document practice, not a unified requirement of the standard.
- Matting agent particle size, porosity, hard/soft blending ratios and dispersion process parameters are taken from chemical material supplier technical data sheets and published technical articles; they belong to the “public-literature basis / supplier data-sheet basis” and are used to explain mechanism and order of magnitude, not as guaranteed measured values from our factory; the third-party laboratory example (176.98 mg/100 r to 181.54 mg/100 r, U=3.03 mg/100 r, k=2) is an instance published by that body under its own stated basis.
- Basis of data: the figures in this article come from three kinds of source — standard method clauses, published textbooks and technical articles, and supplier technical data sheets — and their purpose is to explain mechanism and order of magnitude; judgement for a specific product follows the contract appendix, the test report shipped with the goods and the official text of the standard. The scope of this article is limited to B2B technical and procurement settings in the furniture and coatings chain, and only EXW and FOB delivery terms apply.
Last updated: 2026-11-16
Kexin New Materials (Guangdong) Co., Ltd. This article is written for B2B technical and procurement readers in the furniture and coatings chain, as a reference for formulation, process and acceptance practice; the delivery terms applicable to supply are EXW / FOB.