Epoxy MIO intermediate coat Epoxy MIO Intermediate
Two-component epoxy polyamide/micaceous iron oxide high-build intermediate paint — MIO labyrinth effect physical barrier
Epoxy MIO intermediate coat(Epoxy MIO Intermediate)is a high-performance two-component (2K) anticorrosive primer, in which epoxy resin cured with a polyamide hardener acts as the film-former and ultrafine zinc powder (dry-film content ≥70%) is the principal anti-corrosive pigment.The coating provides active corrosion protection through the sacrificial-anode cathodic-protection action of the zinc on the steel; even where the dry film is locally damaged, the surrounding zinc powder continues to give the exposed steel electrochemical protection.CompliesHG/T 3668-2020《Epoxy MIO intermediate coat》Type 2 standard; when combined with an epoxy micaceous-iron-oxide intermediate coat and a polyurethane / fluorocarbon topcoat, the system withstands a neutral salt spray ≥1000 h, meeting the C4-C5 high-corrosivity environment class requirements of ISO 12944.It is widely used as the anticorrosive primer in major projects such as sea-crossing bridges, offshore oil platforms, petrochemical storage tanks, transmission towers, wind-turbine towers, and large steel-structure buildings.
ProductsOverview
Product overview: who is it for? what problem does it solve?
Epoxy MIO intermediate paint is a heavy-duty anticorrosive primer designed for steel structures requiring long-term anticorrosive protection of over 15 years in C4-C5 highly corrosive environments.The core problem it solves is: ordinary anti-rust paints fail within 3-5 years in harsh environments such as coastal areas, chemical atmospheres, and high humidity, whereas epoxy MIO intermediate paint, through the dual mechanism of "cathodic protection + barrier protection", can provide 15-25 years of long-term protection when combined with intermediate paint and topcoat — greatly reducing whole-life-cycle maintenance costs.
Product definition
Epoxy MIO Intermediate, Chinese standard number HG/T 3668-2020, is a two-component (2K) ambient-temperature crosslinking-curing anticorrosive primer that uses epoxy resin (bisphenol A type, CAS 25068-38-6) and polyamide curing agent (CAS 68410-23-1) as film-forming substances, ultrafine spherical zinc powder (CAS 7440-66-6, particle size 3-8μm, mass fraction in dry film ≥70%) as anti-rust pigment, and xylene/n-butanol as solvent system.
Corrosion protection mechanism:High-content zinc powder particles in the coating form continuous conductive pathways between themselves and with the steel substrate. Since the standard electrode potential of zinc (-0.76V vs SHE) is lower than that of iron (-0.44V), zinc acts as the anode in corrosion microcells and preferentially undergoes oxidation (Zn → Zn²⁺ + 2e⁻). The released electrons flow through the conductive network to the steel surface, cathodically polarizing the steel below its immune potential—this is known as "sacrificial anode cathodic protection." Meanwhile, the corrosion products of zinc (ZnO, Zn(OH)₂, basic zinc carbonate, etc.) gradually fill the coating pores, forming a dense secondary barrier layer—the "corrosion product self-healing effect."
Key performance data:
- The dry film zinc powder content is ≥70% (compliant with HG/T 3668-2020 Category 2).
- Volume solids content ≥60% (ISO 3233:1998)
- Pull-off adhesion ≥6 MPa (ISO 4624:2016, test doll diameter 20mm)
- Single coating resistance to neutral salt spray (NSS) ≥400h (ISO 9227:2022, rust width at the crisscrossing ≤2mm)
- The complete system (epoxy zinc-rich 80μm + epoxy micaceous iron oxide intermediate coat 150μm + polyurethane topcoat 80μm) has an NSS resistance of ≥1000h.
- Mixed application period: 4-8 hours (23°C, main agent: curing agent = 10:1 w/w)
Suitable substrates and limitations:Applicable to carbon steel, low-alloy steel, and cast iron substrates blasted to Sa2.5 (ISO 8501-1:2007). Not recommended for direct application on galvanized steel (the passivation film on the zinc surface will block the conductive path—sweep blasting pretreatment or an epoxy primer transition layer is advised), stainless steel (the surface passivation film must be removed first), or aluminum alloy (risk of galvanic corrosion—the potential difference between zinc and aluminum is too large). Application temperature limits: standard type 5–40°C (below 5°C, the epoxy-amine crosslinking reaction rate is extremely low, resulting in incomplete coating curing).
Industry standing and applications:Epoxy MIO intermediate coatis one of the most widely used primer types in global heavy-duty anticorrosive coating systems (ISO 12944-5:2019 systems A2.08/A3.08/A4.08, etc.), forming a classic triple-protection system with epoxy MIO intermediate coat and PU/fluorocarbon/polysiloxane topcoat. Typical applications include: Akashi Kaikyo Bridge Japan (opened 1998, 100-year design life), Hong Kong-Zhuhai-Macao Bridge (opened 2018, 500,000m² steel box girders), North Sea offshore oil platforms (NORSOK M-501 system certification), etc. According to Grand View Research, the global zinc-rich primer market was approximately USD 2.8 billion in 2023, with Asia-Pacific accounting for 48% share.
ProductsFeatures
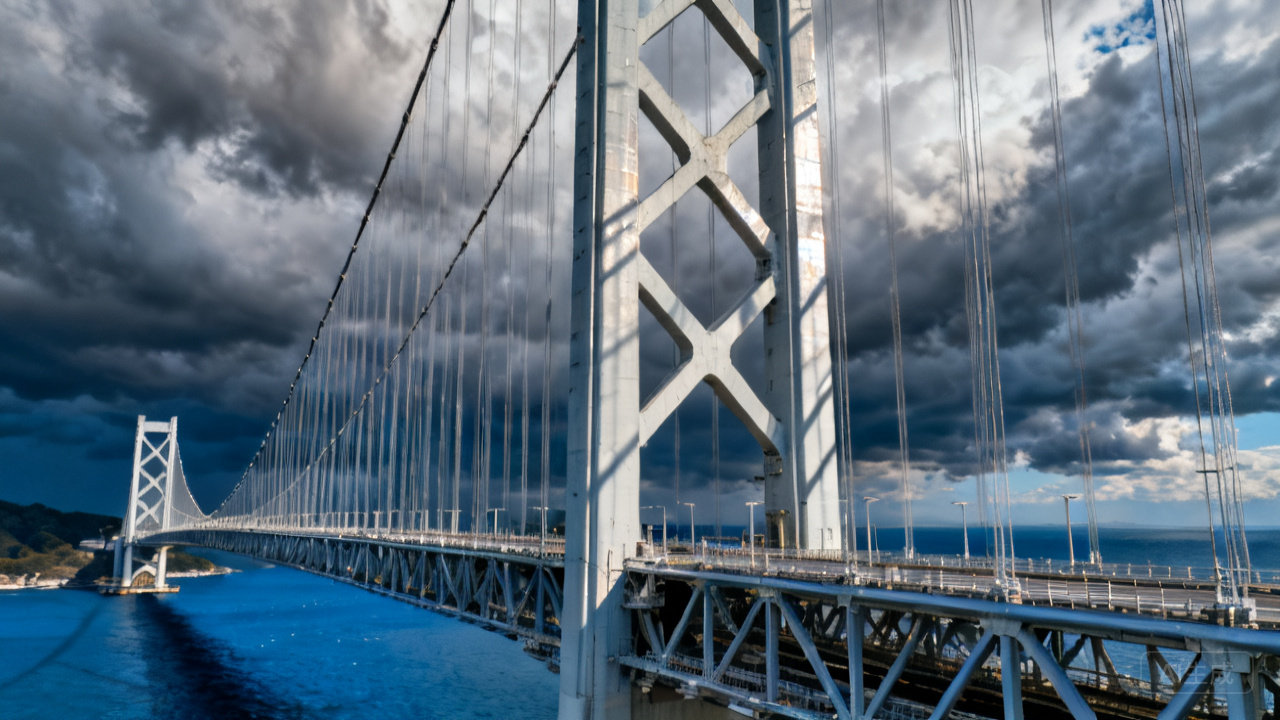
1. Cathodic protection (sacrificial anode) mechanism
The dry film of the coating contains ≥70% zinc powder, forming a continuous conductive network. The standard electrode potential of zinc (-0.76V) is lower than that of iron (-0.44V). When corrosion occurs, zinc preferentially oxidizes (Zn→Zn²⁺+2e⁻), releasing electrons that cathodically polarize the steel to its immunity potential — even if the coating has 3-5mm damage, the surrounding zinc powder can still provide continuous electrochemical protection for the exposed steel, which makes the anticorrosive performance of epoxy MIO intermediate paint far superior to ordinary anti-rust primers that rely only on physical barrier.
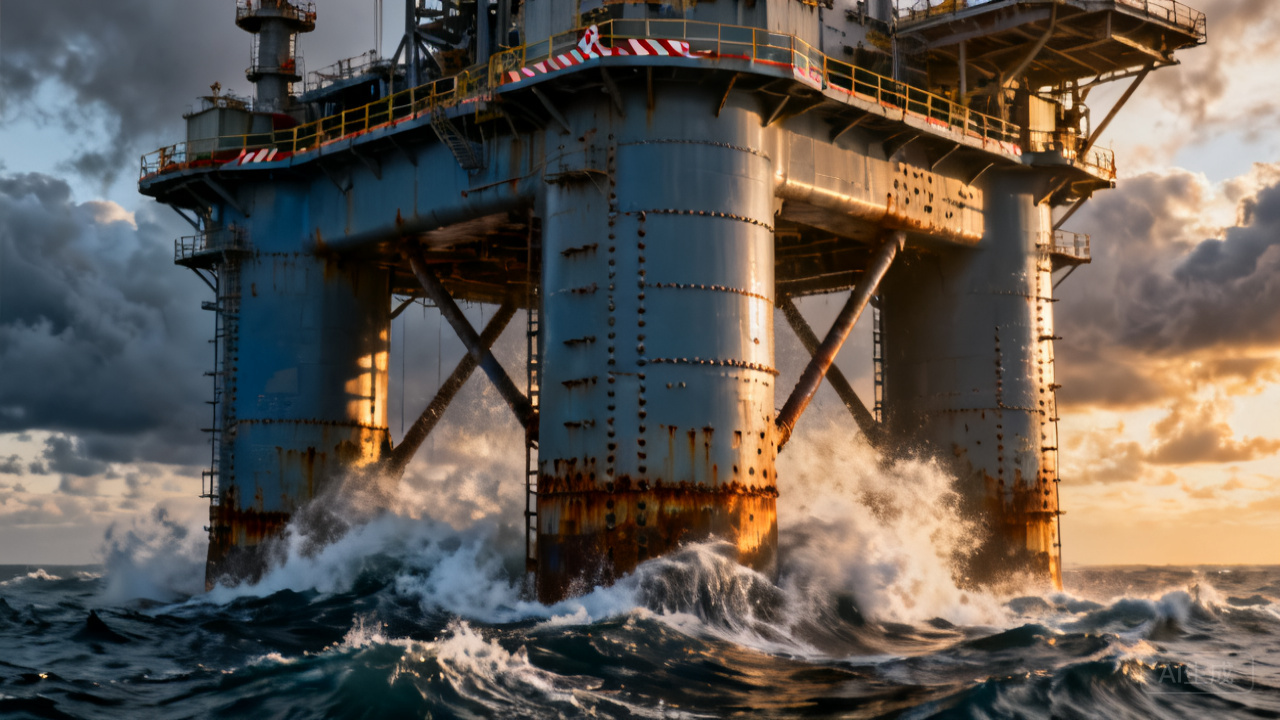
2. Superior corrosion resistance and durability
Single coating NSS≥400h (HG/T 3668 Class 2), and the system with epoxy MIO intermediate paint + polyurethane topcoat achieves NSS≥1000h. Under the C5-M extremely high corrosion environment (marine splash zone) of ISO 12944-2, the design service life is 15-25 years. The Akashi Kaikyo Bridge in Japan adopted an epoxy MIO intermediate paint system in 1998, and the coating remains intact after more than 25 years — the actual service life far exceeds the design value.
3. Excellent compatibility
It has excellent intercoat adhesion (pull-off method ≥5MPa) with epoxy MIO intermediate paint (MIO barrier layer), polyurethane topcoat (weather-resistant decorative layer), fluorocarbon topcoat (ultra-weather-resistant ≥25 years), and polysiloxane topcoat (high weather resistance + high chemical resistance). Epoxy MIO intermediate paint + epoxy MIO intermediate paint + topcoat is the most classic three-coat heavy-duty anticorrosion system in ISO 12944-5 — the primer provides cathodic protection, the intermediate paint provides thickness and physical barrier, and the topcoat provides weather resistance and decoration.
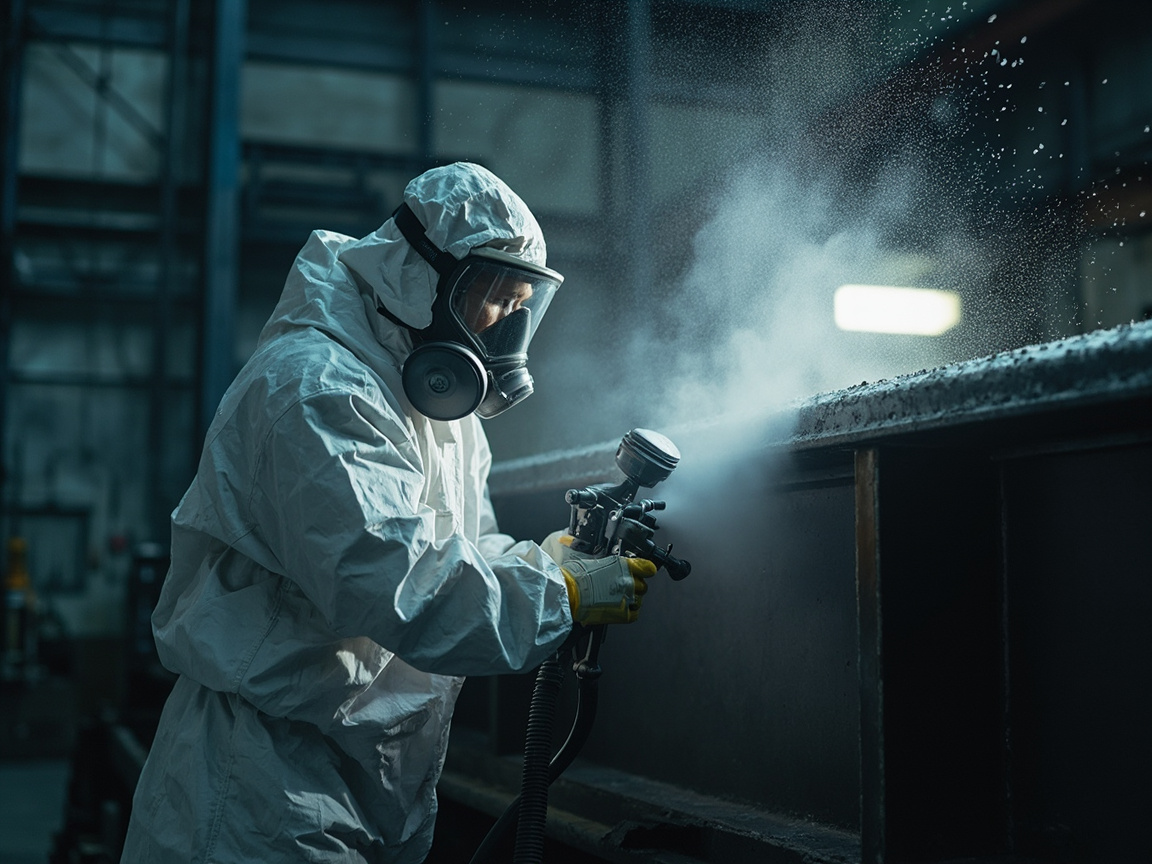
4. Wide adaptability to construction
Supports airless spray (nozzle 0.43–0.53 mm, 15–25 MPa), air spray, and brush/roller application (for small-area touch-ups). Single-pass dry film thickness: 60–80 μm. Mixing ratio: 10:1 (w/w). Pot life: 4–8 h (23°C). Wide temperature range for application (5–40°C); low-temperature formulation can be applied down to –5°C. Continuous stirring is required during spraying to prevent zinc powder sedimentation—use of a pressure pot with a pneumatic agitator is recommended to ensure coating uniformity.
5. Shop Primer Solderability
Specialized formulation (dry film 15-25μm) can be used as a shop primer—after application in the steel structure prefabrication plant, the steel remains suitable for welding and cutting. Welding fumes comply with occupational exposure limits (GBZ 2.1-2019), and the pass rate of X-ray inspection of welds is not affected. Suitable for automated spray painting on steel structure production lines—parts can be handled and stacked within 3-5 minutes after spraying. Note: Only the specialized shop primer formulation is weldable—the standard type with a dry film thickness of 60-80μm is not suitable for welding.
6. Environmental Compliance · Global Standards
Complies with HG/T 3668-2020 (China) Standard Class 2, ISO 12944-5:2019 system numbers A2.08/A3.08/A4.08, NORSOK M-501:2022 (Norwegian Petroleum Industry) System 1, SSPC Paint 20 (USA) Zinc-rich Primer Type II (≥77% zinc powder). VOCs<420g/L(GB 30981-2020),可passedROHS 2011/65/EU和REACH (EC) 1907/2006ComplianceTesting。Products碳足迹约2.8kg CO₂e/kg(摇篮到大门,SimaPro 9.5计算)——低于Inorganic zinc-rich primer(3.5kg CO₂e/kg)。
TechnicalParameters
Physicochemical parameters
Drying and performance
• March 2024, National Coatings Quality Inspection and Testing Center Test Report (No.: NTC-2024-0315-ZR)
· HG/T 3668-2020 "Epoxy MIO Intermediate Paint" Class 2 indicators
The data in this table are typical values under standard laboratory conditions (23±2°C, 50±5%RH). Actual values may vary slightly depending on the substrate condition, construction process, and environmental conditions. Please contact technical support to obtain the batch COA (Certificate of Appointment).
ApplicationProcess
Surface preparation
Sandblast to Sa2.5 (ISO 8501-1:2007), roughness Rz 40-75μm. Manual rust removal ≥ St3. Grease must be removed with SSPC-SP1 solvent. Primer application (RH) must be completed within 4 hours after sandblasting.<50%可延至8h)。禁忌:雨天/雾天/Substrate temperature低于露点3°C时禁止Application。
Mixing / compounding
Stir the main agent for 3-5 minutes until the zinc powder is completely and evenly dispersed. Add the curing agent at a ratio of 10:1 (w/w) and continue stirring for 3-5 minutes. Let it stand for 15-30 minutes (23°C) to mature. Continuously stir during application to prevent zinc powder from settling—a pneumatic mixer is recommended. The mixed usable period is 4-8 hours (23°C). Do not dilute and use materials that have gelled beyond this period.
Primer application
Airless spraying (recommended): Nozzle 0.43-0.53mm/0.017-0.021", pressure 15-25MPa. Air spraying: Nozzle 1.5-2.0mm, pressure 0.3-0.5MPa. Brush/roller coating is only suitable for small-area pre-coating and repair. Single-coat DFT 60-80μm. Pre-coat welds, free edges, etc.
Drying and recoating
Surface dry ≤ 1h (23°C), hard dry ≤ 24h. Minimum recoating interval 8h (23°C). Maximum recoating interval 7d—exceeding this interval requires sandblasting (low pressure 0.2-0.3MPa, non-metallic abrasive) to remove surface zinc salts (basic zinc carbonate). Matching: Epoxy micaceous iron oxide intermediate coat 100-150μm → Polyurethane/fluorocarbon topcoat 50-80μm × 2.
Inspection & acceptance
DFT measurement (ISO 2808:2019, SSPC-PA2): 80% of measuring points ≥ specified value, no measuring points<80%规定值。AdhesionTesting(ISO 4624 pull-off test或ISO 2409Cross-cut method)。pinhole detection(Wet sponge method,67.5V/90V)。Visual inspection:无Sagging/漏涂/起泡/缩孔/zinc powder不均匀。
ApplicationsField/Area
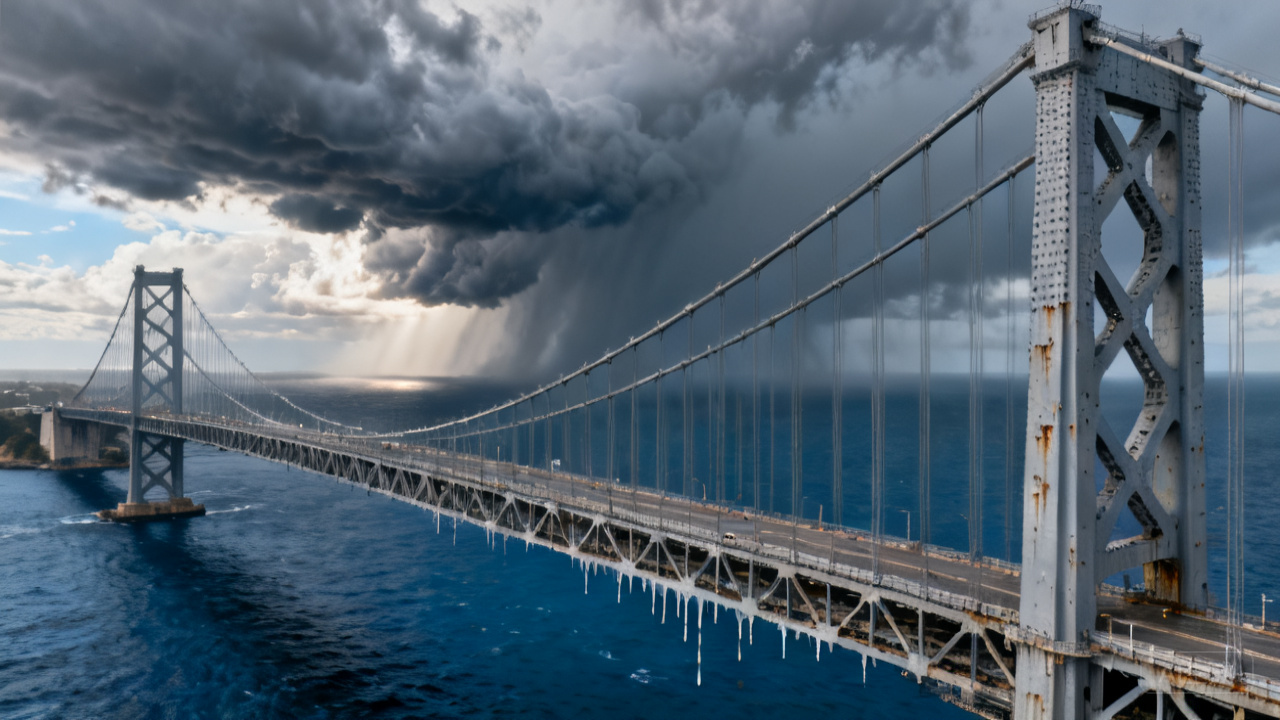
Sea-crossing / river-crossing bridges
Steel box girders, bridge towers, arch ribs
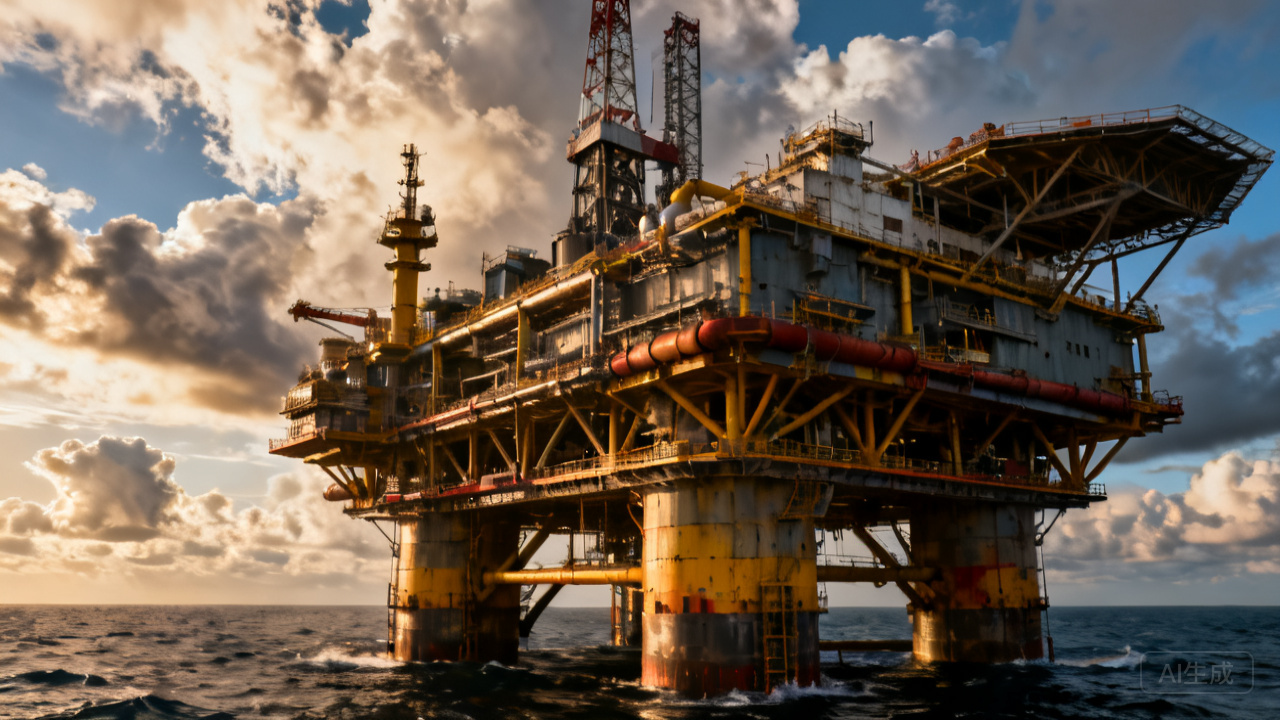
Offshore oil platforms
Jackets, decks, living quarters
Exterior walls of petrochemical storage tanks
Crude oil / refined products / chemical storage tanks
Transmission towers / tubular towers
Steel structures for high-voltage / ultra-high-voltage lines
Large steel structure plants
Industrial plants, sports venues
Port machinery
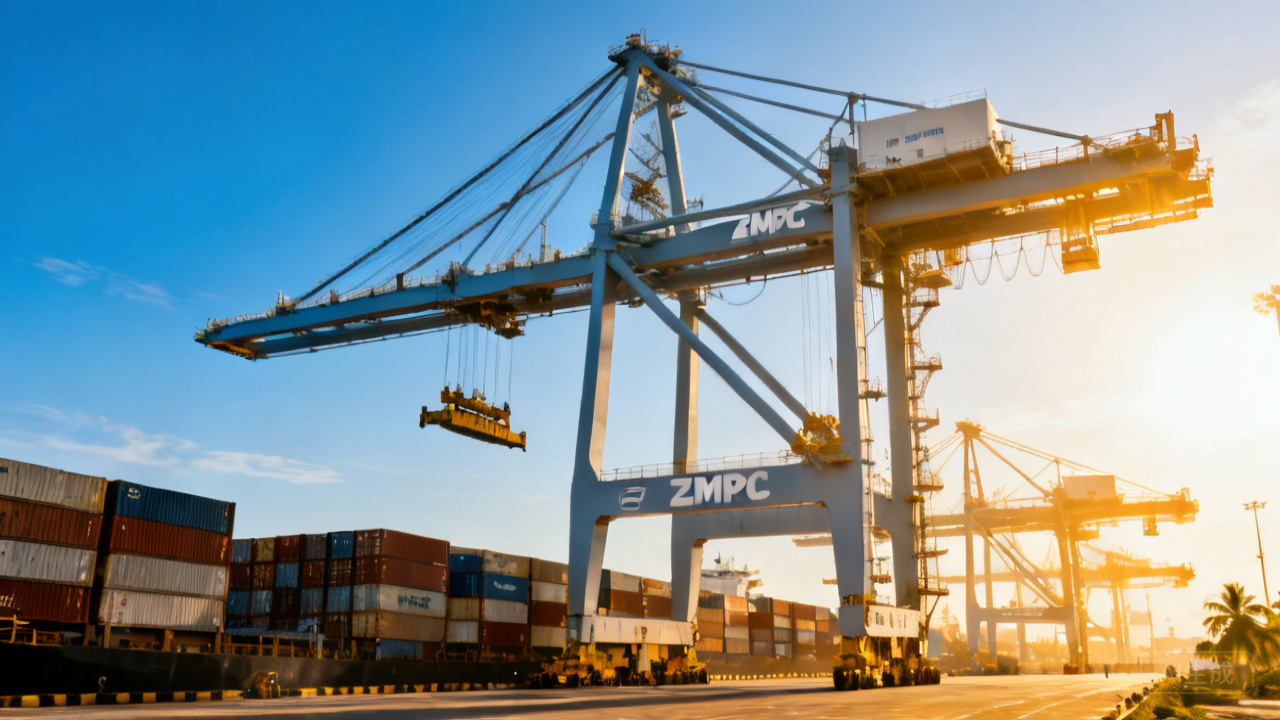
Ship-to-shore cranes, gantry cranes, ship unloaders
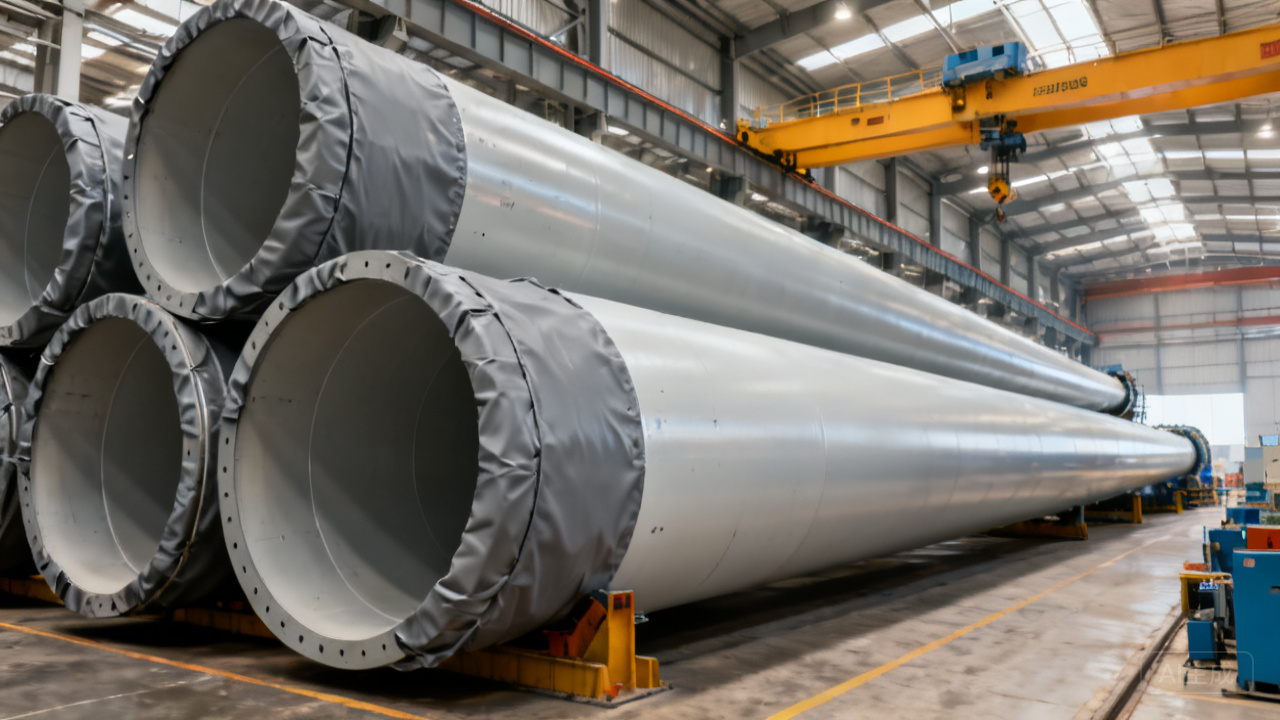
Wind turbine towers
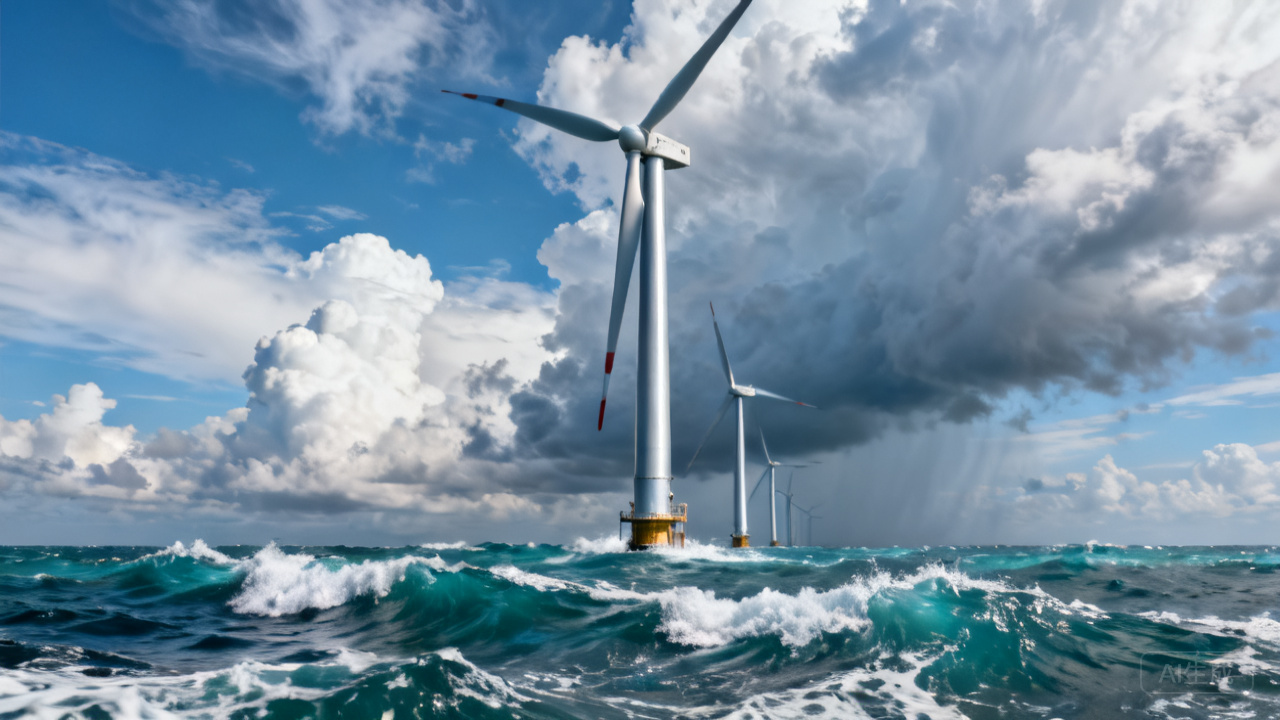
Onshore / offshore wind turbine towers
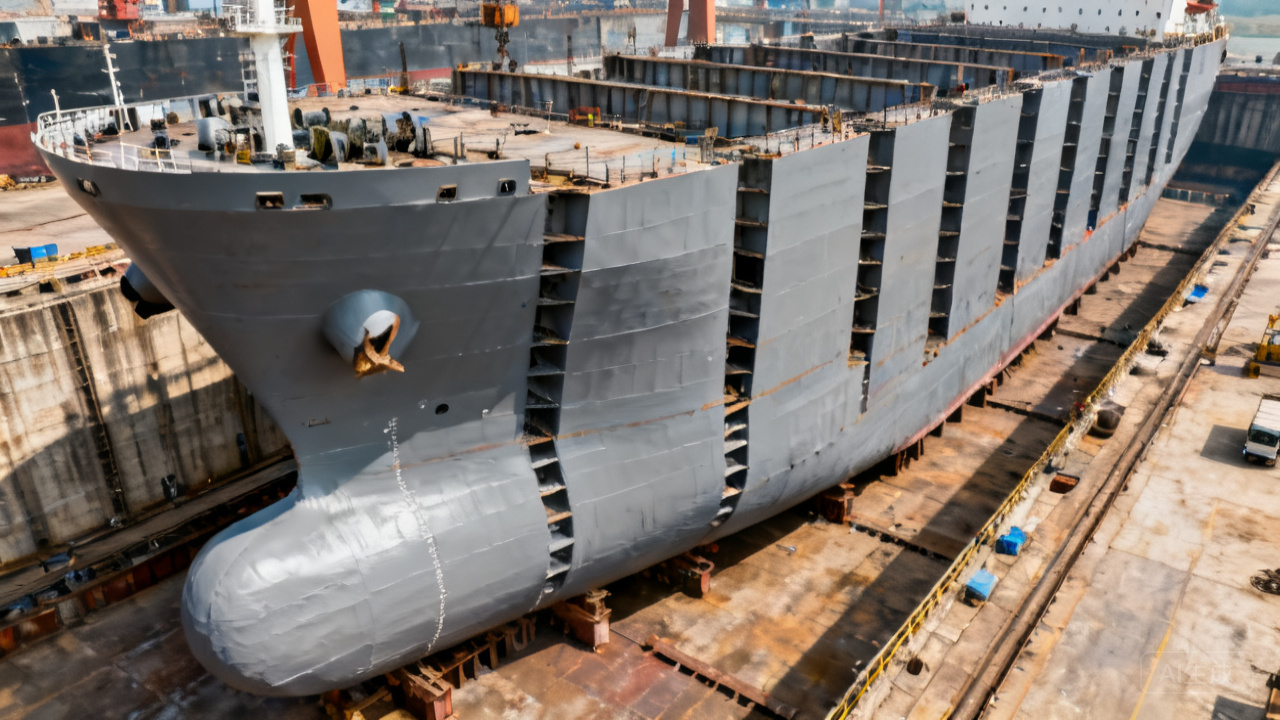
Shipbuilding and offshore engineering
Hull blocks, ballast tanks, decks
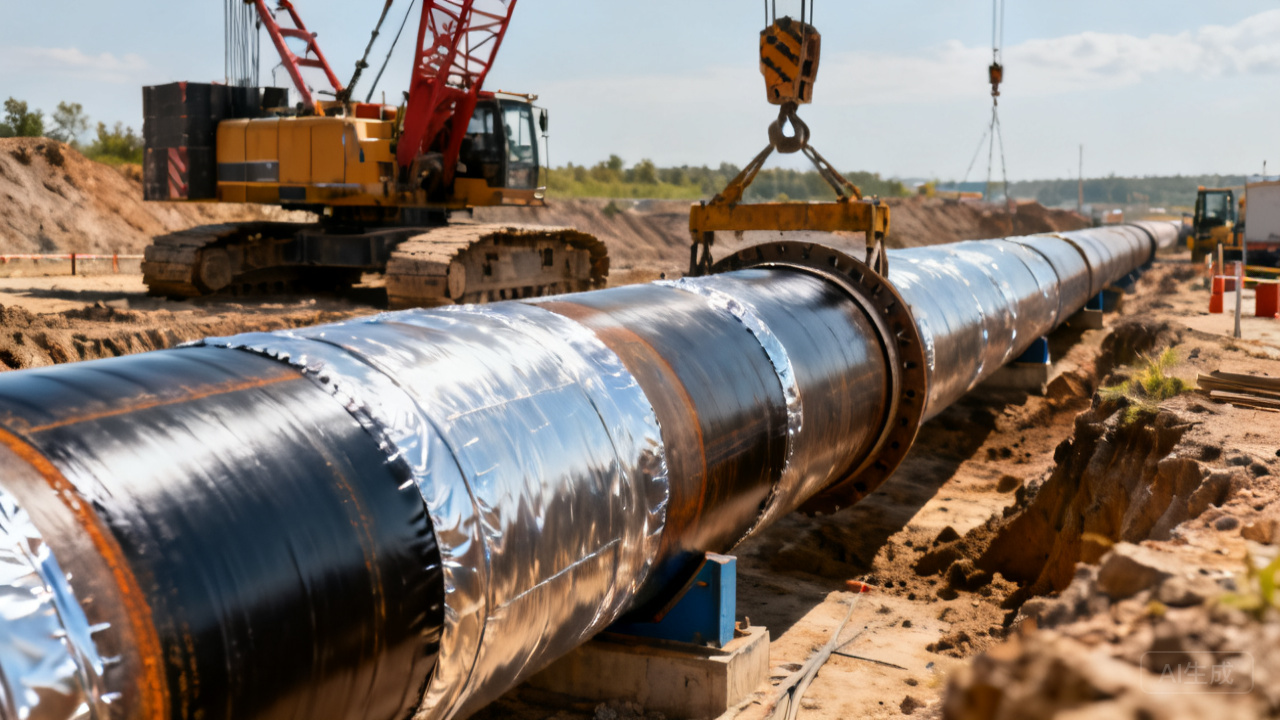
External pipeline anti-corrosion
Long-distance oil, gas and water pipelines
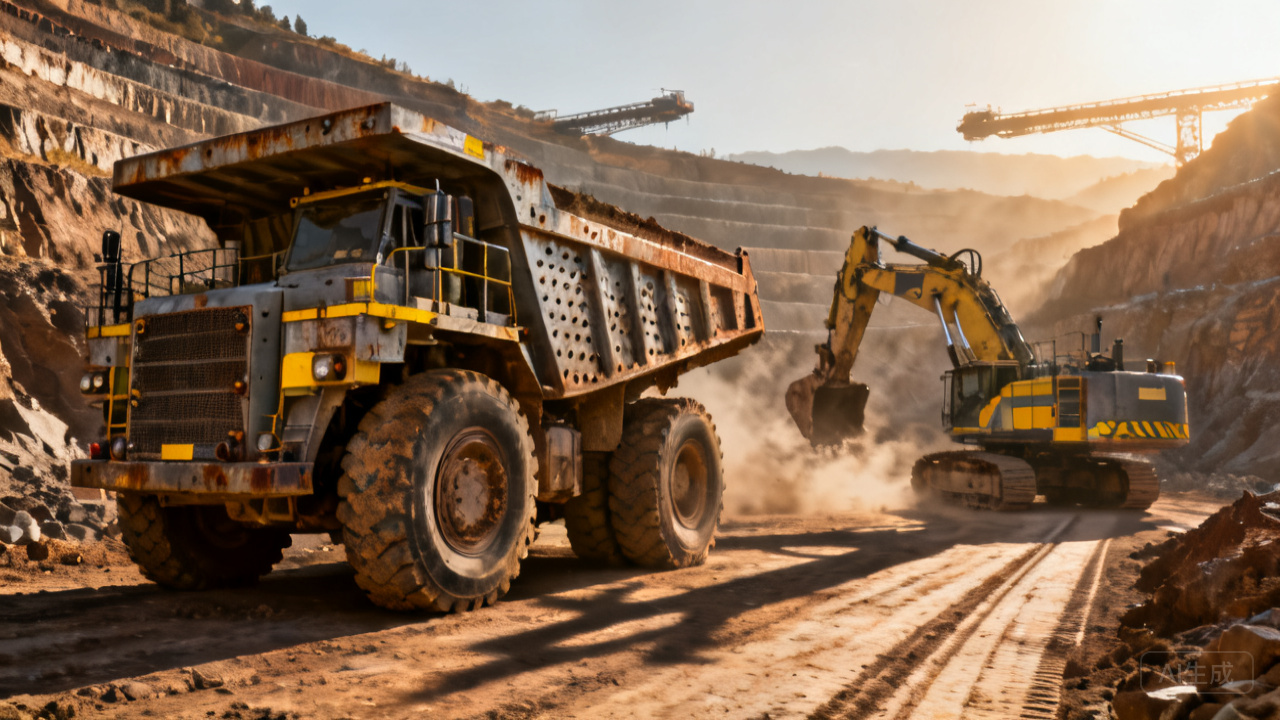
Mining / construction machinery
Excavators, crushers, conveying equipment
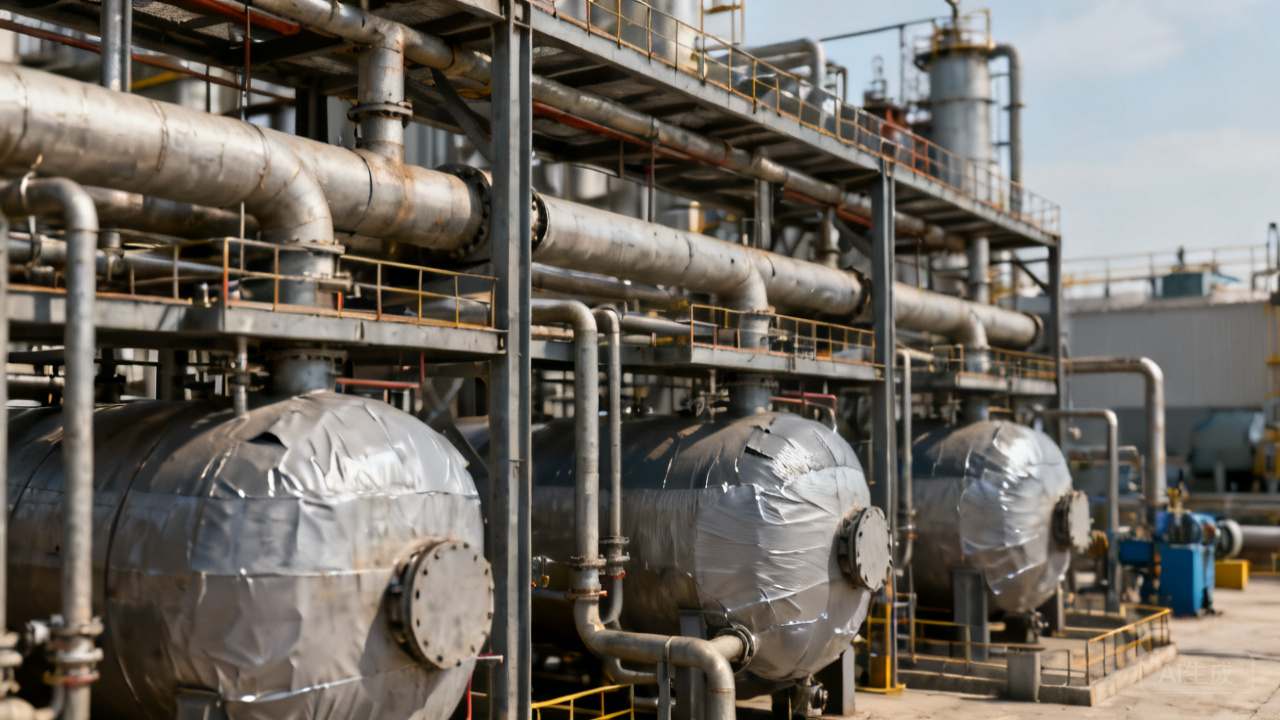
Chemical / refining plants
Reactors, heat exchangers, pipe-rack steelwork
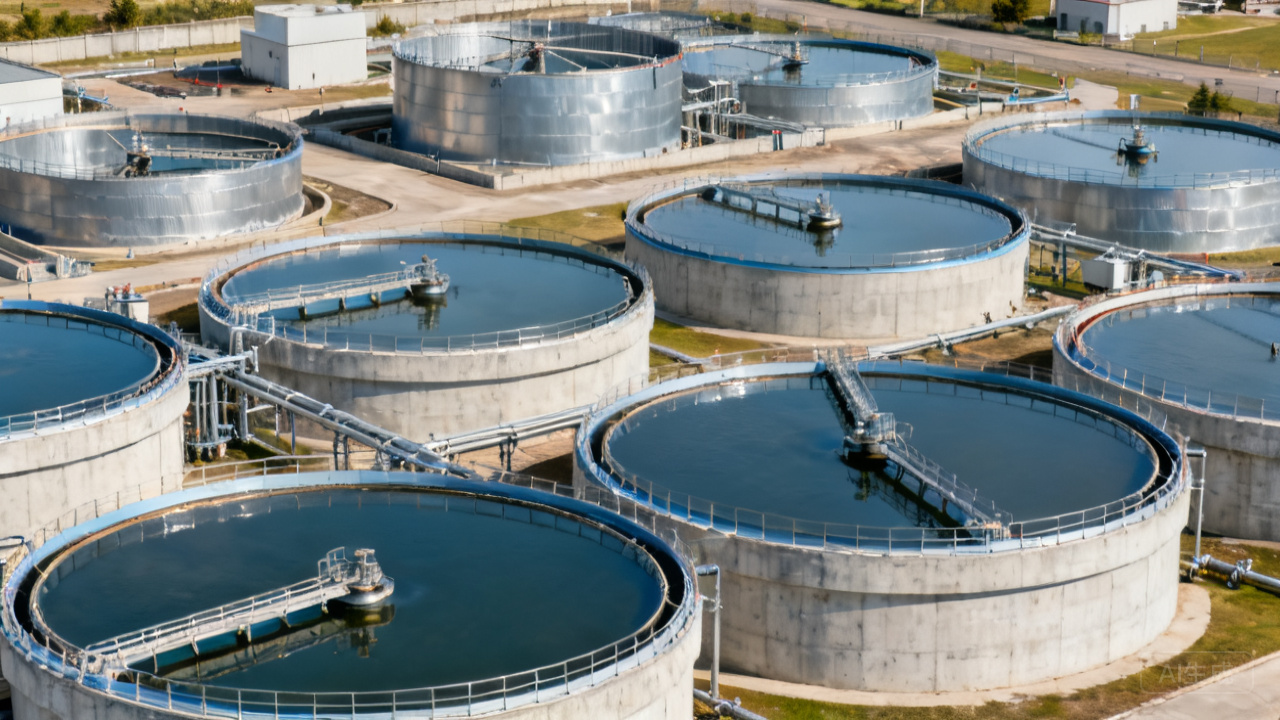
Water treatment / water conservancy facilities
Sewage plants, sluice gates, trash racks
Frequently AskedFAQ
DownloadCenter
TDS Product Technical Specifications
Technical Data Sheet
Compliant with HG/T 3668-2020 standard
MSDS (Material Safety Data Sheet)
Material Safety Data Sheet
16 Chapters · GB/T 16483-2008
Color Card (Product Color Card)
Color Card
Steel-grey / iron-red standard colours
Application guide
Application Guide
Complete construction guidance + defect countermeasures
projectCases
Anticorrosion of the steel box girders of the Akashi Kaikyo Bridge, Japan
Heavy-duty anticorrosion for North Sea offshore oil platform jackets
Anticorrosion for ZPMC container ship-to-shore cranes at Chennai Port, India
Corrosion protection of wind turbine towers at a South China Sea offshore wind farm
Epoxy micaceous iron oxide intermediate paint·Factory direct supply
Free sample testing · Customized technical solutions · On-site construction guidance · ISO 9001 certified factory · 48-hour rapid response
Related articles & news
Further reading: technical articles and industry news from Kexin New Materials